

Design of a Negative Pressure Pneumatic Conveying Device for Sodium Bicarbonate
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. The company's latest innovation is a sophisticated negative pressure pneumatic conveying system tailored for the efficient transport of sodium bicarbonate. This system represents a significant advancement in industrial material transport technology, offering enhanced safety, reliability, and operational efficiency.
Key Features of the Negative Pressure Pneumatic Conveying System
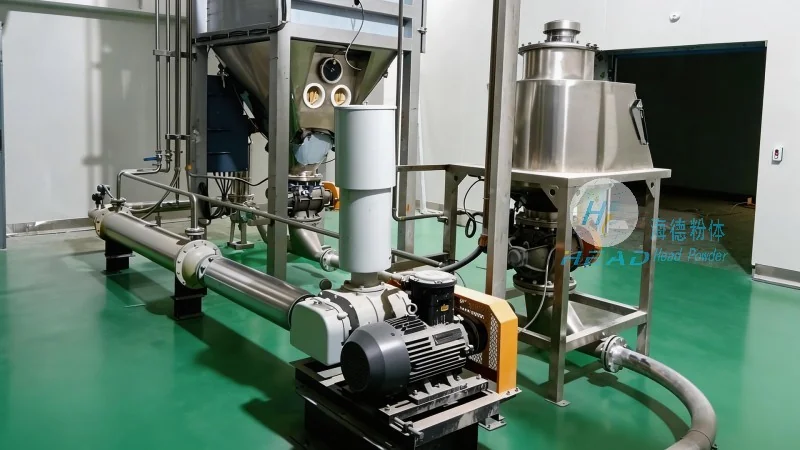
The negative pressure pneumatic conveying device for sodium bicarbonate is engineered with several key features that address the unique challenges of handling this material. The system operates under negative pressure, which prevents dust emissions and ensures a clean, safe working environment. This is particularly important for sodium bicarbonate, a fine powder that can be easily dispersed in the air if not properly contained. The design incorporates high-efficiency filtration systems that capture and recycle any airborne particles, maintaining compliance with environmental regulations and workplace safety standards.
Engineering Excellence and Customization
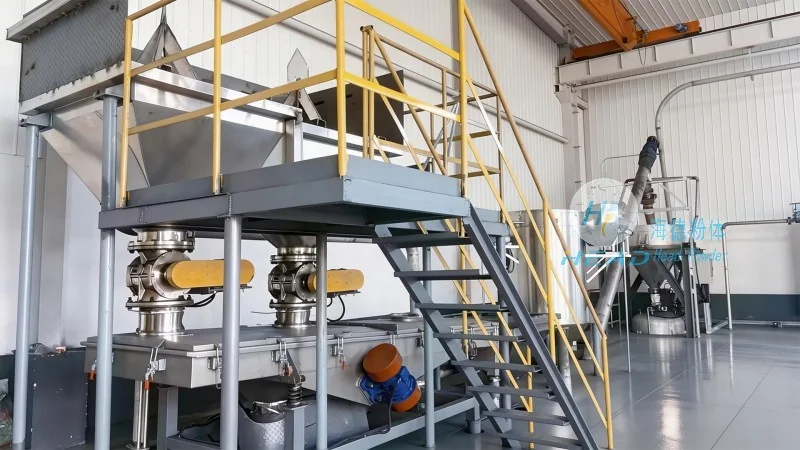
Shandong HeadPowder Engineering Co., Ltd. employs a team of experienced engineers who collaborate closely with clients to develop customized solutions. The negative pressure conveying system is modular and scalable, allowing it to be adapted to various production capacities and facility layouts. The company's expertise in material science and pneumatic transport technology enables the optimization of the system's performance, ensuring minimal energy consumption and maximum throughput. Each component, from the material feeders to the air filtration units, is selected and configured to meet the specific requirements of the sodium bicarbonate application, resulting in a highly efficient and reliable operation.
Operational Benefits and Safety Advantages
Implementing the negative pressure pneumatic conveying system for sodium bicarbonate offers numerous operational benefits. The system reduces labor costs by automating the material transport process, minimizing the need for manual handling of bulk materials. It also enhances production efficiency by ensuring a continuous and uninterrupted flow of sodium bicarbonate, which is critical for maintaining consistent product quality. From a safety perspective, the negative pressure design eliminates the risk of dust explosions, a common hazard in powder handling operations. The enclosed system and integrated filtration further protect workers from respiratory hazards associated with fine powders, creating a safer workplace environment.
Application and Industry Impact
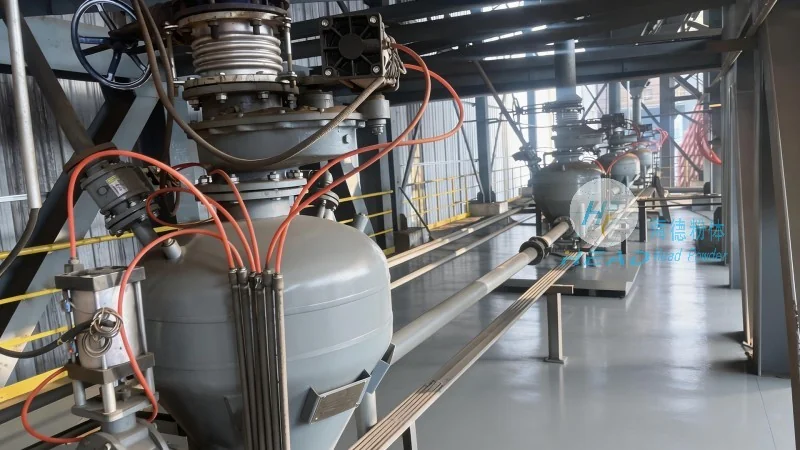
The negative pressure pneumatic conveying device is particularly suitable for industries that rely on sodium bicarbonate as a raw material, such as food processing, pharmaceuticals, and chemical manufacturing. The system's ability to handle fine powders with precision and control makes it an ideal choice for applications where product purity and consistency are paramount. By reducing material loss and improving process control, the system contributes to cost savings and increased profitability for businesses. The technology also aligns with modern industrial standards, supporting sustainable and environmentally responsible operations.