

Long - distance Pneumatic Conveying System for Sodium Bicarbonate
Efficient and reliable material handling is a critical factor in the production and distribution of sodium bicarbonate. The long - distance pneumatic conveying system designed by Shandong HeadPowder Engineering Co., Ltd. offers a cutting - edge solution that addresses the unique challenges associated with transporting this chemical compound over extended distances. This system combines advanced engineering principles with robust construction to ensure safe, efficient, and cost - effective operation in industrial settings.
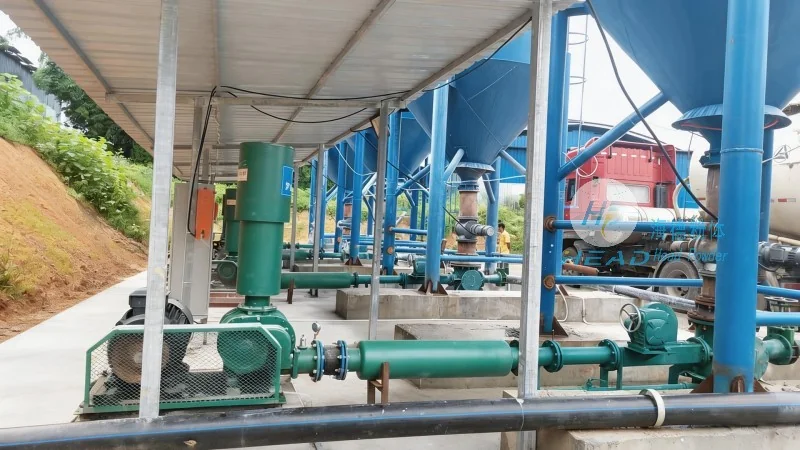
System Overview and Core Components
The pneumatic conveying system for sodium bicarbonate is engineered to handle the specific properties of this material, including its particle size, flow characteristics, and potential dust generation. At the heart of the system are several key components that work in unison to achieve seamless material transport. The feed hopper is designed to store and meter the sodium bicarbonate, ensuring a consistent flow into the conveying line. The air compressor and associated piping system generate the necessary air pressure to move the material through the pipeline. The conveying pipeline itself is constructed from high - quality materials that are resistant to corrosion and wear, which is essential for long - term operation with sodium bicarbonate. Additionally, the system incorporates a dust collection and filtration unit to maintain air quality and comply with environmental regulations. These components are carefully selected and integrated to provide a durable and efficient solution for long - distance material transport.
Advantages of the Pneumatic Conveying System
Compared to traditional conveying methods such as belt conveyors or bucket elevators, the pneumatic conveying system offers several distinct advantages. One of the primary benefits is the ability to transport sodium bicarbonate over long distances without the need for multiple transfer points or intermediate storage. This reduces the overall footprint of the production facility and minimizes the risk of material spillage or contamination. The system also provides a closed - loop operation, which helps to contain dust and prevent environmental pollution. This is particularly important for sodium bicarbonate, as it is a fine powder that can easily become airborne. Furthermore, the pneumatic system allows for precise control over the flow rate and pressure, enabling operators to adjust the conveying speed according to production requirements. This flexibility is crucial in dynamic industrial environments where production rates may vary. The system's energy efficiency is another significant advantage. By using compressed air as the primary motive force, the system consumes less energy compared to mechanical conveying systems that rely on motors and pulleys. This results in lower operational costs and a reduced carbon footprint, aligning with modern sustainability goals.
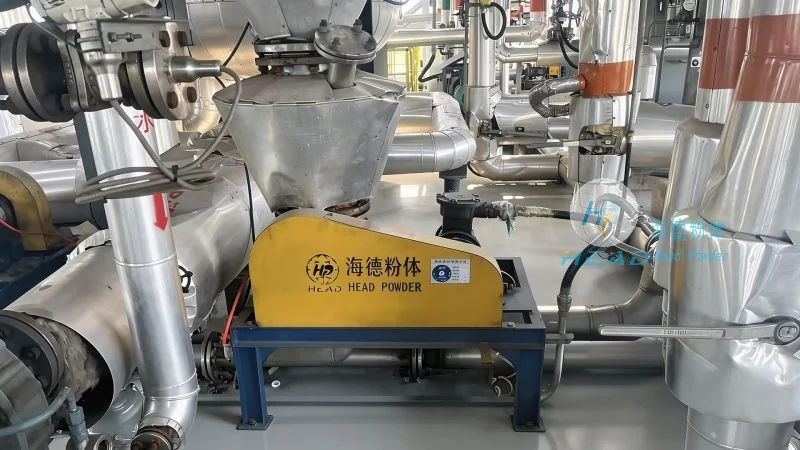
Application Scenarios and Industry Impact
The long - distance pneumatic conveying system is widely used in various industries that rely on sodium bicarbonate as a raw material. In the food and beverage industry, for example, the system is used to transport sodium bicarbonate to production lines for baking powder or other food additives. The system's ability to maintain product purity and prevent contamination is critical in this sector, as any impurities can affect the quality of the final product. In the pharmaceutical industry, the system is employed to move sodium bicarbonate to manufacturing facilities, where it is used as an excipient or active ingredient in various medications. The system's sterile and dust - free operation ensures that the material remains in a state suitable for pharmaceutical use. The chemical industry also benefits from this system, as it is used to transport sodium bicarbonate to plants that produce other chemical compounds. The system's robust construction and corrosion - resistant materials make it suitable for handling the harsh conditions often encountered in chemical processing. Overall, the system has a positive impact on the efficiency and safety of industrial operations, enabling companies to meet production targets while adhering to environmental and safety standards.
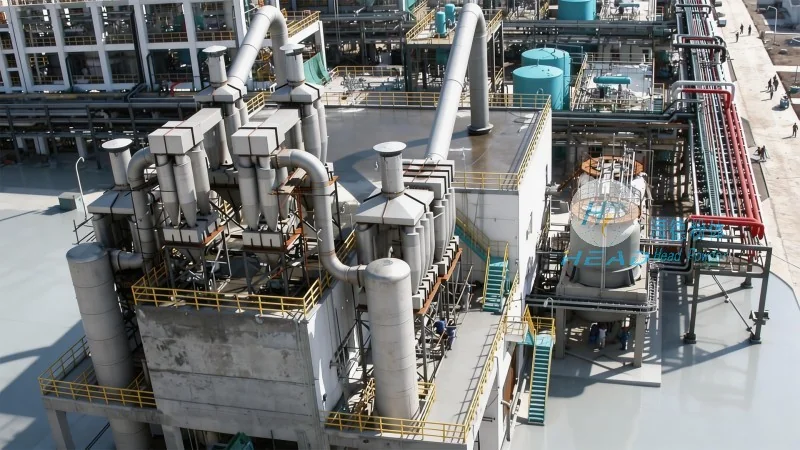
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced material handling systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. Headpowder specializes in designing and manufacturing pneumatic conveying systems for a wide range of materials, including chemicals, powders, and granules. The company's team of experienced engineers and technicians work closely with clients to understand their specific needs and develop customized solutions that meet their requirements. Headpowder's commitment to quality is evident in its use of high - quality materials and rigorous testing procedures. All products are manufactured in compliance with international standards and undergo thorough quality checks before delivery. The company also provides comprehensive after - sales support, including installation, training, and maintenance services. This ensures that clients can operate their systems efficiently and reliably for years to come. Headpowder's headquarters is located in Shandong, China, where the company has a state - of - the - art manufacturing facility and a research and development center. The company's presence in the region allows it to leverage local resources and expertise while serving clients globally.
Conclusion and Future Outlook
The long - distance pneumatic conveying system for sodium bicarbonate developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in material handling technology. By combining advanced engineering with robust construction, the system offers a reliable and efficient solution for transporting sodium bicarbonate over extended distances. The system's advantages, including its ability to handle long distances, maintain product purity, and reduce operational costs, make it an attractive option for industries that rely on this chemical compound. As the demand for efficient material handling continues to grow, companies like headpowder are at the forefront of developing innovative solutions that meet the evolving needs of the market. With its commitment to quality and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. is well - positioned to continue leading the industry in the development of advanced material handling systems.