

Long-Distance Pneumatic Conveying System for Capsules
Long-distance pneumatic conveying systems for capsules represent a sophisticated solution in material handling, particularly for industries dealing with pharmaceuticals, food, and chemical products. These systems utilize air pressure to transport capsules efficiently over extended distances, ensuring minimal product damage and maintaining hygiene standards. The technology has evolved significantly, offering enhanced control, reliability, and adaptability to meet diverse operational requirements.
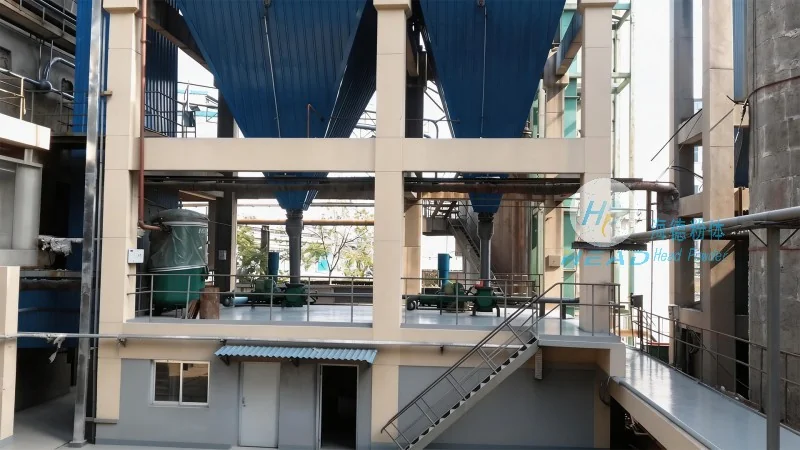
About Shandong HeadPowder Engineering Co., Ltd.
Headpowder, the professional manufacturer behind this advanced pneumatic conveying system, is a leading company based in Shandong, China. With years of expertise in engineering and manufacturing, Headpowder specializes in developing customized material handling solutions tailored to the unique needs of various industries. The company’s commitment to quality, innovation, and customer satisfaction has established it as a trusted partner in the field of pneumatic conveying technology.
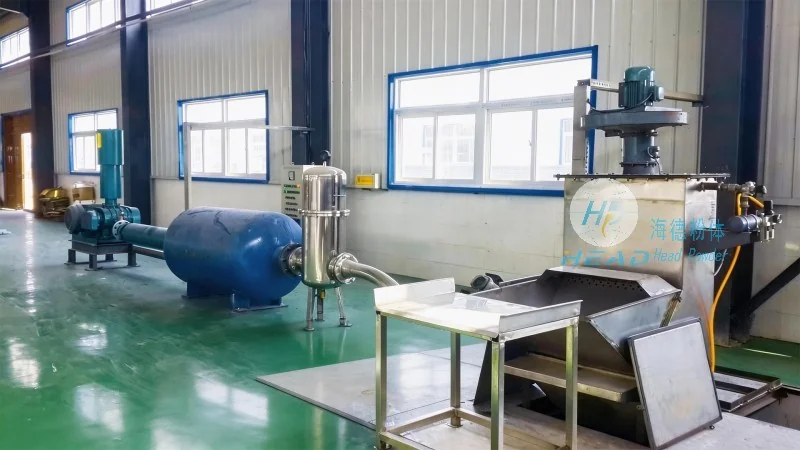
Key Features of the Long-Distance Pneumatic Conveying System
The long-distance pneumatic conveying system for capsules by Headpowder is designed with several key features that enhance performance and reliability. Firstly, the system employs high-efficiency air compressors and precise control valves to maintain consistent air pressure and flow rates, ensuring smooth and continuous capsule transport. The use of specialized conveying pipes and components minimizes friction and product abrasion, preserving the integrity of the capsules during transit. Additionally, the system incorporates advanced monitoring and control systems, allowing operators to track conveying parameters in real-time and adjust settings as needed to optimize efficiency and reduce downtime.
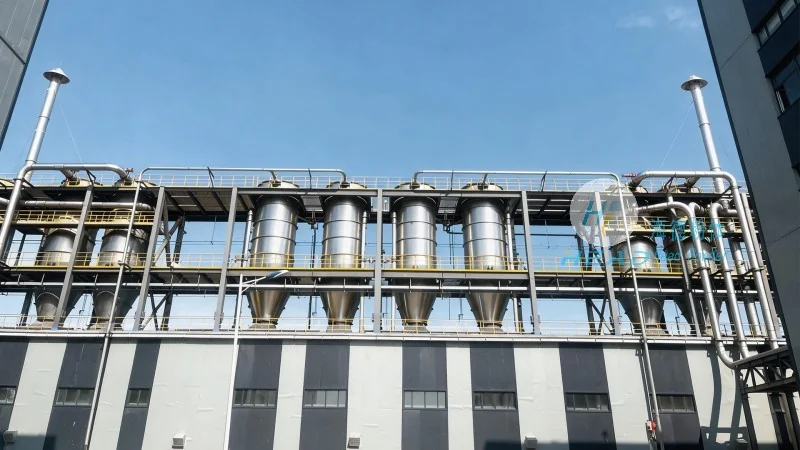
Applications and Benefits
This pneumatic conveying system is widely applicable in pharmaceutical manufacturing, where capsules are transported from production lines to packaging units or storage facilities. The system’s ability to handle delicate capsules without damage is crucial in maintaining product quality and regulatory compliance. In the food industry, it facilitates the transfer of capsules used in dietary supplements or nutraceuticals, ensuring hygienic and efficient processing. The benefits of this system extend beyond efficiency; it also reduces labor costs by automating the conveying process and minimizes the risk of contamination, which is critical in industries where product safety is paramount.
Customization and Integration
Headpowder understands that each client’s operational environment is unique. Therefore, the long-distance pneumatic conveying system is highly customizable to fit specific space constraints, production volumes, and material characteristics. The company offers tailored solutions that integrate seamlessly with existing production lines, minimizing disruption during installation and operation. Whether it’s a small-scale setup or a large industrial facility, Headpowder’s engineering team works closely with clients to design a system that meets all technical and operational requirements.
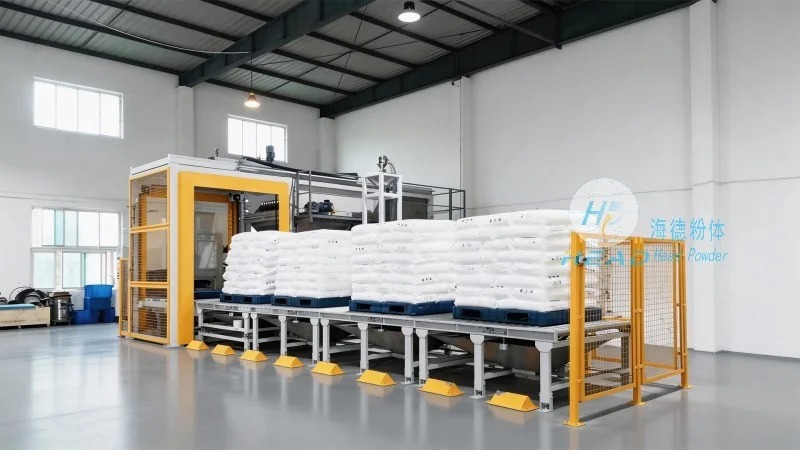
Quality Assurance and After-Sales Support
Headpowder places a strong emphasis on quality assurance throughout the manufacturing process. All components of the pneumatic conveying system are manufactured using high-grade materials and undergo rigorous testing to ensure durability and performance. The company provides comprehensive after-sales support, including maintenance services, spare parts availability, and technical assistance to ensure the system operates at peak efficiency throughout its service life. This commitment to quality and support has earned Headpowder a reputation for reliability and customer satisfaction in the industry.