

Principle and Classification Application of White Sugar Pneumatic Conveying
White sugar, a staple in global food and beverage industries, requires efficient and reliable transportation methods to maintain quality and operational efficiency. Pneumatic conveying has emerged as a preferred solution for handling white sugar, offering advantages such as dust-free operation, reduced product contamination, and enhanced safety. This article provides an overview of the working principles and classification applications of white sugar pneumatic conveying systems, highlighting the technical aspects and practical implementations used by industry leaders like Shandong HeadPowder Engineering Co., Ltd.
Working Principle of Pneumatic Conveying for White Sugar
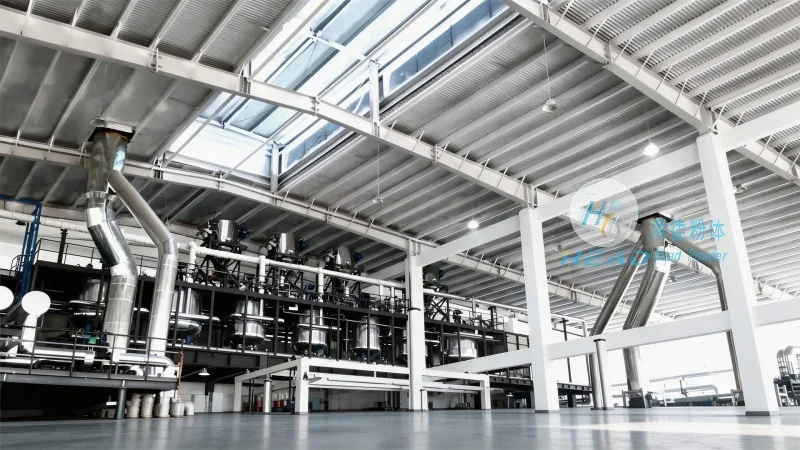
The core principle of pneumatic conveying involves the use of air to transport bulk materials like white sugar through a pipeline system. There are two primary types of pneumatic conveying: dilute-phase and dense-phase. Dilute-phase systems use high-velocity air to suspend the sugar particles, moving them through the pipeline with minimal pressure drop. This method is suitable for short to medium distances and low to medium material loads. Dense-phase systems, on the other hand, operate at lower air velocities, creating a slurry-like flow where sugar particles are more closely packed, reducing particle degradation and ensuring better control over flow rates. For white sugar, which is hygroscopic and sensitive to moisture, dense-phase conveying is often preferred to minimize exposure to air and potential moisture absorption.
Classification of Pneumatic Conveying Systems for White Sugar
Pneumatic conveying systems for white sugar can be classified based on several factors, including the conveying method, pressure level, and application requirements. The most common classifications include:
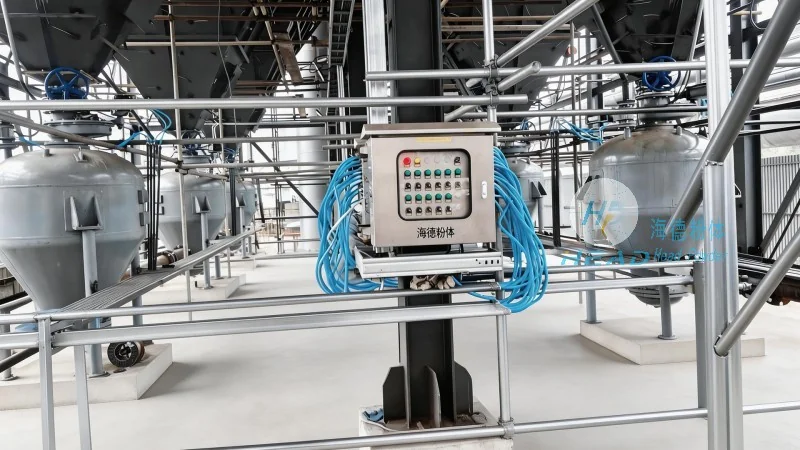
- Positive Pressure Systems: These systems use a blower or fan to generate positive pressure, pushing the air and sugar mixture through the pipeline. They are suitable for long-distance conveying and are commonly used in sugar processing plants to transport raw sugar from storage to processing units.
- Negative Pressure (Vacuum) Systems: In these systems, a vacuum is created at the receiving end to draw the sugar into the pipeline. This method is ideal for short-distance conveying and is often used for transferring sugar from processing equipment to packaging lines. Negative pressure systems are also beneficial for handling fine powders, as they reduce the risk of dust dispersion.
- Hybrid Systems: Combining elements of both positive and negative pressure, hybrid systems offer flexibility in conveying different types of sugar products. For instance, a hybrid system might use positive pressure to transport bulk sugar from a silo to a processing area and then switch to negative pressure for fine sugar transfer to packaging equipment.
Application Scenarios in Sugar Processing
The application of pneumatic conveying in white sugar processing varies based on the stage of production. Here are key scenarios where these systems are utilized:
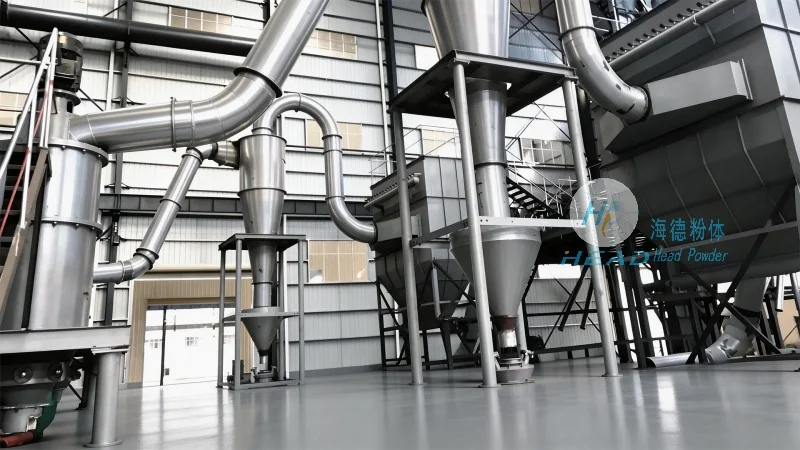
- Raw Sugar Handling: At the initial stage of sugar processing, raw sugar is often stored in large silos. Pneumatic conveying systems efficiently transport raw sugar from storage silos to the refining process, ensuring a continuous supply without manual handling. This reduces labor costs and minimizes the risk of product contamination.
- Refined Sugar Processing: After refining, white sugar is often in a fine powder form. Dense-phase pneumatic conveying is used to move refined sugar from the refining unit to packaging or storage areas. The low velocity and controlled flow prevent the sugar from clumping or losing its fine texture, maintaining product quality.
- Packaging and Distribution: In the final stages, white sugar is transferred to packaging machines for bagging or bulk containers. Pneumatic conveying systems can be integrated with packaging lines to ensure a steady and clean supply of sugar, reducing downtime and improving overall production efficiency.
Advantages of Pneumatic Conveying for White Sugar
Implementing pneumatic conveying systems for white sugar offers several advantages that contribute to operational excellence in sugar processing facilities:
- Dust-Free Operation: Unlike traditional belt or bucket elevators, pneumatic conveying systems operate in closed pipelines, preventing dust dispersion and maintaining a clean working environment. This is crucial for white sugar, which is sensitive to contamination and requires stringent hygiene standards.
- Reduced Product Contamination: The enclosed system minimizes contact with external elements, including moisture and airborne particles. This helps preserve the purity and quality of white sugar, which is essential for meeting food safety regulations and consumer expectations.
- Enhanced Safety: Pneumatic conveying eliminates the need for manual handling of bulk sugar, reducing the risk of workplace accidents such as slips, trips, or falls. The system also reduces exposure to dust, which can cause respiratory issues, making it a safer option for workers.
- Energy Efficiency: Modern pneumatic conveying systems are designed to optimize energy usage. By using appropriate air velocities and pressure levels, these systems can achieve efficient material transport while minimizing energy consumption, leading to cost savings over time.
- Flexibility and Scalability: Pneumatic conveying systems can be easily adjusted to handle varying volumes of white sugar, making them suitable for both small-scale and large-scale sugar processing operations. They can also be integrated with existing infrastructure, allowing for seamless upgrades or expansions.
Conclusion and Company Overview
Pneumatic conveying has become an indispensable technology in the white sugar industry, providing efficient, safe, and hygienic solutions for material handling. Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying systems, specializes in designing and manufacturing customized solutions tailored to the unique needs of sugar processing facilities. With a focus on innovation and quality, the company ensures that its systems meet the highest standards of performance and reliability, helping sugar manufacturers optimize their operations and maintain product excellence. Based in Shandong, China, HeadPowder Engineering leverages its expertise to deliver cutting-edge pneumatic conveying solutions that enhance productivity and sustainability in the global sugar industry.