

Working Principle and Features of Organic Fertilizer Granule Material Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of advanced conveying systems tailored for organic fertilizer granule handling. The organic fertilizer granule material conveying system is a critical piece of equipment in the fertilizer production process, ensuring efficient and reliable transportation of granular organic materials from one stage to another. This article delves into the working principle and key features of such systems, highlighting their importance in modern agricultural and fertilizer manufacturing operations.
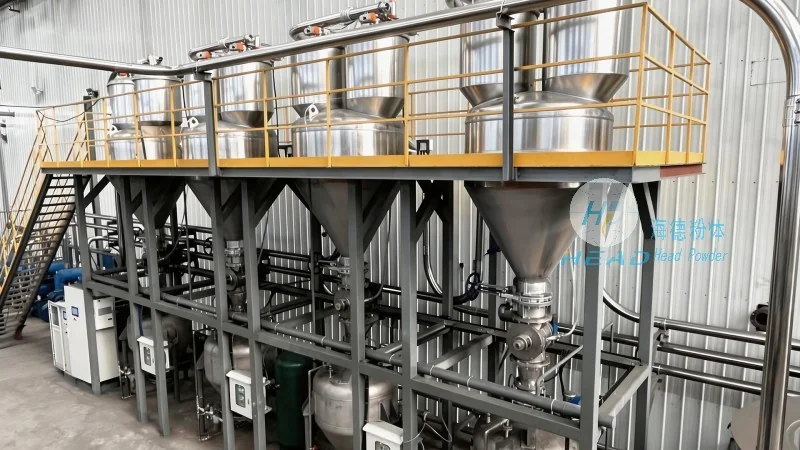
Working Principle of the Organic Fertilizer Granule Material Conveying System
The organic fertilizer granule material conveying system operates on the principle of mechanical transport, utilizing various components to move granular organic fertilizer efficiently. At its core, the system typically includes a feeding mechanism, a conveying unit (such as a screw conveyor, belt conveyor, or pneumatic conveyor), and a control system. The feeding mechanism ensures that the granules are uniformly fed into the conveying unit, while the conveying unit transports them to the desired location. The control system monitors and regulates the flow rate and speed, maintaining consistent performance. For example, a screw conveyor, a common type in such systems, uses a rotating screw to push the granules forward through a cylindrical tube. This mechanism is particularly effective for handling dry, free-flowing granules, as it minimizes material degradation and ensures smooth transport. The system may also incorporate features like variable speed drives and material sensors to adapt to different production demands and maintain optimal operation.
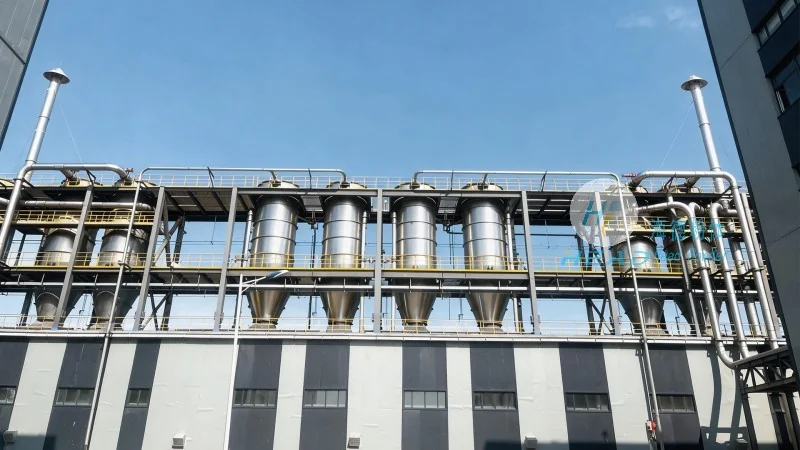
Key Features of the Organic Fertilizer Granule Material Conveying System
Several key features distinguish the organic fertilizer granule material conveying system from other conveying solutions, making it ideal for fertilizer production. First, the system is designed for high efficiency and reliability, with components engineered to handle the specific characteristics of organic fertilizer granules. These granules often have varying sizes, moisture content, and bulk density, which can affect conveying performance. The system’s design addresses these challenges by using durable materials and robust construction, ensuring long service life and minimal downtime. Second, the system offers flexibility in conveying routes, allowing for horizontal, vertical, or inclined transport as required by the production layout. This adaptability is crucial in large-scale fertilizer plants where multiple processing stages are involved. Third, the system incorporates advanced control and monitoring capabilities, enabling real-time tracking of material flow and system performance. This allows operators to adjust parameters dynamically, optimizing energy consumption and production output. Additionally, the system is equipped with safety features, such as overload protection and emergency stop mechanisms, to prevent accidents and ensure safe operation. These features collectively contribute to the system’s high performance and user-friendly operation.
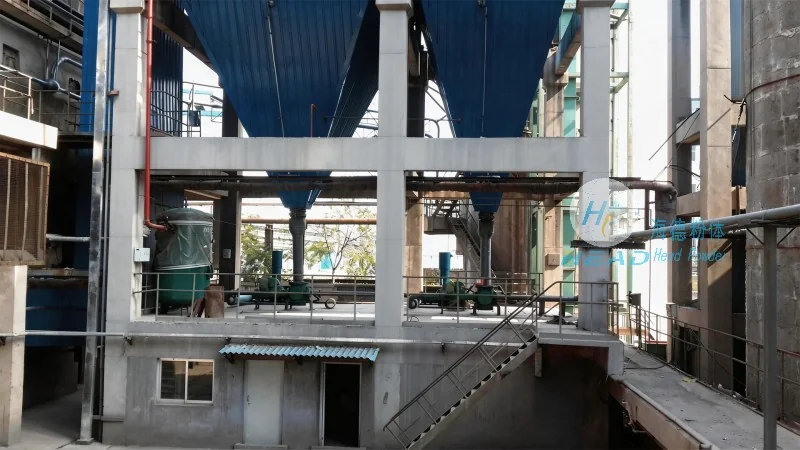
Application and Benefits in Fertilizer Manufacturing
The organic fertilizer granule material conveying system plays a vital role in the overall fertilizer manufacturing process, contributing to increased productivity and operational efficiency. By efficiently transporting granules between different stages—such as from the granulation unit to the packaging line or from storage to the blending area—the system reduces manual handling and labor costs. This automation also minimizes the risk of material spillage and contamination, maintaining product quality. Furthermore, the system’s ability to handle varying material characteristics ensures consistent performance, even with fluctuations in raw material quality. This consistency is essential for maintaining product specifications and meeting customer demands. The system’s durability and low maintenance requirements also contribute to long-term cost savings, as it reduces the need for frequent repairs and replacements. Overall, the organic fertilizer granule material conveying system is a critical investment for fertilizer manufacturers, enhancing their operational capabilities and supporting sustainable agricultural practices.