

Working Principle and Features of Bin Pump Material Handling Equipment
Bin pump material handling equipment is a specialized system designed for efficient bulk material transport in industrial settings. This equipment plays a crucial role in various industries, including mining, construction, and chemical processing, by providing a reliable and flexible solution for moving large volumes of materials over long distances or to elevated positions.
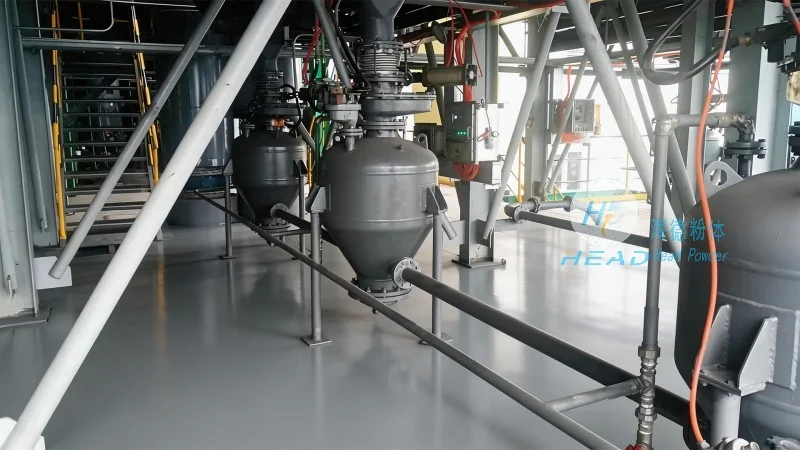
Introduction to Bin Pump Material Handling Equipment
Bin pumps, also known as pressure pumps or pneumatic conveyors, are integral components in material handling systems. They are engineered to handle a wide range of bulk materials, such as powders, granules, and fine particles, with precision and minimal degradation. The equipment is typically composed of a hopper, a pump body, a control system, and a discharge mechanism, all working in harmony to ensure smooth material flow.
Working Principle of Bin Pump Material Handling Equipment
The working principle of bin pump material handling equipment revolves around the use of compressed air or gas to create pressure within the pump chamber. When the material is fed into the hopper, it is drawn into the pump by the pressure differential. As the pump cycles, the material is compressed and forced through the discharge line to the desired destination. This process is highly efficient, as it eliminates the need for mechanical components like belts or screws that can cause material degradation or blockages.
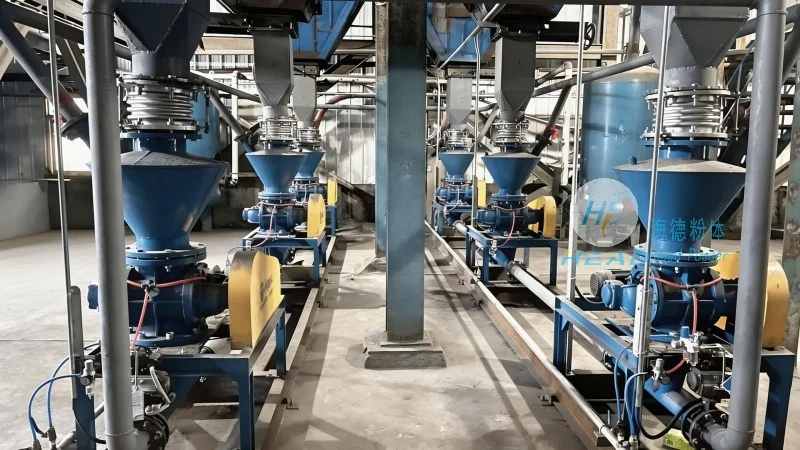
Key Features of Bin Pump Material Handling Equipment
One of the primary features of bin pump material handling equipment is its ability to handle abrasive and corrosive materials without significant wear or damage. The design incorporates durable materials, such as stainless steel or high-grade alloys, to withstand harsh operating conditions. Additionally, the equipment offers high flexibility in terms of layout and installation, allowing it to be integrated into existing production lines or customized for specific application requirements.
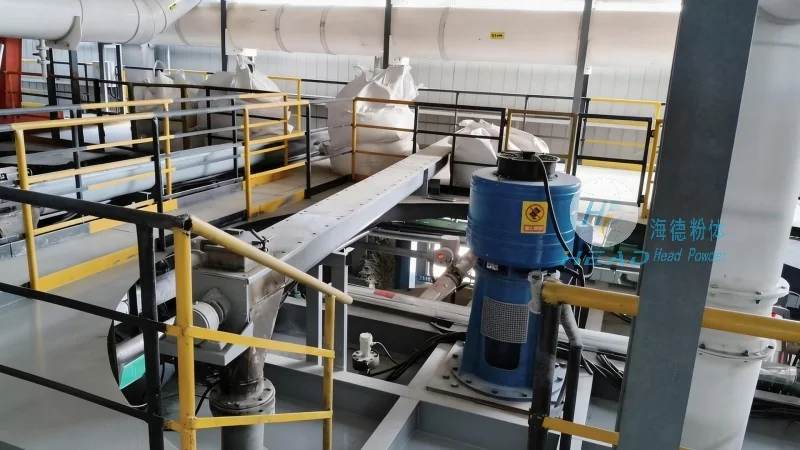
Advantages of Using Bin Pump Material Handling Equipment
Bin pump material handling equipment offers several advantages over traditional conveyor systems. It provides a dust-free and enclosed transport solution, which is essential for maintaining a safe and clean working environment. The system also allows for precise control over material flow rates and pressure, ensuring consistent performance and minimizing material loss. Furthermore, the equipment is energy-efficient, as it uses compressed air rather than electric motors, reducing operational costs and environmental impact.
Applications of Bin Pump Material Handling Equipment
Bin pump material handling equipment is widely used in various industrial applications. In the mining industry, it is employed to transport ore and minerals from storage bins to processing plants. In the construction sector, it is used to move sand, cement, and other building materials to construction sites. The equipment is also prevalent in the chemical and pharmaceutical industries, where it handles powders and granules with high purity requirements. Its versatility makes it suitable for both new installations and retrofitting existing facilities.