

Operation Process and Working Principle of Chicken Essence Material Pneumatic Conveying Line
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of material handling systems, specializes in the design, production, and installation of advanced pneumatic conveying equipment. The company, often referred to as HeadPowder, is headquartered in Shandong, China, and has built a strong reputation for delivering high-quality solutions tailored to the needs of the food processing industry, particularly in the handling of chicken essence materials.
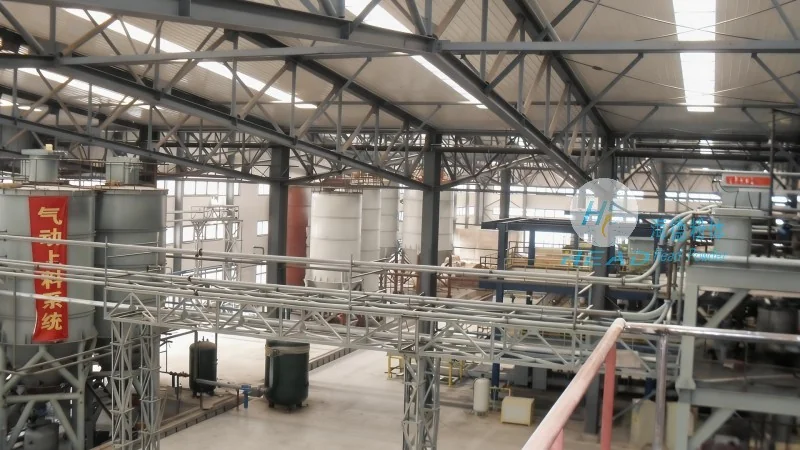
Overview of Chicken Essence Material Pneumatic Conveying Lines
A chicken essence material pneumatic conveying line is a sophisticated system designed to transport chicken essence powders and related ingredients from storage silos or production areas to processing units or packaging stations. This system utilizes compressed air or other gas to move the material through a network of pipes, ensuring efficient, hygienic, and low-maintenance operation. The design of such a line is critical for maintaining the quality and integrity of the chicken essence, which is highly sensitive to moisture, temperature, and contamination.
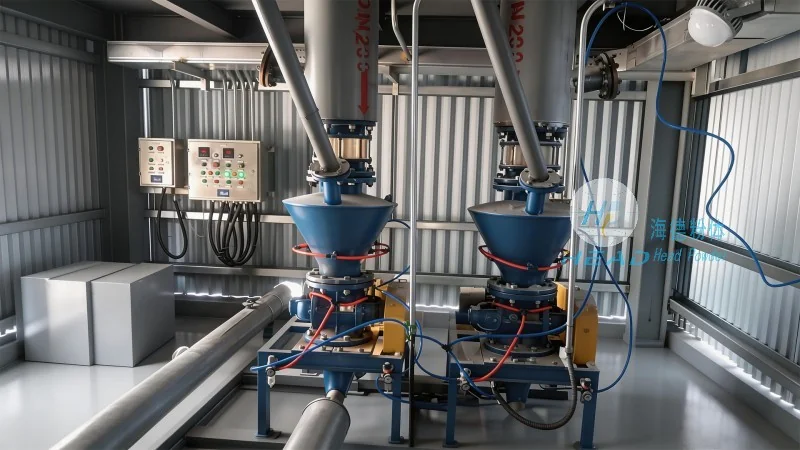
Working Principle of the Pneumatic Conveying System
The core working principle of a chicken essence material pneumatic conveying line involves the use of a positive pressure or negative pressure system to move material through the pipeline. In a positive pressure system, compressed air is introduced into the material, creating a flow that propels the powder forward. Conversely, a negative pressure system draws the material into the pipe using a vacuum. For chicken essence, which is typically a fine powder, a positive pressure system is often preferred as it provides better control over the material's velocity and reduces the risk of clogging. The system includes key components such as a feeder, a compressor, a filter, and a receiver, each playing a vital role in the overall operation.
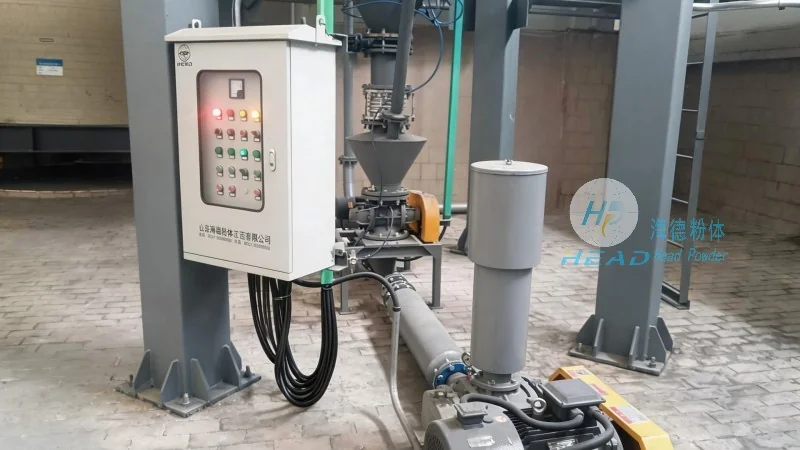
Step-by-Step Operation Process
The operation of a chicken essence material pneumatic conveying line begins with the material being fed into the system from a storage silo. The feeder, which can be a rotary valve or a screw feeder, regulates the flow rate of the chicken essence into the pipeline. Simultaneously, the compressor generates the necessary pressure to move the material. As the compressed air mixes with the powder, it forms a slurry that travels through the pipes to the destination point, such as a mixing or packaging unit. The receiver at the end of the line collects the material and may include a dust collection system to ensure environmental compliance and product purity. The entire process is automated, with sensors and controls monitoring pressure, flow rate, and material levels to maintain optimal performance and prevent system failures.
Key Technical Features and Benefits
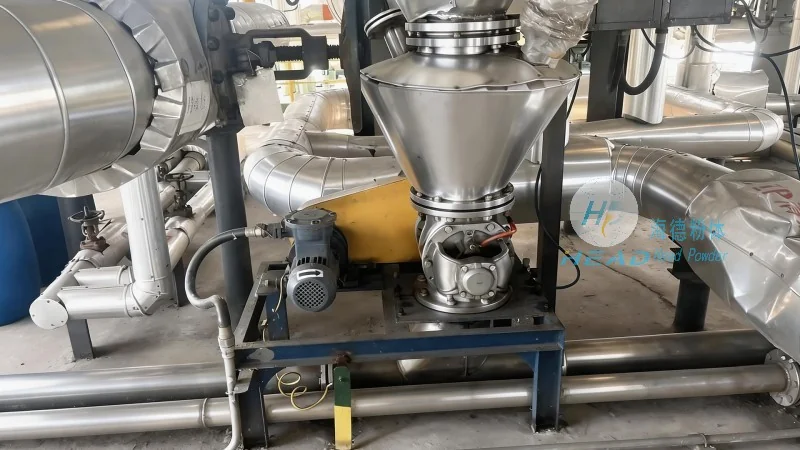
Shandong HeadPowder Engineering Co., Ltd. designs chicken essence material pneumatic conveying lines with several key technical features that enhance efficiency and product quality. These include: (1) Hygienic Design: The system is constructed from stainless steel and other food-grade materials to prevent contamination and meet regulatory standards. (2) Low Maintenance: The use of positive pressure and proper material handling reduces wear and tear on components, minimizing downtime. (3) Energy Efficiency: Advanced compressors and flow control mechanisms optimize energy consumption while maintaining performance. (4) Customization: The company offers tailored solutions to accommodate varying production volumes and material characteristics, ensuring that the system meets the specific needs of each client.
Conclusion
Chicken essence material pneumatic conveying lines, as exemplified by the solutions provided by Shandong HeadPowder Engineering Co., Ltd., represent a reliable and efficient method for handling sensitive food materials. By understanding the working principles and operation process, users can appreciate the technological advancements that enable safe, hygienic, and cost-effective material transport in the food processing industry. The company's commitment to quality and innovation ensures that its customers receive systems that not only meet current industry standards but also support long-term operational success.