

Working Principle and Features of Negative Pressure Vacuum Powder Conveying Lines
Understanding the working principle of negative pressure vacuum powder conveying lines is essential for appreciating their efficiency and reliability in industrial applications. These systems operate by creating a vacuum within the conveying pipeline, which draws the powder material from the source to the destination. The process typically involves a vacuum pump that generates the negative pressure, while the powder is transported through a sealed system to prevent dust emissions and ensure material integrity.
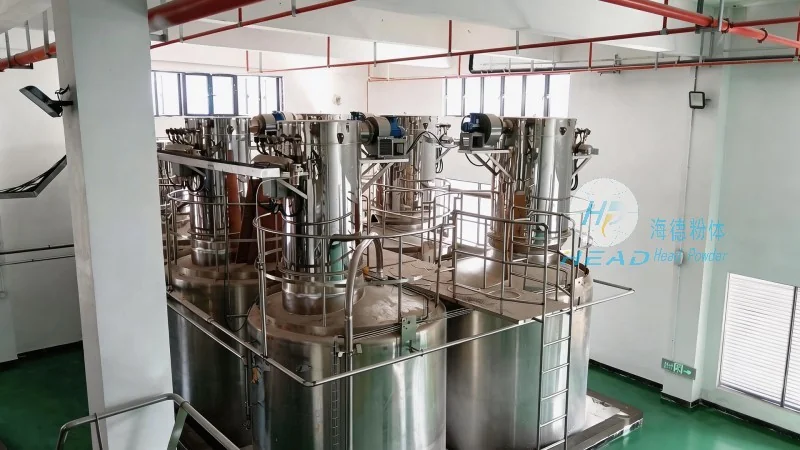
Key Components and Operation Mechanism
The core components of a negative pressure vacuum powder conveying line include a vacuum pump, a filter system, a control panel, and a network of pipes. The vacuum pump is responsible for maintaining the low-pressure environment, while the filter captures any fine particles or dust to protect the pump and ensure clean operation. The control panel allows operators to monitor and adjust the system parameters, such as pressure and flow rate, to optimize performance. The sealed pipes prevent material leakage and environmental contamination, making the system suitable for handling sensitive or hazardous powders.
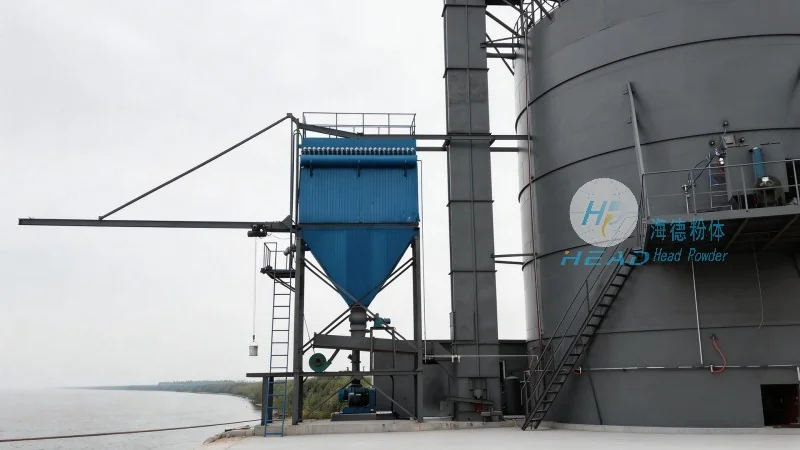
Features and Advantages of Negative Pressure Vacuum Conveying Systems
One of the primary features of negative pressure vacuum powder conveying lines is their ability to handle a wide range of powder types, from fine powders to bulk materials. The system’s flexibility allows for customized configurations to meet specific process requirements. Another key advantage is the high efficiency in material transfer, as the vacuum ensures consistent and continuous flow, reducing downtime and increasing productivity. Additionally, the sealed design enhances safety by minimizing dust exposure and preventing cross-contamination, which is crucial in industries like pharmaceuticals, food processing, and chemical manufacturing.
Application-Specific Benefits and Customization Options
For industries requiring precise control over powder handling, negative pressure vacuum systems offer tailored solutions. For example, in the pharmaceutical sector, the sealed environment and filtration ensure compliance with regulatory standards, while in food processing, the system’s hygienic design prevents contamination. Customization options include adjustable vacuum levels, variable speed pumps, and modular pipe configurations, allowing the system to adapt to different production scales and material characteristics. The durability of the components, such as corrosion-resistant materials for the pipes and pump, further enhances the system’s longevity and cost-effectiveness.
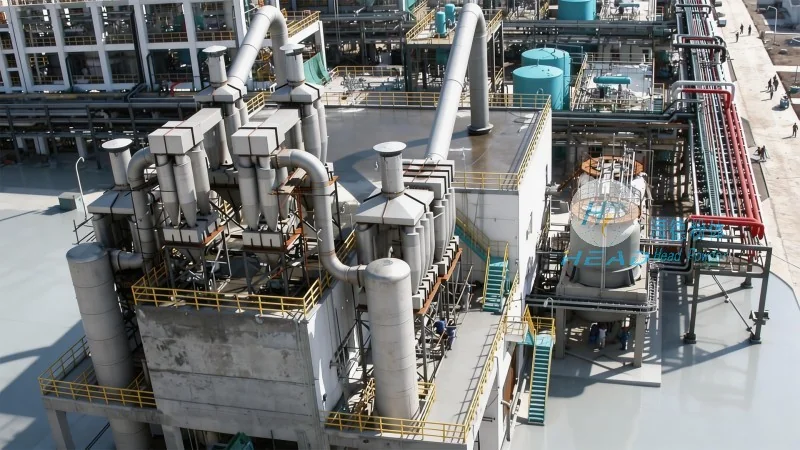
About Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer of powder handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and supplying high-quality negative pressure vacuum powder conveying lines. With years of experience in the industry, the company has developed advanced technologies to meet the diverse needs of its clients. HeadPowder’s commitment to innovation and quality ensures that their systems are reliable, efficient, and compliant with international standards. The company’s headquarters is located in Shandong, China, where they maintain a state-of-the-art production facility and a dedicated R&D team focused on improving powder handling solutions.