

Working Principle and Features of Sodium Bicarbonate Powder Conveying Systems
For industrial applications, the efficient and reliable handling of sodium bicarbonate powder is crucial. This article explores the working principle and key features of a specialized powder conveying system designed for such tasks, highlighting how it addresses common challenges in material transport and storage.
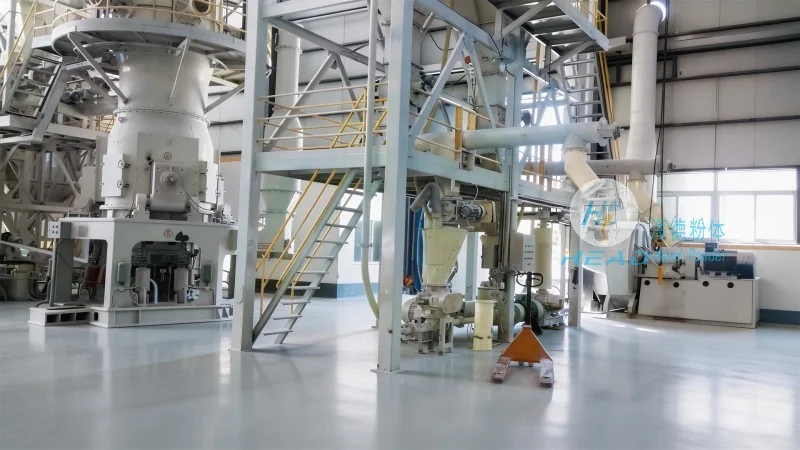
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Headpowder, a leading provider in the field, specializes in engineering solutions for powder handling systems. With a focus on innovation and precision, the company has developed advanced technologies tailored to meet the demands of various industries that rely on sodium bicarbonate. Based in Shandong, China, Headpowder combines years of experience with cutting-edge design to deliver high-performance conveying solutions.
Overview of the Powder Conveying System
The system designed by Headpowder is engineered to handle sodium bicarbonate powder with minimal loss, ensuring consistent flow and preventing material degradation. It integrates multiple components that work in tandem to achieve efficient transport from storage to processing units. The system’s modular design allows for easy integration into existing production lines, making it a versatile solution for different industrial settings.
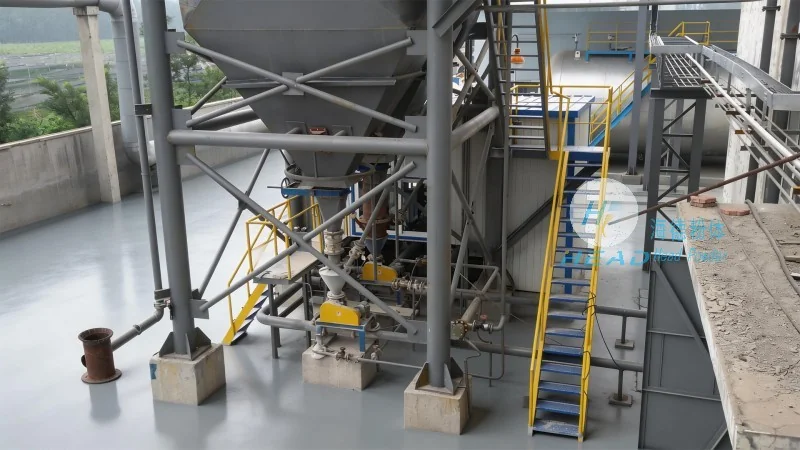
Working Principle of the Conveying System
The core of the system operates on a combination of mechanical and pneumatic principles. It typically begins with a hopper that stores the sodium bicarbonate powder, where a rotary valve or feeder controls the initial discharge. The powder then moves through a pipeline system, often utilizing a positive displacement pump or a pneumatic conveying line. The system uses air pressure to propel the powder, ensuring a smooth and continuous flow. Key components include a dust collector to maintain air quality and a filter system to prevent contamination, which is essential for maintaining the purity of the sodium bicarbonate.
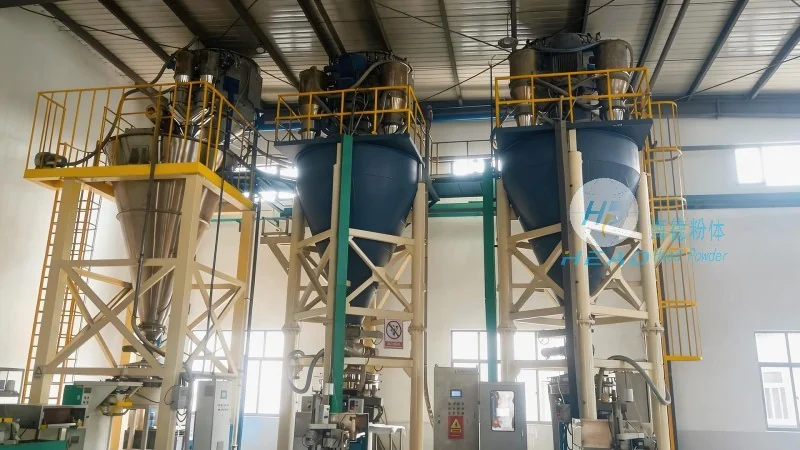
Key Features and Advantages
One of the primary features of this system is its ability to handle fine powders without clogging or blockages. The design incorporates anti-static measures to prevent powder buildup, which enhances safety and operational efficiency. The system also offers adjustable flow rates, allowing users to control the speed of material transport according to specific production requirements. Additionally, the modular construction enables easy maintenance and component replacement, reducing downtime and operational costs. Another notable feature is the system’s energy efficiency, as it minimizes power consumption while maximizing conveying capacity. This makes it an environmentally friendly option for industries seeking sustainable solutions.
Application and Industry Impact
The sodium bicarbonate powder conveying system is widely used in sectors such as food processing, pharmaceuticals, and chemical manufacturing. In food processing, it ensures that the powder is delivered to production lines without contamination, maintaining product quality. In pharmaceutical applications, the system’s precision and cleanliness are critical for meeting regulatory standards. For chemical manufacturers, the system’s ability to handle varying particle sizes and flow rates supports efficient production processes. Overall, the system enhances productivity by streamlining material handling and reducing the risk of material loss or degradation.