

Working Principle and Features of Sugar Pneumatic Conveying Equipment
Understanding the working principle and features of sugar pneumatic conveying equipment is crucial for optimizing material handling processes in the sugar industry. This equipment plays a vital role in efficiently transporting granular sugar from one location to another, ensuring smooth operations and maintaining product quality. The following sections will delve into the technical aspects and key characteristics of such systems, providing insights for industry professionals.
Working Principle of Sugar Pneumatic Conveying Equipment
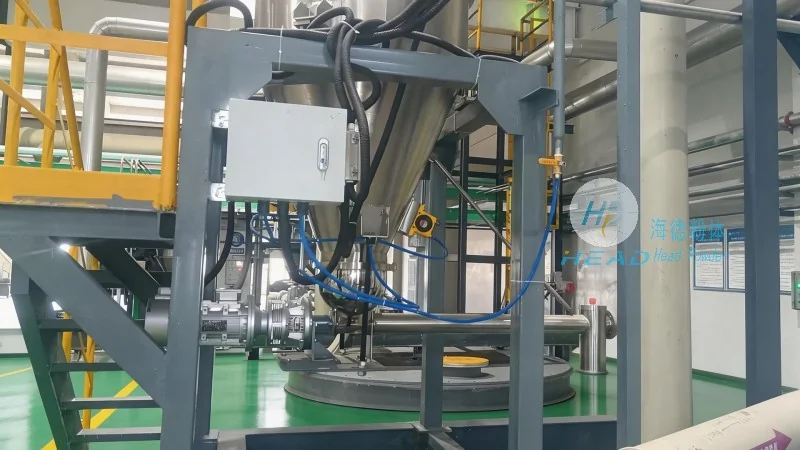
Sugar pneumatic conveying equipment operates based on the principle of using air or gas to transport solid materials like granulated sugar. The system typically consists of a hopper, a conveying line, a fan or blower, and a discharge point. The process begins when sugar is fed into the hopper, where it is then drawn into the conveying line by the airflow generated by the fan. The air-sugar mixture travels through the pipeline under pressure, reaching the discharge point where the sugar is separated from the air and collected. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and minimizing product contamination. The fan or blower provides the necessary pressure and airflow to move the sugar efficiently, with the system's design tailored to handle the specific properties of granulated sugar, such as its density and flowability.
Key Features of Sugar Pneumatic Conveying Equipment
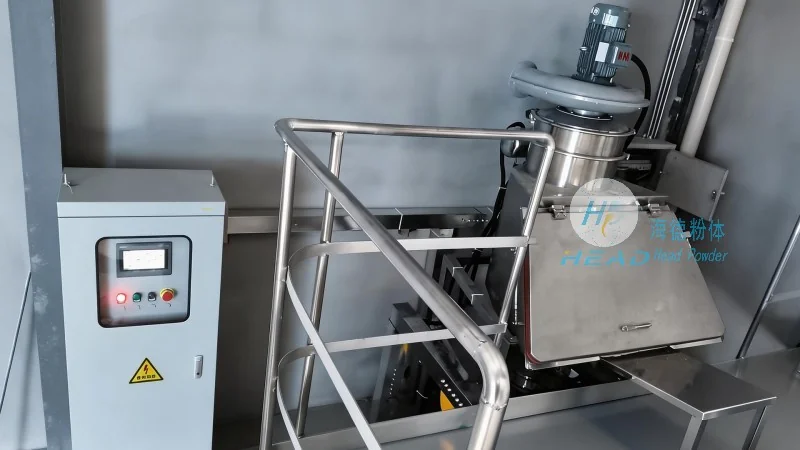
Several notable features distinguish sugar pneumatic conveying equipment from other material handling systems. Firstly, it offers a high degree of flexibility in terms of layout and installation, as the conveying lines can be easily adjusted or reconfigured to accommodate changes in production needs. This adaptability is particularly valuable in sugar processing facilities where space is limited or where production lines are frequently modified. Secondly, the equipment ensures minimal product degradation and contamination, as the sugar remains in a closed system throughout the conveying process. This is achieved through the use of sealed pipelines and proper air filtration, which prevents exposure to external elements or contaminants. Thirdly, the system provides excellent control over the conveying rate, allowing operators to adjust the flow of sugar based on demand or processing requirements. This control is essential for maintaining consistent product quality and preventing overloading or underloading of downstream equipment. Additionally, the equipment is designed for easy cleaning and maintenance, with components that can be easily disassembled and cleaned to prevent the buildup of sugar residue, which can affect the system's performance over time.
Advantages and Applications in Sugar Processing
The implementation of sugar pneumatic conveying equipment brings numerous advantages to sugar processing plants. One of the primary benefits is the significant reduction in labor costs and operational time, as the automated system minimizes the need for manual handling of sugar. This not only improves efficiency but also enhances workplace safety by reducing the risk of accidents associated with manual lifting and moving of heavy sugar bags or containers. Another advantage is the improved product quality, as the closed system prevents moisture absorption or contamination from external sources, which can affect the sugar's taste and shelf life. Furthermore, the equipment's ability to handle large volumes of sugar at a time makes it ideal for high-throughput sugar processing facilities, where rapid and consistent material transport is critical. In applications such as sugar refining, beet sugar processing, or raw sugar handling, the pneumatic conveying system ensures that sugar is transported quickly and efficiently from storage silos to processing units, or from processing units to packaging areas. This streamlined process helps in maintaining the flow of operations and meeting production targets effectively.
Technical Specifications and Customization Options
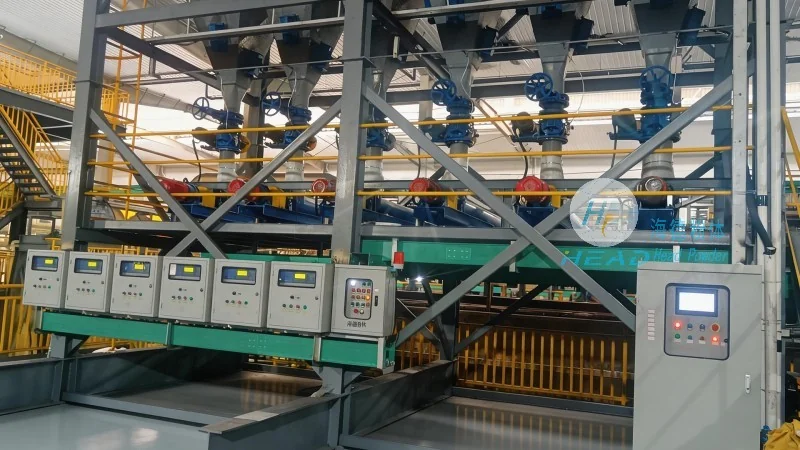
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of sugar pneumatic conveying equipment, offers a range of technical specifications and customization options to meet the diverse needs of sugar processing facilities. The company's systems are designed with robust materials, such as stainless steel, to withstand the corrosive nature of sugar and prevent rust or contamination. The conveying lines are equipped with high-quality valves and check valves to ensure proper air and sugar flow control. The fan or blower units are selected based on the required pressure and airflow, with options ranging from low to high pressure systems, depending on the distance and volume of sugar to be conveyed. Additionally, the company provides customization services to tailor the equipment to specific production requirements, including different hopper sizes, conveying line lengths, and discharge configurations. This flexibility allows sugar processing plants to optimize their material handling processes according to their unique operational needs, ensuring maximum efficiency and cost-effectiveness.