

Working Principle and Features of Gravity Dust Removal Pneumatic Conveying Systems
Gravity dust removal pneumatic conveying systems represent a sophisticated solution for handling and transporting fine particulate materials in industrial settings. These systems are designed to efficiently separate dust from air streams while simultaneously conveying the collected material to designated storage or processing locations. The technology integrates principles of gravity separation and pneumatic transport, offering a cost-effective and reliable method for material handling in various industries such as cement, mining, and chemical processing.
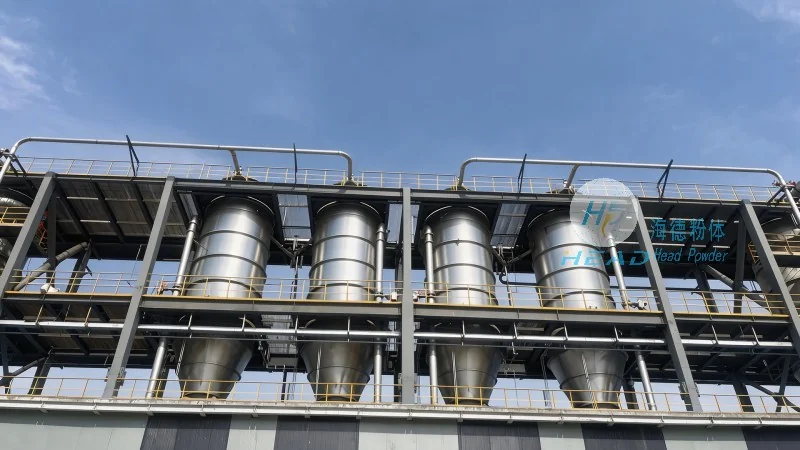
Understanding the Working Principle of Gravity Dust Removal Pneumatic Conveying Systems
The core of a gravity dust removal pneumatic conveying system lies in its dual-stage operation. Initially, the system draws in air containing fine dust particles through an inlet. As the air passes through a gravity separator, the heavier dust particles settle due to gravitational forces, while the lighter air continues to flow. This separation process is critical for capturing the bulk of the particulate matter, preventing it from being carried along with the air stream and potentially causing blockages or contamination in downstream equipment. The collected dust is then discharged into a hopper or collection bin, while the cleaned air is either recirculated or vented to the atmosphere, depending on the system design and environmental regulations.
Following the separation stage, the system transitions to the pneumatic conveying phase. The air, now relatively free of dust, is directed through a series of ducts and valves to transport the material from the collection hopper to the target destination. This conveying process relies on the velocity and pressure of the air to move the material, often using positive pressure or negative pressure (suction) methods. The design of the ductwork, including bends, elbows, and expansion joints, is carefully engineered to minimize pressure loss and ensure smooth material flow. The system may also incorporate features like pulse-jet cleaning or vibration to maintain the efficiency of the separation and conveying stages.
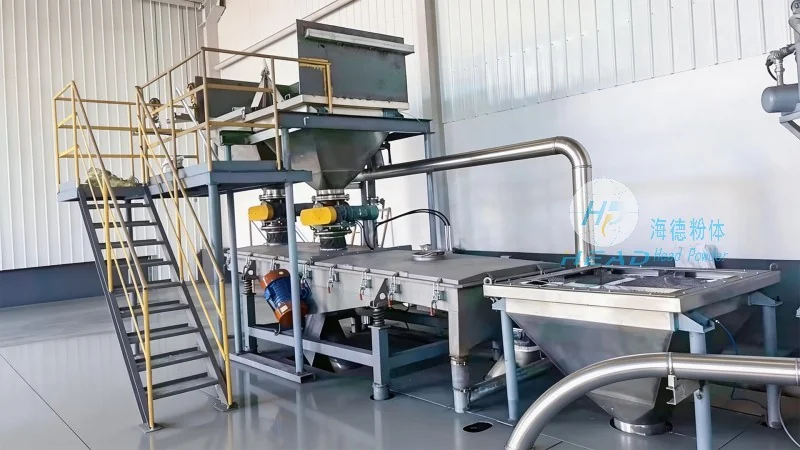
Key Features and Advantages of Gravity Dust Removal Pneumatic Conveying Systems
One of the primary advantages of these systems is their ability to handle a wide range of dust types and particle sizes. The gravity separation stage effectively captures particles from microns to millimeters, making it suitable for diverse applications. Additionally, the system operates with minimal moving parts, reducing maintenance requirements and extending the lifespan of the equipment. This simplicity contributes to lower operational costs and higher reliability compared to more complex systems.
Another notable feature is the energy efficiency of gravity dust removal pneumatic conveying systems. By separating the dust from the air stream early, the system reduces the load on the conveying equipment, allowing for lower air pressure and velocity requirements. This translates into reduced energy consumption and operational costs. Furthermore, the system’s compact design makes it suitable for installation in confined spaces, optimizing factory layouts and maximizing available floor space.
The systems also offer flexibility in material handling. They can be integrated with existing dust collection equipment, such as baghouses or electrostatic precipitators, to enhance overall dust control. The collected material can be stored in bulk containers or fed directly into processing lines, streamlining the material flow and improving operational efficiency. The modular design of these systems allows for easy expansion or modification to accommodate changing production needs.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of industrial material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing gravity dust removal pneumatic conveying systems tailored to the specific needs of various industries. HeadPowder’s expertise lies in combining advanced engineering principles with practical application, ensuring that their systems deliver optimal performance and reliability. The company’s commitment to customer satisfaction and technical excellence has established it as a trusted partner in the field of industrial material handling.
HeadPowder’s headquarters are located in Shandong, China, where the company maintains a state-of-the-art research and development facility. This facility enables continuous improvement of their products through rigorous testing and innovation. The company’s team of experienced engineers and technicians work closely with clients to understand their operational challenges and develop customized solutions that meet their unique requirements. By leveraging their deep industry knowledge and technical capabilities, HeadPowder ensures that their gravity dust removal pneumatic conveying systems are not only efficient but also cost-effective and sustainable for long-term use.