

[W]Working Principle and Features of Carbon Black and Coal Powder Pneumatic Conveying Systems
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for carbon black and coal powder applications. With a strong presence in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable material transport. This article delves into the working principle and key features of such systems, highlighting how they enhance operational efficiency and safety in bulk material handling.
Understanding the Working Principle of Pneumatic Conveying Systems
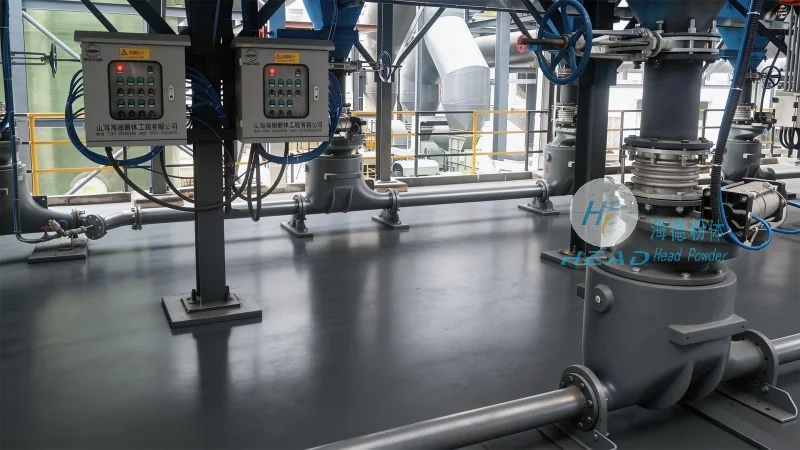
Pneumatic conveying systems utilize air or gas as the medium to transport bulk materials like carbon black and coal powder from one location to another. The core mechanism involves a series of components that work in tandem to achieve this transport. Typically, the system starts with a material hopper or feeder where the powder is stored. An air compressor then generates the necessary pressure to draw the material into the conveying line. As the air flows through the pipeline, it carries the powder particles along, ensuring a continuous and controlled movement. The system may include features such as rotary valves, filters, and pressure regulators to maintain optimal performance and prevent material degradation or blockages. The entire process is designed to be energy-efficient and low-maintenance, making it suitable for high-volume applications in industries like chemical manufacturing, power generation, and mining.
Key Features of Carbon Black and Coal Powder Pneumatic Conveying Systems
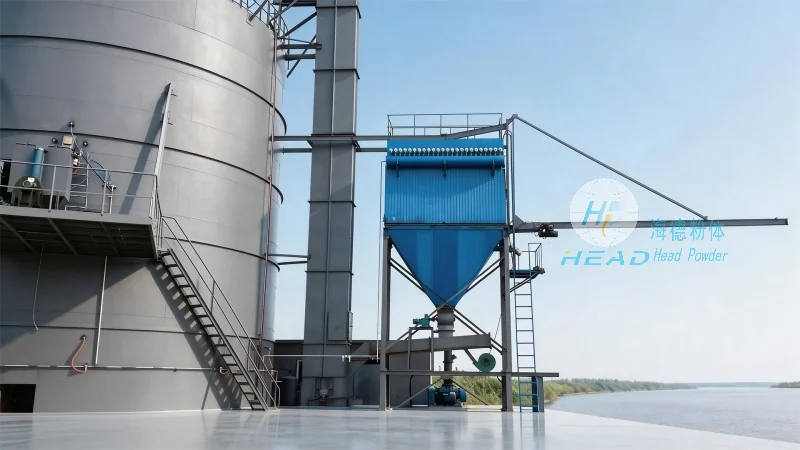
HeadPowder's pneumatic conveying systems for carbon black and coal powder are engineered with several distinctive features that set them apart in the market. Firstly, the systems are equipped with advanced control systems that allow for precise regulation of air pressure and flow rates. This ensures consistent material transport, minimizing variations in delivery and preventing overloading or underloading of downstream equipment. Secondly, the use of high-quality materials in the construction of pipelines and components ensures durability and resistance to corrosion, which is crucial when handling abrasive powders like carbon black. The systems also incorporate dust collection and filtration mechanisms to maintain air quality and comply with environmental regulations. Additionally, the design allows for easy integration with existing production lines, reducing downtime during installation and operation. These features collectively contribute to improved operational reliability, reduced maintenance costs, and enhanced safety for personnel and equipment.
Benefits and Applications in Industrial Settings
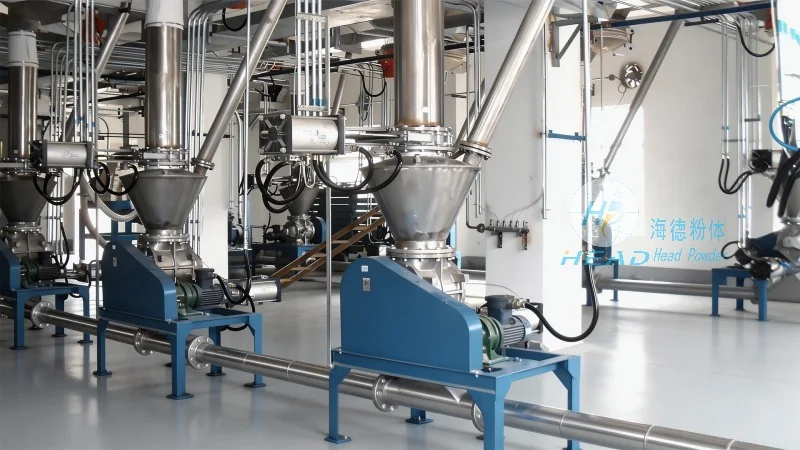
The implementation of pneumatic conveying systems for carbon black and coal powder offers numerous benefits to industrial operations. By eliminating the need for traditional bulk handling methods such as trucks or conveyor belts, these systems significantly reduce labor costs and operational complexity. The continuous flow of material ensures a steady supply to processing units, improving overall productivity and reducing bottlenecks in production. Furthermore, the enclosed nature of the system minimizes dust exposure, enhancing workplace safety and compliance with health regulations. HeadPowder's systems are particularly well-suited for applications in power plants, where coal is transported to boilers, and in chemical plants, where carbon black is used in the production of tires and other rubber products. The company's expertise in customizing systems to meet specific client requirements ensures that each installation is optimized for the unique demands of the application, whether it involves high-volume transport over long distances or precise dosing for quality control.
Conclusion and Company Overview
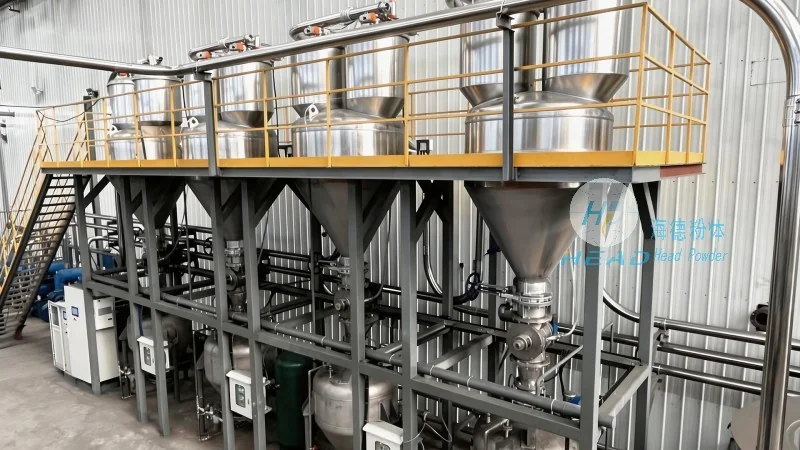
HeadPowder Engineering Co., Ltd., based in Shandong, China, continues to lead the industry in providing innovative and efficient pneumatic conveying solutions for carbon black and coal powder. By combining advanced technology with a deep understanding of material handling challenges, the company delivers systems that enhance operational efficiency, reduce costs, and improve safety. The working principle of these systems, centered on air-based transport, coupled with key features like precise control and durable construction, makes them an ideal choice for modern industrial applications. As industries strive for greater efficiency and sustainability, HeadPowder remains committed to delivering solutions that meet the evolving needs of bulk material transport, ensuring long-term success and reliability for its clients.