

[Detailed Explanation of Red Bean Pneumatic Conveying System]
HeadPowder, a leading enterprise in the field of pneumatic conveying technology, specializes in the design, manufacturing, and installation of advanced material handling systems. Based in Shandong, China, the company has established itself as a trusted provider of efficient and reliable solutions for various industrial applications. This article provides a comprehensive overview of the Red Bean Pneumatic Conveying System, highlighting its key features, operational principles, and practical applications.
Company Profile and Expertise
HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China, and has been at the forefront of developing innovative pneumatic conveying solutions for decades. The company's team of experienced engineers and technicians leverages cutting-edge technology and rigorous quality control processes to deliver systems that meet the highest industry standards. With a strong commitment to customer satisfaction and sustainable operations, HeadPowder has built a reputation for excellence in the material handling sector.
Introduction to the Red Bean Pneumatic Conveying System
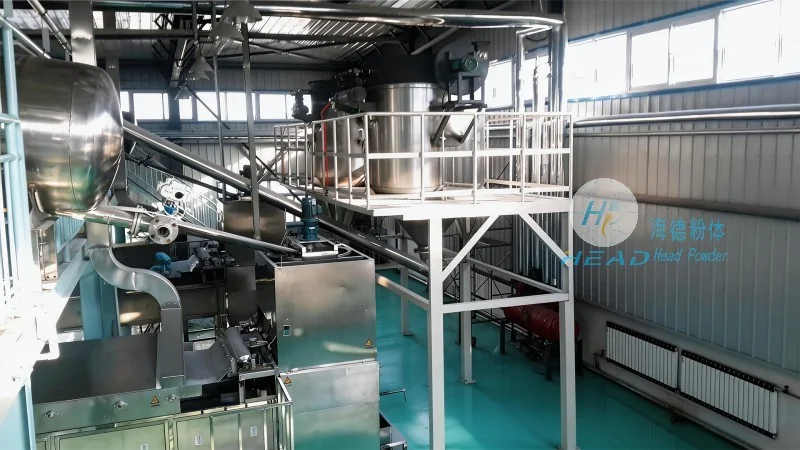
The Red Bean Pneumatic Conveying System is a state-of-the-art solution designed to transport bulk materials such as powders, granules, and fine particles through an air-driven system. This system offers a flexible and efficient alternative to traditional mechanical conveying methods, reducing operational costs and improving process reliability. The system's design incorporates advanced components, including high-efficiency blowers, flexible hoses, and precise control mechanisms, ensuring optimal performance under diverse operational conditions.

Key Technical Features
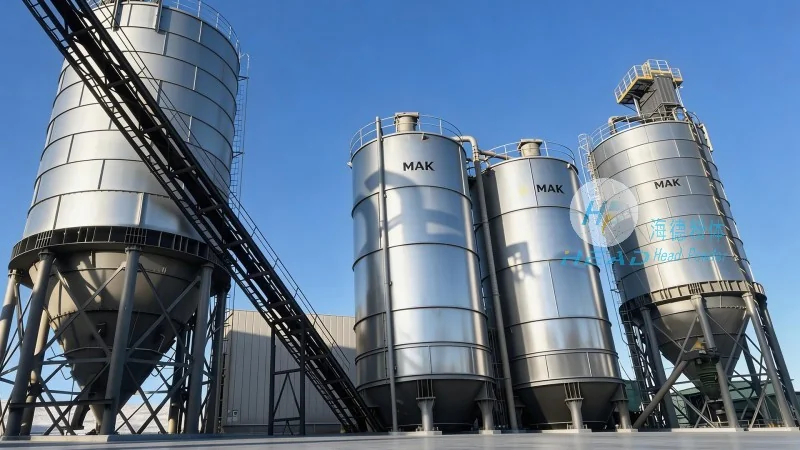
The Red Bean Pneumatic Conveying System is equipped with several key technical features that enhance its functionality and adaptability. One of the primary advantages is its ability to handle a wide range of materials, from low-density powders to high-density granules, with minimal degradation or loss. The system utilizes positive pressure or negative pressure conveying methods, depending on the specific application requirements, to ensure efficient material transport. Additionally, the system incorporates advanced filtration and separation technologies to maintain material purity and prevent contamination. The control system is user-friendly, allowing operators to monitor and adjust conveying parameters in real-time, thereby optimizing process efficiency and reducing downtime.
Operational Advantages and Benefits
Implementing the Red Bean Pneumatic Conveying System brings numerous operational advantages to industrial facilities. Firstly, it significantly reduces labor costs by automating material handling processes, minimizing the need for manual intervention. Secondly, the system minimizes material waste and spillage, contributing to a cleaner and safer working environment. Thirdly, the energy-efficient design of the system lowers operational expenses, making it a cost-effective solution for long-term use. Furthermore, the system's modular design allows for easy integration with existing production lines and scalability to accommodate future growth. These benefits collectively enhance overall productivity and profitability for businesses across various industries.
Application Scenarios
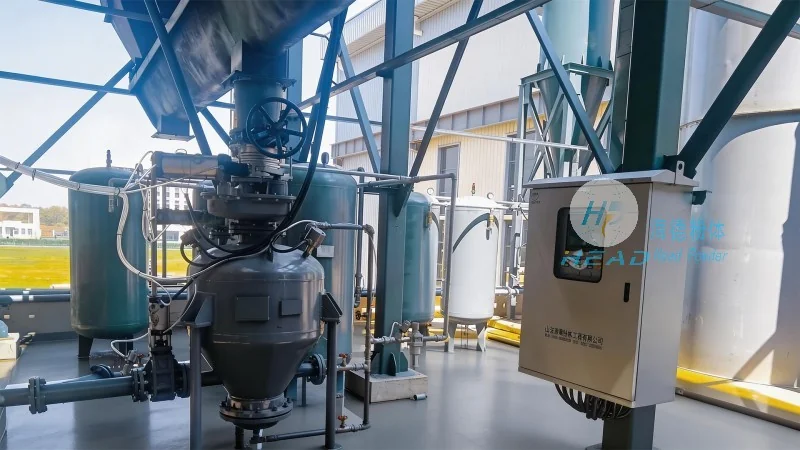
The Red Bean Pneumatic Conveying System is versatile and can be applied in a wide array of industrial sectors. In the food and pharmaceutical industries, it is used to transport ingredients, powders, and finished products with strict hygiene and contamination control requirements. In the chemical and petrochemical sectors, the system efficiently handles hazardous materials while ensuring safety and compliance with regulatory standards. The system is also widely used in the mining and mineral processing industries for transporting raw materials and byproducts. Additionally, in the agricultural and food processing industries, it facilitates the handling of grains, seeds, and other bulk agricultural products. The adaptability of the system makes it suitable for various operational needs, from small-scale operations to large-scale industrial plants.
Conclusion and Contact Information
HeadPowder Engineering Co., Ltd. continues to innovate and provide high-quality pneumatic conveying solutions, including the Red Bean Pneumatic Conveying System. With its advanced technology, operational efficiency, and commitment to customer satisfaction, the company remains a leading choice for businesses seeking reliable material handling systems. For more information or to explore how the Red Bean Pneumatic Conveying System can enhance your industrial processes, please contact HeadPowder Engineering Co., Ltd. based in Shandong, China.