

Airflow Transport Solutions for Heptahydrate Magnesium Sulfate
Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industrial applications. Efficient and reliable material handling is crucial for optimizing production processes, and airflow conveying technology offers a sophisticated approach to transporting this material. This article explores the specialized solutions provided by Shandong HeadPowder Engineering Co., Ltd. for the air-based transport of heptahydrate magnesium sulfate, highlighting key considerations and technical advantages.
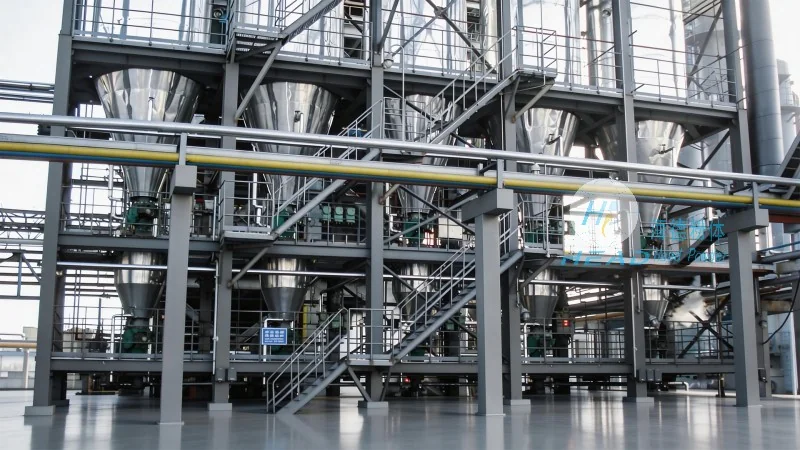
Understanding Heptahydrate Magnesium Sulfate and Its Handling Requirements
Heptahydrate magnesium sulfate (MgSO₄·7H₂O) is a hygroscopic, crystalline solid that requires careful handling to maintain its quality and prevent degradation. Traditional conveying methods, such as belt conveyors or screw conveyors, may introduce friction, heat, or moisture variations that can affect the material's properties. Airflow conveying, or pneumatic transport, addresses these challenges by using compressed air to move the material through a pipeline system. This method minimizes direct contact with equipment, reducing the risk of contamination and preserving the material's integrity.
Key Features of Airflow Conveying Systems for Heptahydrate Magnesium Sulfate
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing airflow conveying systems tailored to the unique characteristics of heptahydrate magnesium sulfate. These systems incorporate several critical features to ensure optimal performance. First, the use of low-pressure or high-pressure pneumatic transport, depending on the distance and material flow rate, allows for gentle material handling. The system includes components such as rotary air locks, dust collectors, and material feeders that work in tandem to maintain consistent material flow and prevent blockages. Additionally, the design incorporates corrosion-resistant materials, such as stainless steel or specialized coatings, to withstand the chemical properties of the magnesium sulfate and prevent equipment degradation over time.
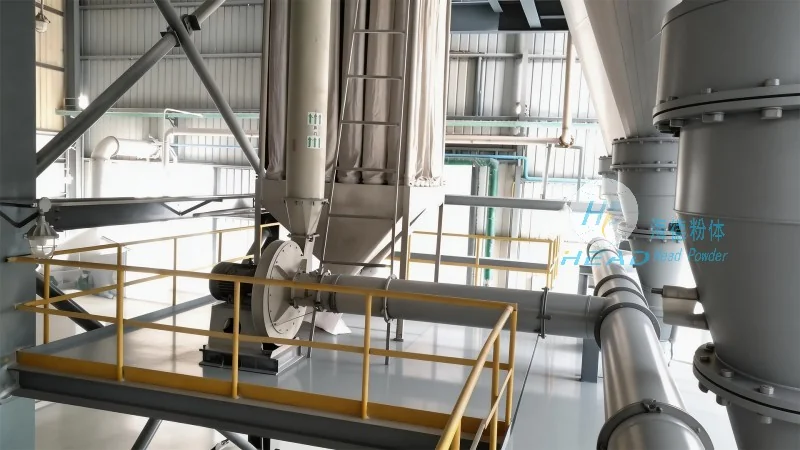
Advantages of Airflow Conveying Solutions
Implementing an airflow conveying system for heptahydrate magnesium sulfate offers several advantages over conventional methods. One of the primary benefits is the ability to transport material over long distances without the need for intermediate transfer points, which reduces operational complexity and maintenance requirements. The system also provides better control over material moisture content, as the air flow can be adjusted to maintain the desired humidity levels. Furthermore, airflow conveying minimizes dust generation and improves workplace safety by containing the material within a closed pipeline system. This not only enhances operational efficiency but also aligns with environmental regulations by reducing emissions and improving air quality.
Customization and Integration with Existing Facilities
Shandong HeadPowder Engineering Co., Ltd. recognizes that each industrial facility has unique operational needs and existing infrastructure. Therefore, their solutions are highly customizable to integrate seamlessly with current production lines. The company's engineers work closely with clients to assess existing equipment, space constraints, and material flow patterns to design a system that maximizes efficiency while minimizing disruption to ongoing operations. Customization may include adjusting pipeline diameters, selecting appropriate air pressure levels, or incorporating additional filtration systems to meet specific quality standards. This tailored approach ensures that the airflow conveying solution is not only effective but also cost-efficient and compatible with the client's long-term goals.
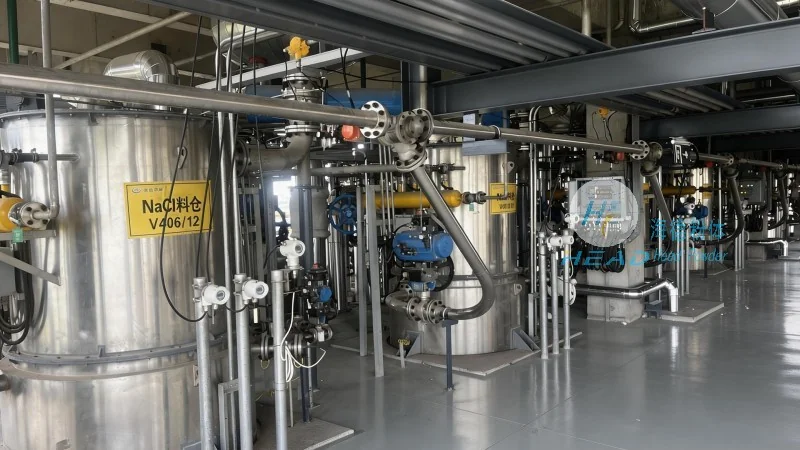
Installation and Maintenance Considerations
The successful implementation of an airflow conveying system for heptahydrate magnesium sulfate requires careful planning and professional installation. Shandong HeadPowder Engineering Co., Ltd. employs experienced technicians who follow industry best practices to ensure proper setup and commissioning. Regular maintenance is also essential to maintain the system's performance and longevity. The company provides comprehensive maintenance services, including routine inspections, component replacement, and troubleshooting support, to keep the system operating at peak efficiency. By adhering to a proactive maintenance schedule, clients can minimize downtime and maximize the return on their investment in the airflow conveying solution.
Conclusion: Enhancing Efficiency with Airflow Conveying Solutions
For industries relying on heptahydrate magnesium sulfate, the choice of material handling technology significantly impacts production efficiency and product quality. Airflow conveying solutions, as offered by Shandong HeadPowder Engineering Co., Ltd., provide a reliable and efficient method to transport this material while preserving its integrity. By leveraging specialized engineering and customization, these systems address the unique challenges of handling heptahydrate magnesium sulfate, offering benefits such as reduced contamination, improved safety, and enhanced operational control. As a result, companies can optimize their production processes, reduce costs, and maintain high standards of product quality. Shandong HeadPowder Engineering Co., Ltd. continues to lead in providing innovative and effective airflow conveying solutions, supporting clients in achieving their industrial objectives with precision and reliability.