

What is Corn Kernels Pneumatic Conveying? Classification and Applications of Pneumatic Conveying
Corn kernels pneumatic conveying is a specialized method used in the agricultural and food processing industries to transport bulk materials like corn kernels efficiently. This technology involves using air as the medium to move the material from one location to another, offering advantages such as reduced contamination, improved hygiene, and the ability to handle delicate or sensitive products without mechanical contact. Understanding the principles and applications of this system is crucial for businesses in the grain processing sector.
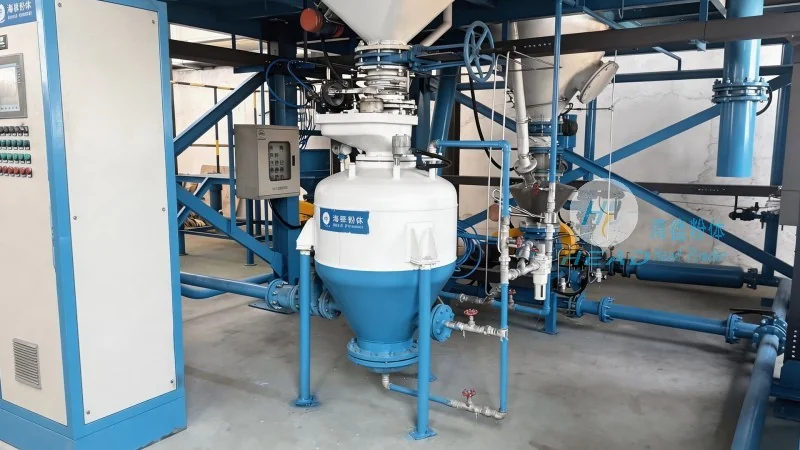
Understanding Pneumatic Conveying Systems
Pneumatic conveying systems are designed to transport bulk materials through a pipeline using air pressure or vacuum. The process typically involves a hopper or storage bin where the corn kernels are loaded, a conveyor line with a series of pipes, and a receiver or discharge point where the material is deposited. The system can operate under pressure (positive pressure) or vacuum (negative pressure), depending on the application and material characteristics. For corn kernels, which are relatively light and have a consistent size, positive pressure systems are often preferred as they provide efficient and gentle handling.
Types of Pneumatic Conveying for Corn Kernels
There are primarily two types of pneumatic conveying systems used for corn kernels: dilute phase and dense phase. Dilute phase systems operate with a low concentration of material in the air stream, typically at a velocity that keeps the material suspended. This method is suitable for short to medium distances and offers high throughput. Dense phase systems, on the other hand, use higher air pressure and lower velocity to move material in a more concentrated form, which is ideal for longer distances and more delicate materials that require minimal agitation. Both systems have their applications in corn processing, and the choice depends on factors like distance, material properties, and desired throughput.
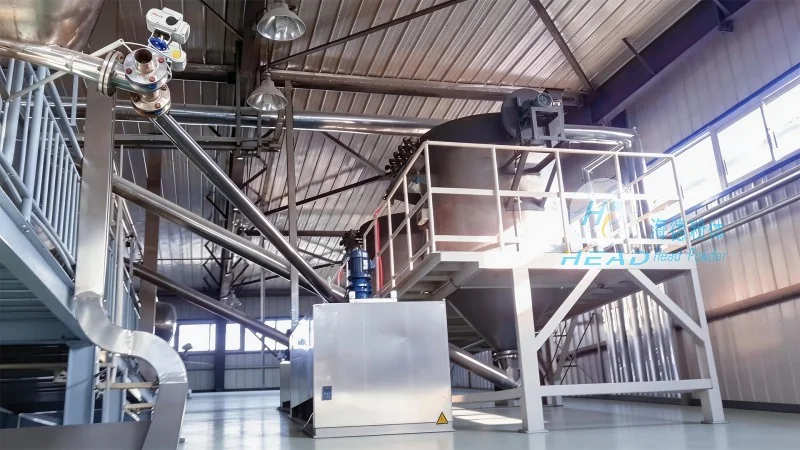
Applications of Corn Kernels Pneumatic Conveying
The applications of corn kernels pneumatic conveying span various stages of the corn processing industry. In the initial stages, it is used to transfer raw corn kernels from storage silos to processing facilities, ensuring a continuous supply of raw material. During processing, the system can be employed to move kernels between different processing units, such as from cleaning and grading to milling or drying. Additionally, it is used in the packaging stage to transport processed corn products, like cornmeal or grits, to packaging lines. The technology is also beneficial in the storage and distribution of corn products, allowing for efficient movement of bulk materials to warehouses or distribution centers. Overall, pneumatic conveying enhances operational efficiency and reduces labor costs by automating the material handling process.
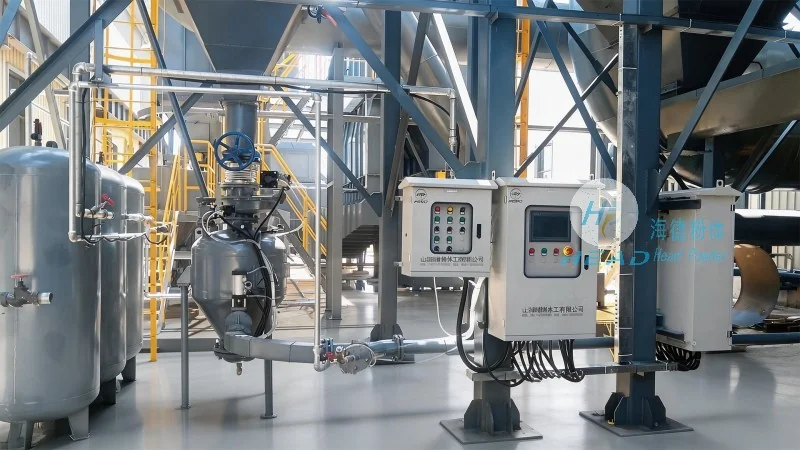
Benefits of Using Pneumatic Conveying for Corn Kernels
Implementing a pneumatic conveying system for corn kernels offers several key benefits. Firstly, it minimizes product contamination and damage as the material is not in direct contact with mechanical components, which is particularly important for food-grade products. Secondly, the system improves hygiene and sanitation, as it can be easily cleaned and maintained, reducing the risk of bacterial growth or cross-contamination. Thirdly, it enhances operational efficiency by automating the material handling process, reducing downtime and increasing throughput. Fourthly, it provides flexibility in system design, allowing for easy integration with existing processing equipment and expansion as production needs grow. These benefits make pneumatic conveying a preferred choice for modern corn processing facilities.
About HeadPowder: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the needs of the agricultural and food processing industries. With years of experience and a commitment to quality, HeadPowder provides customized solutions for corn kernels and other bulk materials, ensuring efficient and reliable material handling. The company's products are designed to meet industry standards and customer requirements, offering durability and performance in demanding environments. HeadPowder's expertise in pneumatic conveying technology helps businesses optimize their operations and improve overall productivity.