

Introduction to the Pneumatic Conveying of Quicklime Powder and Its Structural Principles
Quicklime powder, also known as calcium oxide powder, is a widely used industrial material in various sectors such as construction, chemical manufacturing, and environmental treatment. The efficient and reliable transportation of quicklime powder is crucial for industrial processes, and pneumatic conveying systems have emerged as a preferred method due to their ability to handle fine powders like quicklime with minimal dust generation and high transport efficiency. This article provides an overview of the pneumatic conveying process for quicklime powder, detailing its structural components and operational principles.
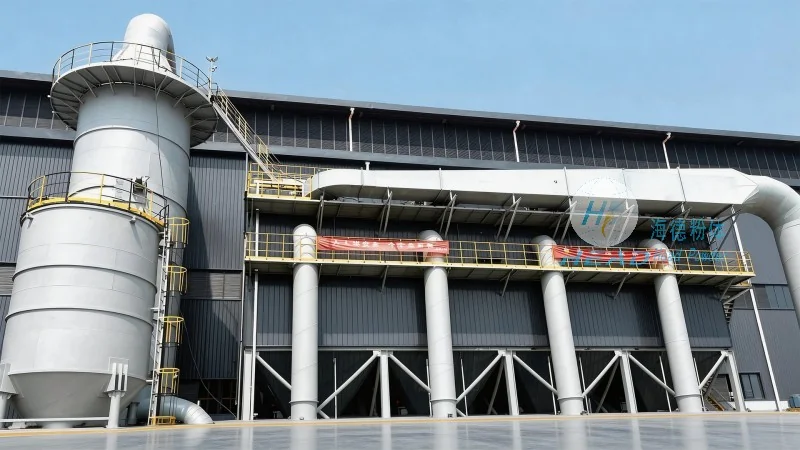
Structural Principles of Pneumatic Conveying Systems
The core of a pneumatic conveying system for quicklime powder involves several key components that work in tandem to ensure effective material transport. The system typically includes a material feed unit, a conveying pipeline, a pressure or vacuum source, and a collection or separation device. The feed unit, often a rotary valve or a screw feeder, introduces the quicklime powder into the system at a controlled rate. This is followed by the pipeline, which can be either positive pressure or negative pressure (or a combination) depending on the application. The pressure source, such as a blower or a vacuum pump, generates the airflow that propels the powder particles through the pipeline. The separation device, such as a cyclone or a bag filter, separates the powder from the air at the end of the conveying line, allowing the powder to be collected in a designated container.
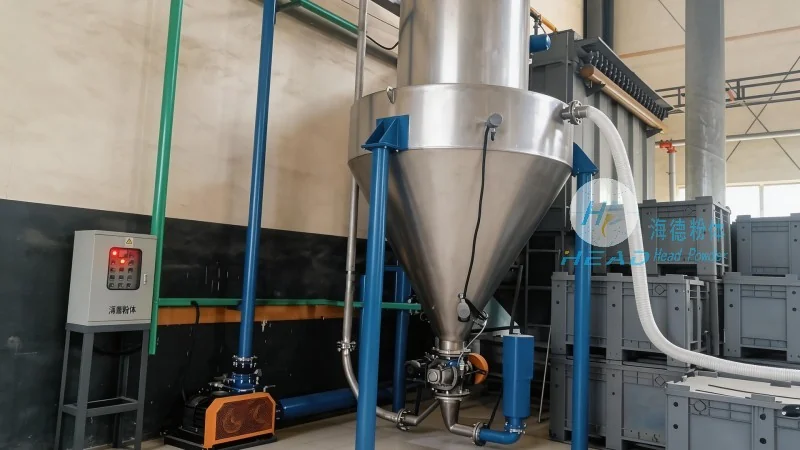
Key Components and Their Functions
Each component of the pneumatic conveying system plays a critical role in the successful transport of quicklime powder. The material feed unit ensures a consistent and controlled flow of powder into the system, preventing blockages and maintaining system efficiency. The conveying pipeline, usually made of materials like stainless steel or plastic, is designed to withstand the pressure and temperature conditions of quicklime powder transport. The pressure source provides the necessary airflow to move the powder particles, with the velocity of the air being a critical factor in preventing particle deposition and ensuring smooth transport. The separation device is essential for recovering the quicklime powder from the air stream, minimizing dust emissions and maintaining environmental compliance.
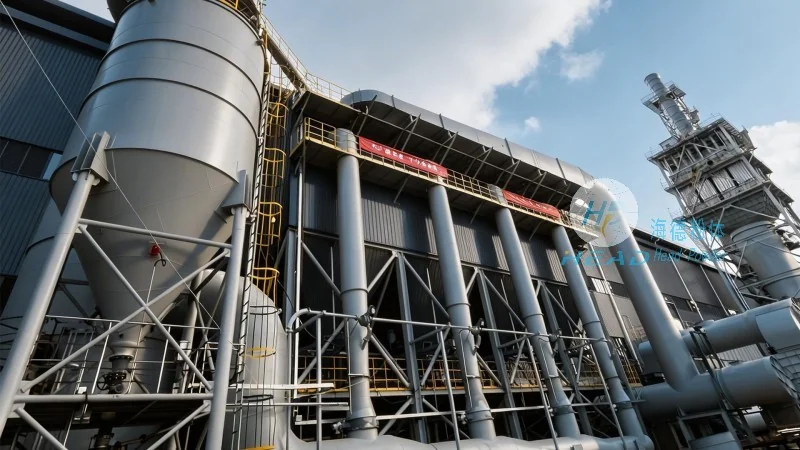
Applications and Benefits of Pneumatic Conveying for Quicklime Powder
Pneumatic conveying systems are widely used in industries that handle quicklime powder due to their numerous advantages over traditional methods like bucket elevators or belt conveyors. These systems offer advantages such as reduced dust generation, lower maintenance requirements, and the ability to transport powders over long distances without the need for multiple transfer points. Additionally, pneumatic conveying systems can be integrated with other processing equipment, such as reactors or mixers, to create a seamless production line. The benefits of using pneumatic conveying for quicklime powder include improved safety, as it eliminates the need for manual handling of powders, and enhanced product quality, as the system minimizes contamination and degradation of the powder.
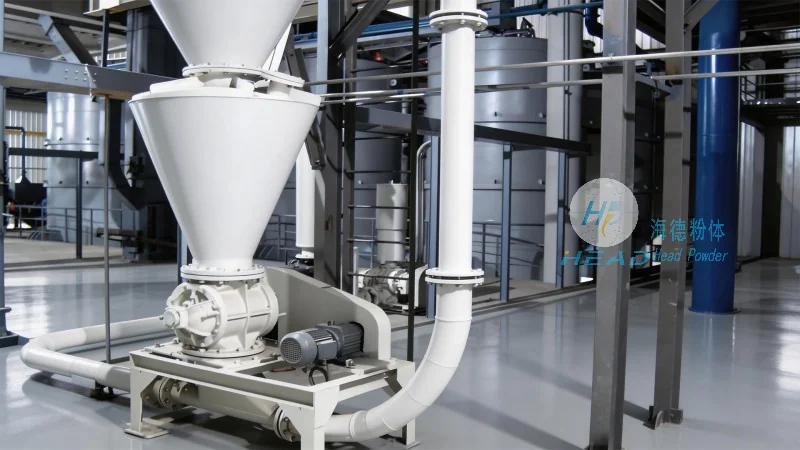
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment for industrial applications. With a focus on innovation and quality, HeadPowder provides customized solutions for the transportation of various powders, including quicklime powder. The company's expertise lies in designing and manufacturing efficient, reliable, and cost-effective pneumatic conveying systems that meet the specific needs of its clients. HeadPowder's products are known for their durability, low maintenance, and high performance, making them a preferred choice for industries that require consistent and safe powder transport. The company is headquartered in Shandong, China, and serves clients worldwide with its advanced technology and professional service.