

Operation Process and Working Principle of High-Pressure Dilute-Phase Pneumatic Conveying Systems
High-pressure dilute-phase pneumatic conveying systems represent a sophisticated technology used for transporting bulk materials over long distances with high efficiency and minimal operational issues. These systems are particularly valuable in industries such as chemical processing, food and beverage, and mining, where the need to move powders and granules safely and effectively is paramount. The operation of such systems involves a series of integrated components working in concert to achieve reliable material transport. Developed and manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, these systems are designed to meet the diverse needs of modern industrial applications.
Key Components and Their Roles
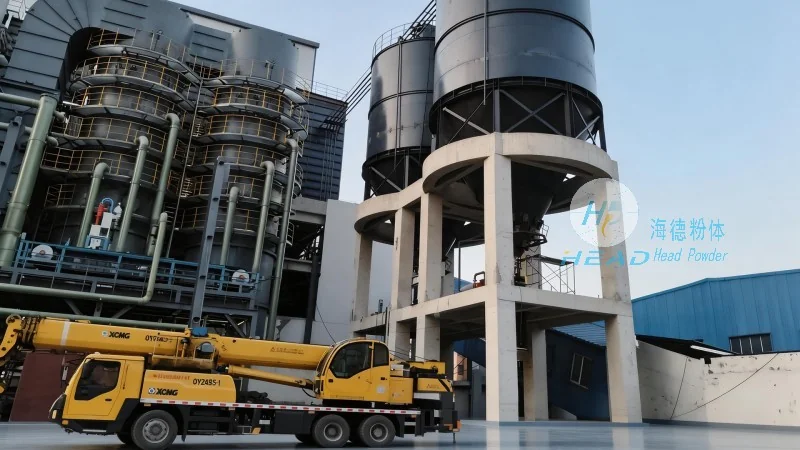
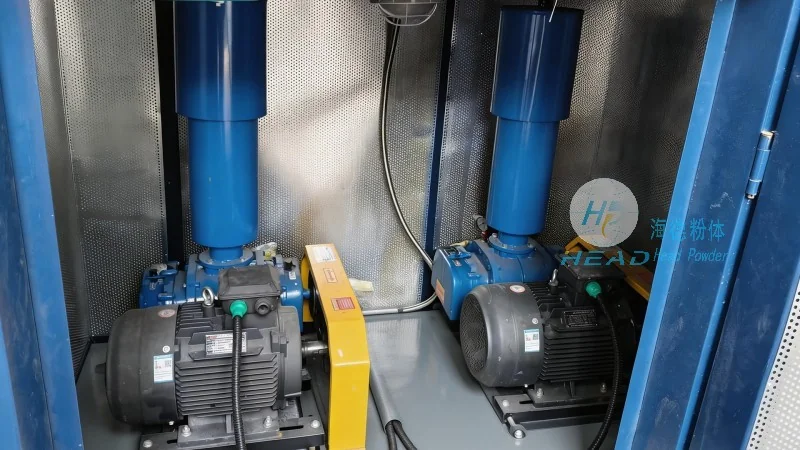
At the core of a high-pressure dilute-phase pneumatic conveying system are several critical components that ensure smooth operation. The system typically includes a positive displacement blower or compressor to generate the necessary air pressure, a hopper or feeder to introduce the material into the system, a pipeline network to transport the material, and a receiver or discharge unit to collect the material at the destination. Each component plays a vital role in maintaining the system's performance and efficiency. The blower provides the driving force, while the feeder controls the material flow rate, ensuring consistent operation. The pipeline design is crucial for minimizing pressure drop and preventing material degradation or blockages. The receiver at the end of the pipeline collects the material, completing the transport process.
Working Principle of the System
The working principle of a high-pressure dilute-phase pneumatic conveying system is based on the creation of a dilute mixture of material particles suspended in a high-velocity air stream. The system operates by drawing air from the blower and mixing it with the material from the hopper. The air, under high pressure, carries the material particles through the pipeline. The velocity of the air is maintained at a level sufficient to keep the particles suspended, preventing them from settling or clogging the pipeline. This dilute-phase operation ensures that the material is transported as a uniform mixture, reducing the risk of agglomeration and ensuring consistent flow characteristics. The high pressure generated by the blower ensures that the material is propelled efficiently through the pipeline, even over long distances.
Operation Process: From Material Loading to Discharge
The operation process of a high-pressure dilute-phase pneumatic conveying system begins with the loading of material into the hopper. The feeder then regulates the material flow into the pipeline, ensuring a steady supply. The blower or compressor increases the air pressure to the required level, and the air, along with the material, is propelled through the pipeline. The system maintains a consistent pressure and velocity throughout the pipeline to ensure the material is transported without issues. At the receiving end, the material is discharged into a receiver or storage tank. The system may also include controls to monitor pressure, flow rate, and material level, allowing for real-time adjustments to maintain optimal performance. The entire process is designed to be automated, reducing the need for manual intervention and enhancing operational efficiency.
Advantages and Applications
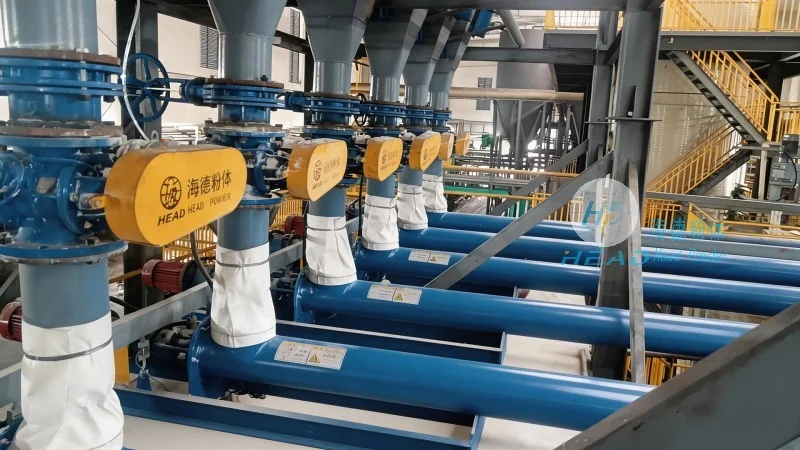
High-pressure dilute-phase pneumatic conveying systems offer several advantages over traditional conveying methods. These include the ability to transport materials over long distances, the reduction of material degradation due to minimal contact with equipment, and the prevention of contamination from external sources. The systems are also flexible, allowing for changes in material type or flow rate without significant modifications. Applications of these systems span various industries, including the chemical industry for transporting powders and granules, the food industry for handling dry ingredients, and the mining industry for transporting ore and other bulk materials. The efficiency and reliability of these systems make them a preferred choice for many industrial applications. Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of such systems, ensuring that clients receive tailored solutions that meet their specific operational requirements.