

Working Principle and Features of Organic Salt Material Transport Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling solutions tailored for organic salt applications. The organic salt material transport system is a sophisticated setup engineered to efficiently manage the movement, storage, and processing of organic salts, which are widely used in various industrial sectors such as chemical manufacturing, food processing, and pharmaceuticals.
Understanding the Working Principle of Organic Salt Material Transport Systems
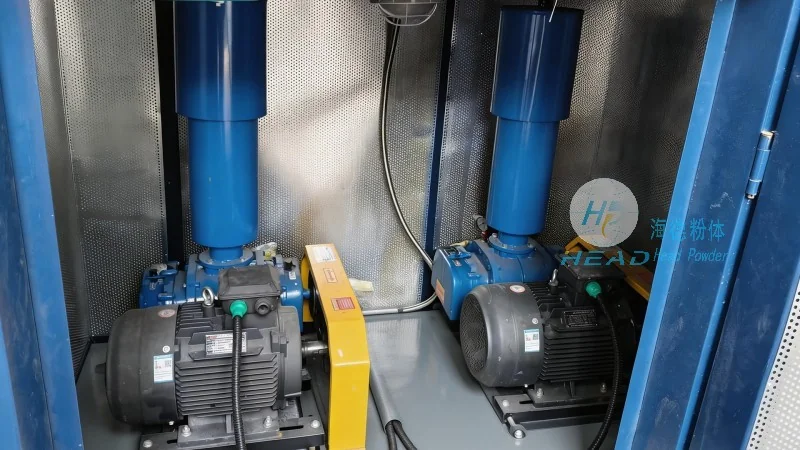
The core working principle of an organic salt material transport system revolves around the integration of several key components, including conveyor mechanisms, storage silos, and control systems. These systems are designed to handle the unique physical and chemical properties of organic salts, which often require specialized handling to prevent degradation or contamination. The process typically begins with the loading of organic salt into a storage silo, where it is stored under controlled conditions to maintain its quality. From the silo, the material is transferred to a conveyor system, which can be either a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the specific requirements of the application. The conveyor system transports the organic salt to the processing or packaging area, where it is further handled by downstream equipment. Advanced control systems are integrated into the setup to monitor and regulate the flow of material, ensuring consistent performance and safety. This integrated approach allows for a seamless and efficient workflow, minimizing downtime and maximizing productivity.
Key Features of Organic Salt Material Transport Systems
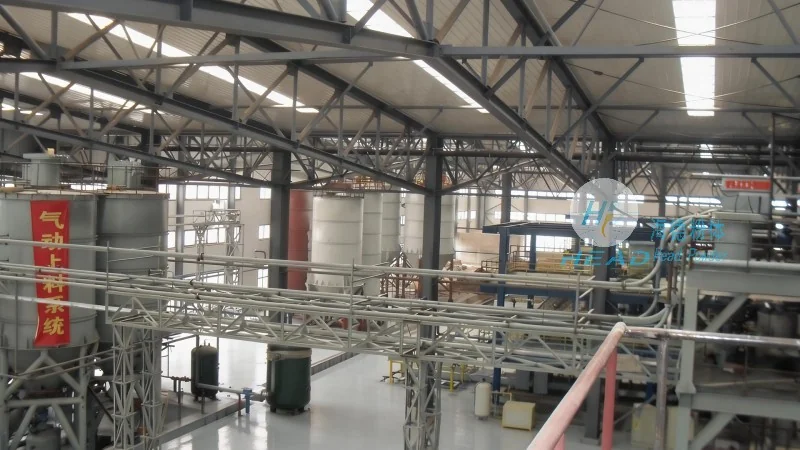
Organic salt material transport systems from HeadPowder are characterized by several distinctive features that set them apart in the industry. Firstly, they are designed with robust construction to withstand the corrosive and abrasive nature of organic salts, ensuring long-term durability and reliability. The systems incorporate high-quality materials, such as stainless steel and corrosion-resistant alloys, to prevent material degradation and equipment failure. Secondly, the systems are equipped with advanced automation and control technologies, enabling precise monitoring and adjustment of the material flow. This automation reduces the need for manual intervention, enhances operational efficiency, and improves safety by minimizing human exposure to the material. Thirdly, the transport systems are highly customizable to meet the specific needs of different applications. Whether it's a small-scale operation or a large industrial facility, the systems can be tailored to handle varying volumes and types of organic salts. Additionally, the systems are designed with safety features, including emergency stop mechanisms and overfill protection, to ensure a secure working environment. These features not only enhance operational safety but also comply with industry regulations and standards.
Efficiency and Reliability in Organic Salt Handling
The efficiency of an organic salt material transport system is a critical factor in industrial operations. The systems are engineered to minimize material loss and contamination, which is essential for maintaining product quality and meeting regulatory requirements. The use of sealed and enclosed conveyor systems helps prevent dust and moisture from entering or exiting the system, ensuring a clean and hygienic environment. This is particularly important in industries like food and pharmaceuticals, where product purity is paramount. Furthermore, the systems are designed to handle different particle sizes and shapes of organic salts, adapting to the specific characteristics of the material being transported. This adaptability allows for versatile applications across various industries. The reliability of the system is also enhanced by regular maintenance and quality control measures. HeadPowder provides comprehensive support, including maintenance services and spare parts availability, to ensure that the systems operate at optimal performance levels. This commitment to reliability helps businesses maintain consistent production schedules and reduce operational costs.
Customization and Application Flexibility
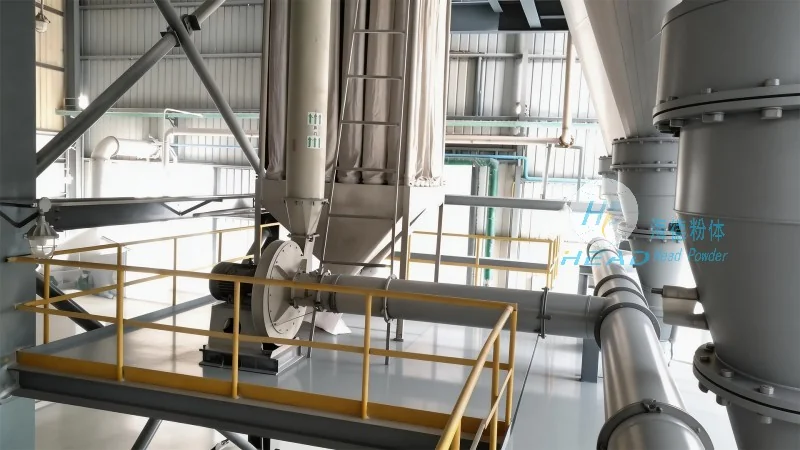
HeadPowder understands that each industrial application has unique requirements, and therefore, their organic salt material transport systems are highly customizable. The systems can be configured with different conveyor types, such as belt conveyors for bulk material handling or screw conveyors for precise dosing. The storage silos can be designed with varying capacities to accommodate different production volumes. Additionally, the control systems can be integrated with existing plant infrastructure, allowing for seamless integration into existing workflows. This flexibility enables businesses to adapt the system to their specific needs, whether it's for small-scale production or large-scale industrial operations. The customization also extends to safety features, where the systems can be equipped with additional safety measures based on the specific hazards associated with the organic salt being handled. This ensures that the system not only meets operational efficiency requirements but also adheres to safety standards and regulations.