

Working Principle and Features of Activated Carbon Material Handling Systems
For industrial applications requiring the efficient and reliable transport of activated carbon, understanding the working principles and key features of specialized material handling systems is crucial. This article provides an in-depth look at how activated carbon material handling systems operate and the advantages they offer to industries such as water treatment, air purification, and chemical processing.
Introduction to Activated Carbon Material Handling Systems
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions in China, specializes in designing and manufacturing advanced material handling systems tailored for activated carbon. With operations based in Shandong, China, the company leverages decades of industry experience to deliver systems that meet the stringent demands of modern industrial processes. The following sections explore the core working principles and distinctive features of these systems, offering insights into their functionality and benefits.

The Working Principle of Activated Carbon Material Handling Systems
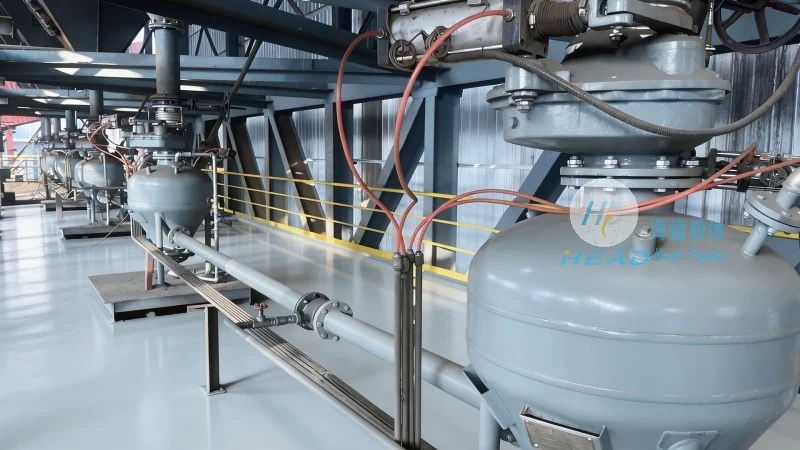
Activated carbon material handling systems are engineered to efficiently transport activated carbon, a highly porous and adsorbent material, from storage to processing units. The primary working principle involves the integration of mechanical and sometimes pneumatic components to ensure smooth and controlled movement. Typically, these systems consist of several key components, including storage silos, conveyor belts, feeding mechanisms, and control systems. The process begins with activated carbon being stored in bulk containers or silos. From there, a feeding device, such as a screw conveyor or a rotary valve, regulates the flow of material into the primary conveyor system. Conveyor belts, often made of durable materials like rubber or metal, transport the activated carbon to the processing or treatment equipment. In some advanced systems, pneumatic conveying is employed, where compressed air is used to move the carbon through pipelines, allowing for more flexible and dust-free transport. The control systems ensure that the flow rate, speed, and direction of the material are precisely managed, preventing overloading or blockages. This integrated approach ensures that the activated carbon is handled safely and efficiently, minimizing loss and maximizing throughput.
Key Features of Activated Carbon Material Handling Systems
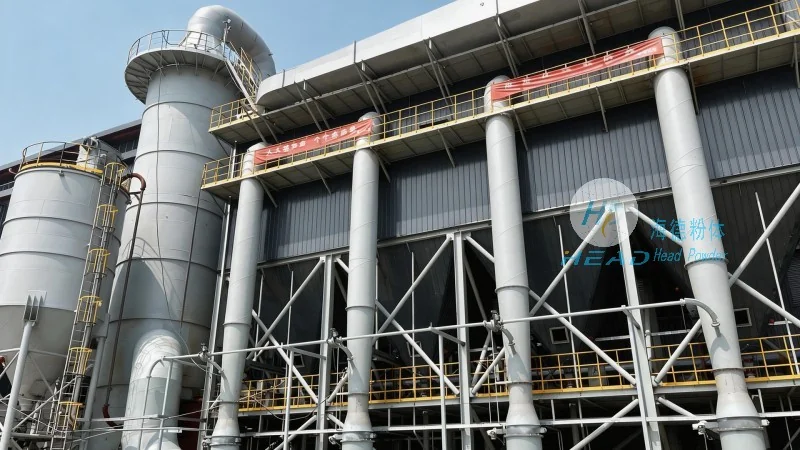
Activated carbon material handling systems from Shandong HeadPowder Engineering Co., Ltd. are distinguished by several key features that enhance performance and reliability. One of the most notable features is their high efficiency in material transport. By optimizing the flow rate and conveyor speed, these systems minimize downtime and maximize production output. The systems are also designed with durability in mind, using high-quality materials that can withstand the abrasive nature of activated carbon, which is known for its fine particles and potential to cause wear on equipment. This durability reduces maintenance costs and extends the operational life of the system. Another critical feature is the emphasis on safety and environmental protection. Activated carbon handling often involves dust, which can be hazardous if not properly contained. The systems incorporate dust suppression mechanisms, such as enclosed conveyor systems and air filtration units, to maintain a safe working environment and comply with environmental regulations. Additionally, the systems are equipped with advanced monitoring and control technologies, allowing operators to track the material flow in real-time and make adjustments as needed. This level of control enhances operational flexibility and ensures consistent performance. The systems also offer adaptability to different operational needs. Whether for small-scale laboratory use or large-scale industrial production, the systems can be customized to meet specific requirements, including varying material volumes and processing speeds. This adaptability makes them suitable for a wide range of applications, from water treatment plants to chemical manufacturing facilities. Furthermore, the systems are designed for easy integration into existing production lines, reducing the need for extensive modifications and ensuring a smooth transition to new processes. The combination of these features makes activated carbon material handling systems from Shandong HeadPowder Engineering Co., Ltd. a reliable choice for industries that require consistent and efficient handling of activated carbon.
Conclusion
In conclusion, activated carbon material handling systems from Shandong HeadPowder Engineering Co., Ltd. are sophisticated solutions designed to address the unique challenges of transporting activated carbon. By understanding the working principles and leveraging the key features of these systems, industries can enhance their operational efficiency, ensure safety, and comply with environmental standards. The company's commitment to quality and innovation, combined with its expertise in material handling, positions it as a trusted partner for businesses seeking reliable and effective activated carbon transport solutions. Whether for new installations or system upgrades, these systems provide a robust foundation for optimizing industrial processes and achieving superior performance.