

Sulfuric Nickel Powder Conveying System Equipment: What It Is and Its Design Principles
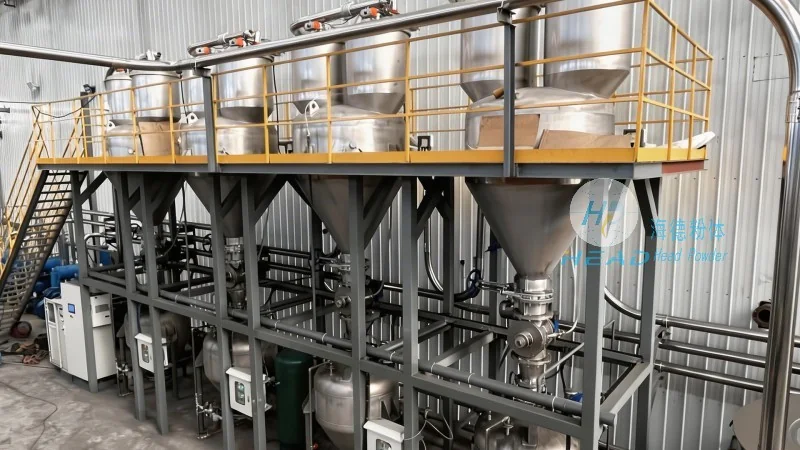
Sulfuric nickel powder conveying system equipment is a specialized industrial solution designed to handle the transportation and processing of nickel sulfate powders. This type of equipment is crucial in various industrial applications, particularly in the battery manufacturing sector where nickel compounds are essential raw materials. The system integrates multiple components to ensure efficient, safe, and reliable movement of the powder from one processing stage to another. As a key component in material handling, these systems are engineered to meet the specific demands of nickel sulfate handling, including considerations for dust control, material flow optimization, and operational safety.
Design Principles of Sulfuric Nickel Powder Conveying Systems
The design of sulfuric nickel powder conveying systems is based on several fundamental principles that ensure optimal performance and safety. First, the system must address the unique properties of nickel sulfate powders, such as their hygroscopic nature and potential for dust generation. Engineers from Shandong HeadPowder Engineering Co., Ltd. focus on creating a closed-loop system to minimize exposure to moisture and air, which can affect the powder's quality and handling characteristics. The design incorporates advanced materials and components that are resistant to corrosion and chemical reactions, as nickel sulfate is a reactive compound that can degrade or react with certain metals and surfaces.
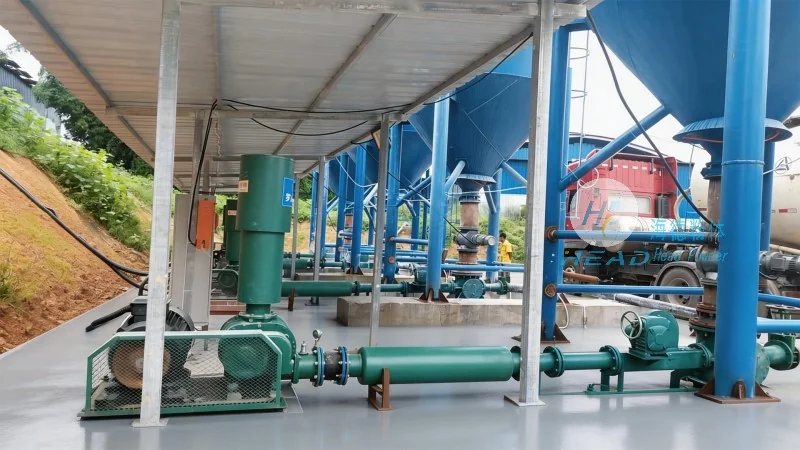
Second, the system emphasizes efficient material flow. This involves selecting appropriate conveyor types, such as screw conveyors, pneumatic conveyors, or bucket elevators, based on the specific characteristics of the nickel sulfate powder. For example, screw conveyors are often used for horizontal or slight incline transport due to their ability to handle bulk materials without the need for external air pressure. Pneumatic conveyors, on the other hand, are suitable for vertical or long-distance transport, utilizing air pressure to move the powder through a pipeline. The design also considers the density and flowability of the powder, ensuring that the chosen conveyor type can maintain consistent and controlled flow rates.
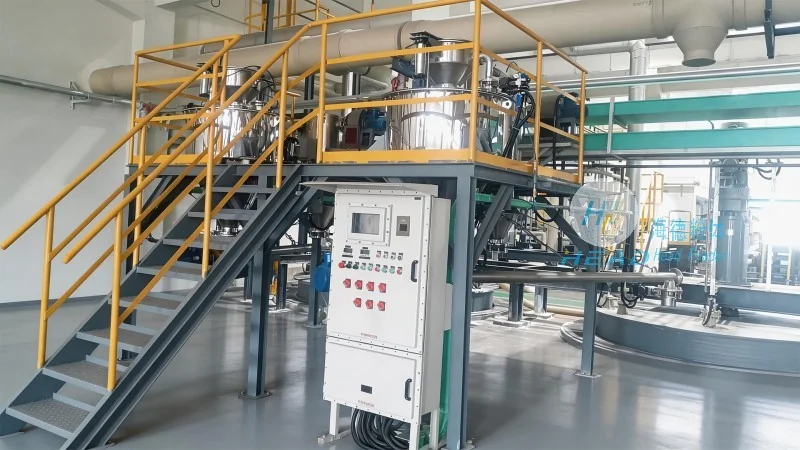
Third, safety and environmental considerations are integral to the design. The system incorporates dust collection and filtration systems to prevent the release of nickel sulfate particles into the environment, which is critical for compliance with environmental regulations and occupational health standards. Additionally, the equipment is designed with explosion-proof features and proper ventilation to mitigate the risks associated with handling powders that may be combustible under certain conditions. The use of sealed and enclosed components reduces the risk of dust accumulation and potential fire hazards, ensuring a safe working environment for operators.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of specialized powder handling equipment, including sulfuric nickel powder conveying systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industrial sector, particularly for applications involving nickel compounds. HeadPowder's engineering team combines extensive industry experience with advanced technology to develop customized solutions that meet the unique needs of clients. The company's facilities in Shandong, China, are equipped with state-of-the-art manufacturing capabilities and rigorous quality control processes to ensure that each system meets the highest standards of performance and reliability.
Conclusion
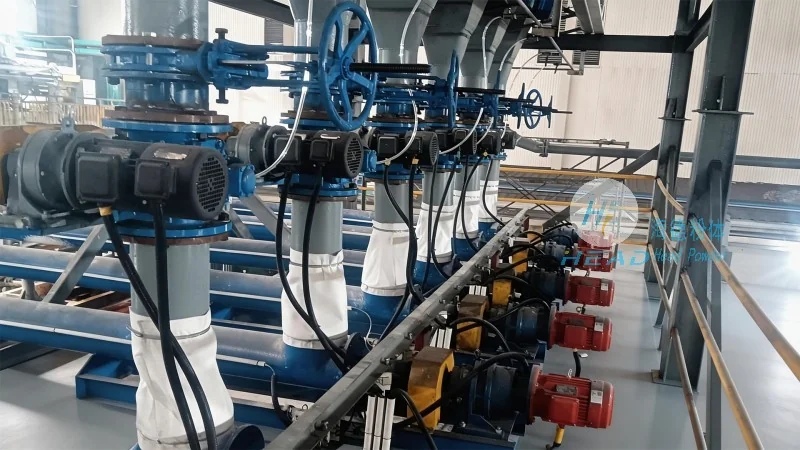
Sulfuric nickel powder conveying system equipment is a sophisticated industrial solution that plays a vital role in the efficient and safe handling of nickel sulfate powders. The design principles behind these systems, developed by experts like those at Shandong HeadPowder Engineering Co., Ltd., prioritize material flow efficiency, safety, and environmental compliance. By integrating advanced components and adhering to strict engineering standards, these systems ensure consistent performance and reliability in various industrial applications. For industries relying on nickel compounds, investing in a well-designed conveying system is essential for optimizing production processes and maintaining operational safety.