

What is a Mung Bean Powder Conveying System Equipment? What Are Its Design Principles?
Understanding the Mung Bean Powder Conveying System Equipment and Its Design Principles
Introduction to Mung Bean Powder Conveying Systems
A mung bean powder conveying system is a specialized industrial equipment designed to handle, transport, and manage mung bean powder efficiently. This system is crucial in industries like food processing, pharmaceuticals, and chemical manufacturing, where consistent and hygienic powder handling is essential. The equipment ensures mung bean powder is moved between processing stages without contamination or loss, maintaining product quality and operational efficiency.
Key Components of the Mung Bean Powder Conveying System
The mung bean powder conveying system typically includes several key components working together to achieve effective powder handling. These components are:
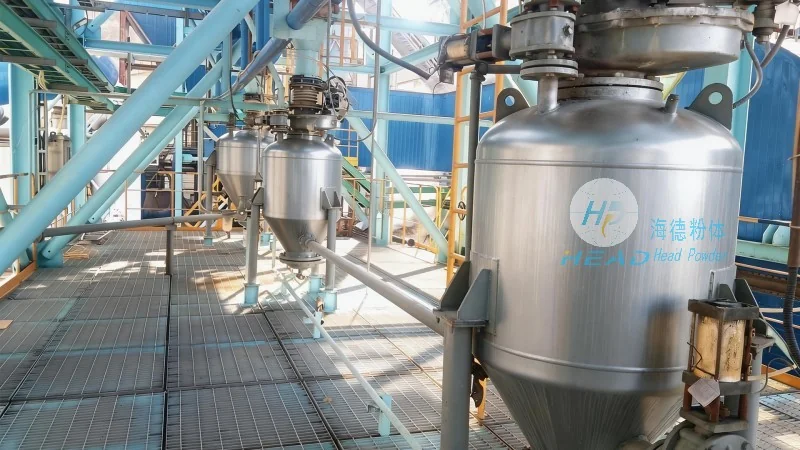
1. Feeding Hopper: This initial component loads mung bean powder. It features a sloped bottom to facilitate powder flow into the conveyor system and includes a discharge valve to control flow rate.
2. Pneumatic Conveying Lines: These lines use compressed air to transport powder through a network of pipes. The system may use positive or negative pressure systems based on application needs.
3. Conveying Equipment: Options include screw conveyors, pneumatic conveyors, or bucket elevators. The choice depends on powder characteristics, transport distance, and desired flow rate.
4. Control Panel: This monitors and regulates system operation, allowing operators to adjust air pressure, flow rate, and conveyor speed for optimal performance.
5. Cleaning and Maintenance Systems: These ensure hygiene and prevent clogging, with easy access points for maintenance.
Design Principles Behind the Mung Bean Powder Conveying System
The system's design is based on principles to ensure efficiency, safety, and product integrity. These include:
1. Hygienic Design: Constructed from easy-to-clean materials like stainless steel, with smooth surfaces and minimal dead zones to prevent powder accumulation and contamination.
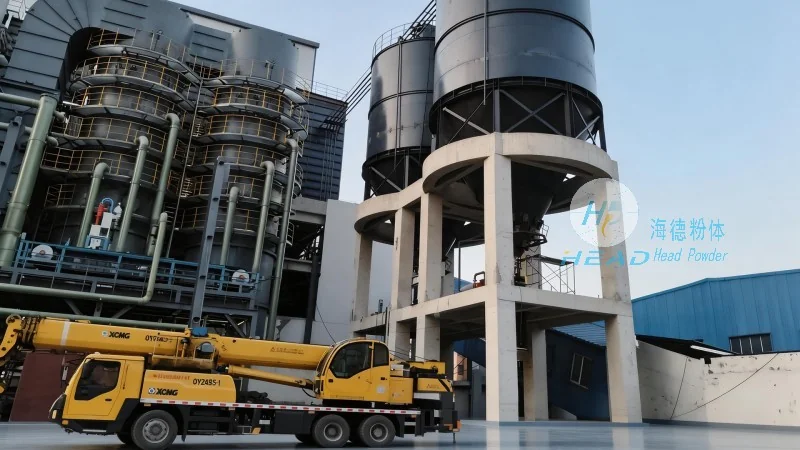
2. Efficient Material Handling: Minimizes material degradation and loss during transport by using appropriate conveying speeds and pressures to avoid particle breakage.
3. Energy Efficiency: Engineered to use energy efficiently, optimizing air pressure and flow rates to reduce consumption while maintaining performance.
4. Flexibility and Scalability: Allows easy integration with existing production lines and can be scaled to accommodate varying production volumes.
5. Safety Features: Includes pressure relief valves, emergency stop buttons, and interlocks to prevent accidents and ensure operator safety.
Operational Workflow of the Mung Bean Powder Conveying System
The operational workflow typically follows these steps:
1. Powder Loading: Mung bean powder is loaded into the feeding hopper, with the hopper's design ensuring smooth flow into the system.
2. Conveying: Powder is transported via pneumatic lines or other equipment, using compressed air to move it from the hopper to the next processing stage.
3. Distribution: Powder is distributed to processing units like mixing tanks, storage silos, or packaging machines.
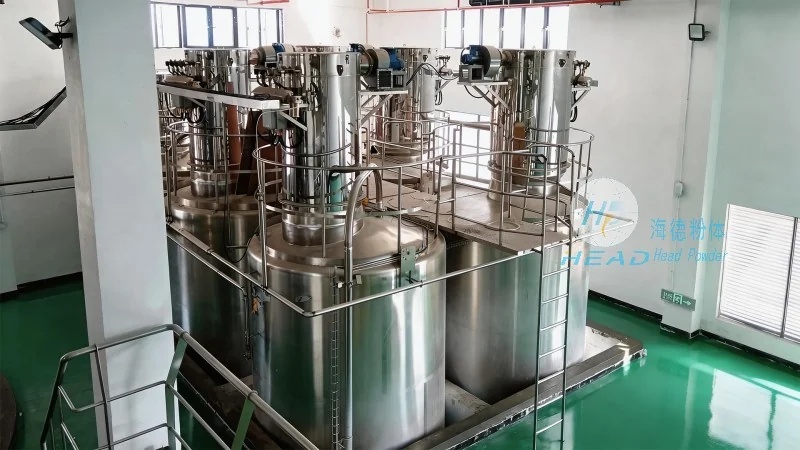
4. Monitoring and Control: The control panel continuously monitors performance, adjusting parameters as needed to maintain optimal operation.
5. Cleaning and Maintenance: Regular cleaning and maintenance are performed to keep the system in good working condition and prevent issues.
Applications and Benefits of the Mung Bean Powder Conveying System
The system is widely used due to its efficiency and reliability, offering several key benefits:
1. Improved Product Quality: Consistent and hygienic handling reduces contamination risk and maintains product quality.
2. Increased Operational Efficiency: Automation reduces labor costs and boosts production throughput.
3. Reduced Waste: Efficient conveying minimizes material loss, leading to cost savings.
4. Enhanced Safety: Safety features protect operators and prevent accidents.
5. Flexibility: Easily adapts to different production requirements and integrates with other equipment.
Conclusion
The mung bean powder conveying system is vital in industries handling mung bean powder. Its design, based on hygienic handling, efficiency, and safety principles, ensures effective powder transport while maintaining quality. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, specialize in designing and manufacturing such systems, providing reliable solutions for diverse industrial applications.