

What is a Silica Aerated Conveyor? And What Are Its Design Principles?
For industries dealing with silica powder, efficient and reliable material handling is crucial. Silica aerated conveyors represent a sophisticated solution to this challenge, offering a method to transport fine powders like silica with precision and minimal loss. This article explores the fundamental aspects of silica aerated conveyors, including their design principles and operational mechanisms.
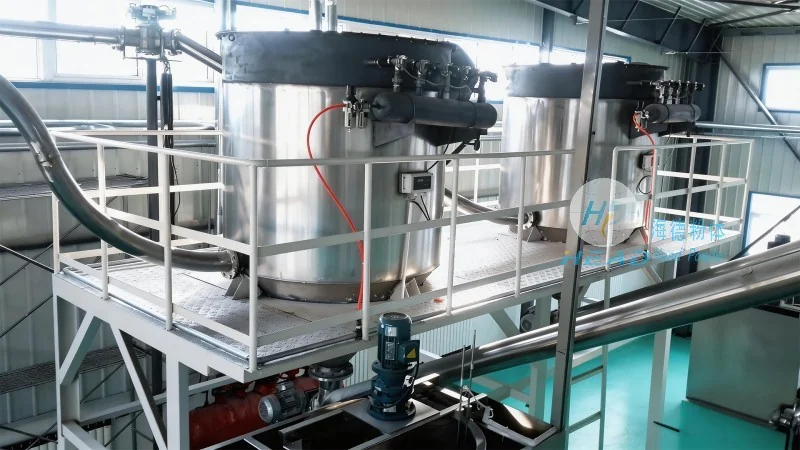
What is a Silica Aerated Conveyor?
A silica aerated conveyor, also known as a pneumatic conveyor, is a system designed to transport dry, fine materials such as silica powder through a pipeline using compressed air. Unlike traditional mechanical conveyors, this system relies on air pressure to move the material, making it ideal for handling delicate or abrasive powders that could be damaged by mechanical contact. The process involves feeding the silica powder into a hopper, where it is mixed with a controlled amount of air, creating a slurry-like mixture that flows through the pipeline to the destination point.
The Core Design Principles of Silica Aerated Conveyors
The design of a silica aerated conveyor is built on several key principles to ensure optimal performance. The first principle is the balance of air and material flow. Engineers must calculate the precise ratio of air to silica to achieve a stable, uniform flow without causing blockages or excessive pressure drops. This ratio is critical for maintaining the conveyor's efficiency and preventing material degradation. Second, the system must incorporate appropriate pressure control mechanisms. The compressed air system is typically equipped with regulators and valves to maintain consistent pressure, which directly impacts the conveying velocity and distance. Third, the pipeline design is crucial for minimizing friction and pressure loss. Smooth, corrosion-resistant pipes are used to reduce wear and tear on the material and the system components. Additionally, the system includes features like air locks and cyclones to separate the material from the air at the discharge point, ensuring clean and efficient material handling.
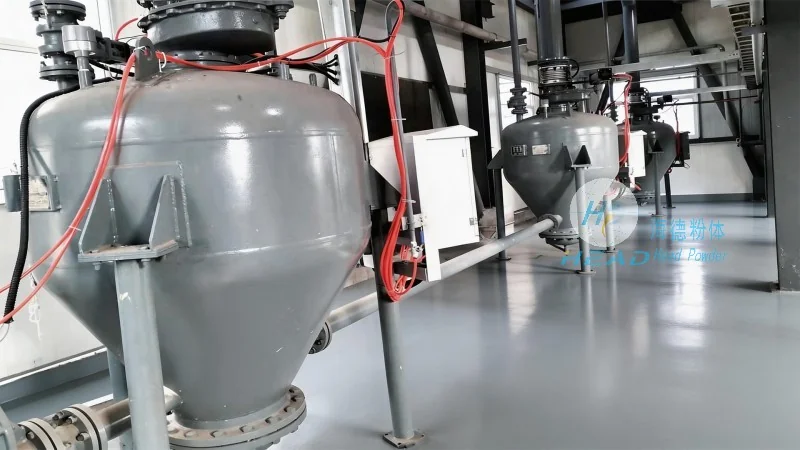
Key Components and Their Functions
Several key components make up a silica aerated conveyor system. The hopper is the primary feeding device, where silica powder is stored and fed into the system. It is designed to prevent material buildup and ensure a consistent flow. The air compressor supplies the necessary compressed air, which is regulated to maintain the required pressure. The pipeline network connects the hopper to the discharge point, and its design is critical for efficient material transport. The air lock or rotary valve at the discharge end prevents backflow and ensures that the material is discharged cleanly. The cyclone separator is another essential component, as it separates the silica powder from the air stream, allowing the air to be recycled back into the system and the powder to be collected for further use. Each component works in tandem to ensure the system operates smoothly and efficiently.
Application Scenarios and Benefits
Silica aerated conveyors are widely used in various industries, particularly those dealing with fine powders. In the chemical industry, they are used to transport silica-based products, such as silica gel or fumed silica, from production lines to storage or packaging areas. In the construction industry, they help transport silica sand for concrete production or other construction materials. The benefits of using a silica aerated conveyor include reduced labor costs, as the system can operate continuously without manual intervention. It also minimizes material loss and contamination, as the enclosed system prevents dust and debris from escaping. Furthermore, the system is compact and can be installed in tight spaces, making it suitable for facilities with limited room. The ability to handle abrasive materials without damage is another significant advantage, as the pneumatic method avoids mechanical wear and tear.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of material handling solutions, specializes in designing and manufacturing silica aerated conveyors. With a strong focus on quality and innovation, the company has developed advanced systems that meet the needs of various industries. HeadPowder's products are known for their durability, efficiency, and reliability, making them a trusted choice for businesses dealing with silica and other fine powders. The company's headquarters is located in Shandong, China, where it has a team of experienced engineers and technicians dedicated to research and development. HeadPowder's commitment to customer satisfaction and product excellence has earned it a reputation as a leading supplier in the material handling industry.