

Types and Practical Applications of Pneumatic Conveying Systems in Sugar Transportation
Pneumatic conveying systems play a crucial role in the efficient and reliable transportation of sugar within industrial and processing facilities. As a key component of material handling infrastructure, these systems are designed to move bulk materials like sugar from one location to another, ensuring smooth operations and maintaining product quality. The selection of an appropriate pneumatic conveying system depends on various factors, including the type of sugar, processing requirements, and the specific layout of the facility. Understanding the different types and practical applications of these systems is essential for optimizing sugar handling processes.
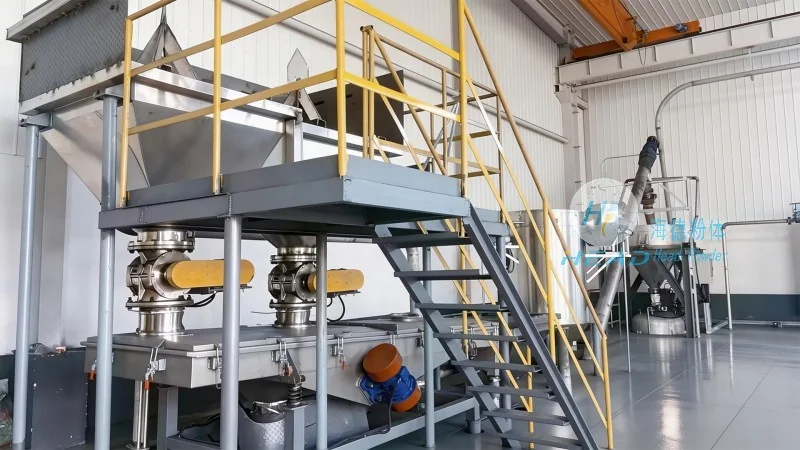
Types of Pneumatic Conveying Systems Used in Sugar Transportation
There are several types of pneumatic conveying systems commonly employed in sugar transportation, each with its own advantages and suitability for different operational conditions. The primary categories include positive pressure systems, negative pressure systems, and hybrid systems. Positive pressure systems, such as pressure vessels and blowers, generate air pressure to push the material through the system. These systems are often preferred for long-distance or high-capacity applications due to their ability to maintain consistent flow rates and handle abrasive materials like sugar without significant wear. Negative pressure systems, on the other hand, use vacuum to draw the material into the system, which is typically more suitable for short-distance or low-volume operations. Hybrid systems combine elements of both positive and negative pressure, offering flexibility in handling different material characteristics and operational needs.
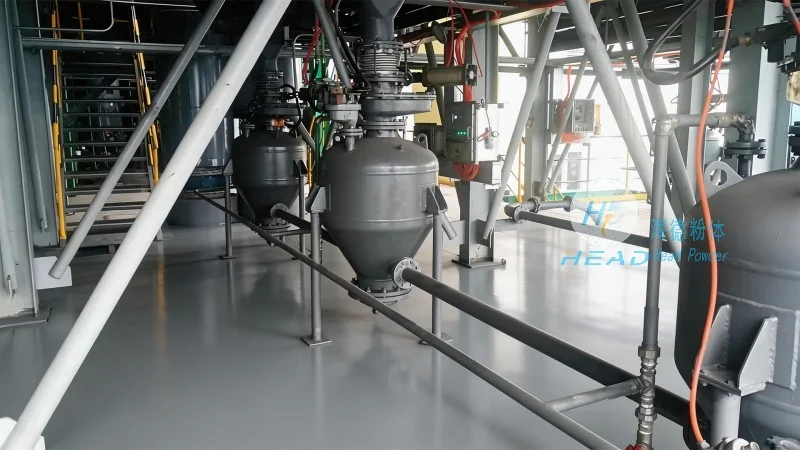
Practical Applications of Pneumatic Conveying Systems in Sugar Handling
In the sugar industry, pneumatic conveying systems are utilized in various stages of the processing and distribution chain. One common application is the transfer of raw sugar from storage silos to processing equipment, such as crushers and grinders. This process requires efficient and dust-free movement of the material to prevent contamination and ensure consistent quality. Another practical application is the transportation of refined sugar from the refining stage to packaging lines, where precise control over the flow rate is critical to maintain product integrity. Additionally, pneumatic conveying systems are used in bulk handling operations, such as loading and unloading sugar from trucks or ships, enabling seamless integration with logistics and supply chain management. The systems are also employed in quality control and sampling processes, where small quantities of sugar need to be transported to testing laboratories for analysis. By providing a clean and efficient method of material transport, these systems contribute to overall operational efficiency and product quality in sugar processing facilities.

Key Considerations for Selecting a Pneumatic Conveying System for Sugar Transportation
When selecting a pneumatic conveying system for sugar transportation, several key factors must be considered to ensure optimal performance and longevity. The first consideration is the type of sugar being handled, as different varieties may have varying moisture content, particle size, and flow characteristics. For example, granulated sugar may require different system design parameters compared to powdered sugar. The second factor is the distance and capacity requirements, as these directly impact the system's pressure and power needs. Additionally, the system's ability to handle abrasive materials and prevent product degradation is crucial, as sugar can be sensitive to friction and temperature changes. Maintenance and operational costs are also important considerations, as regular maintenance is required to ensure the system operates efficiently and reliably. Finally, compliance with industry standards and regulations regarding dust control and safety is essential, especially in facilities handling bulk materials like sugar.
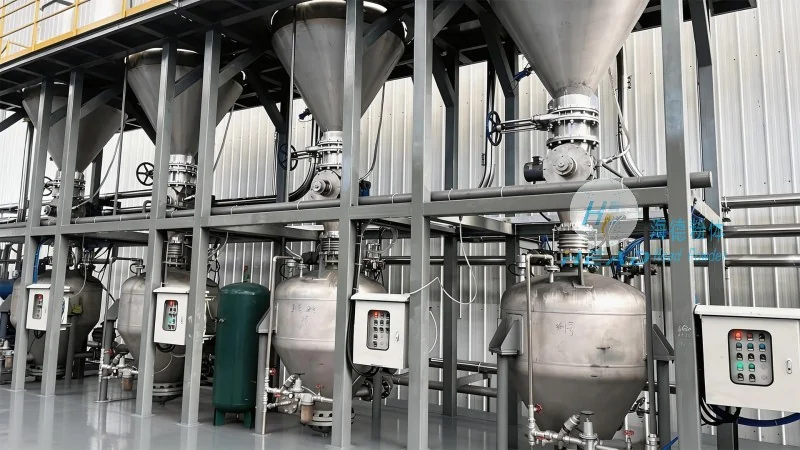
Conclusion and Company Overview
Pneumatic conveying systems are indispensable in modern sugar transportation and processing operations, offering efficient, clean, and reliable solutions for moving bulk materials. The appropriate selection and implementation of these systems can significantly enhance operational efficiency, reduce downtime, and maintain product quality. Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for material handling, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of the sugar industry. With a focus on innovation and quality, the company has established itself as a trusted partner in optimizing sugar handling processes. Based in Shandong, China, HeadPowder Engineering leverages advanced technology and expertise to deliver solutions that meet the highest standards of performance and reliability. By understanding the diverse applications and considerations of pneumatic conveying systems, sugar processing facilities can make informed decisions to improve their operational capabilities and ensure long-term success.