

Introduction to Fertilizer Granule Conveying Systems and the Advantages of Pneumatic Conveying for G
For agricultural and industrial applications, the efficient and reliable transport of fertilizer granules is crucial for maintaining productivity and ensuring product quality. This article introduces the fertilizer granule conveying system, highlighting the key advantages of pneumatic conveying technology. The system is designed and manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions based in Shandong, China.
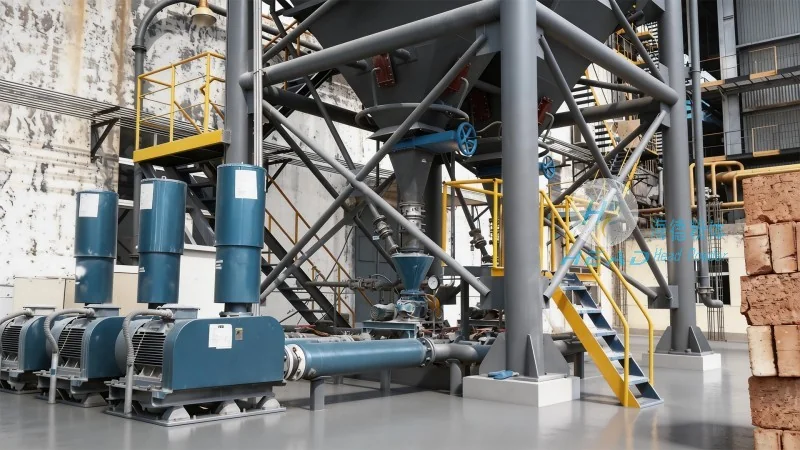
Introduction to Fertilizer Granule Conveying Systems
The fertilizer granule conveying system is a specialized equipment setup used to transport granular fertilizers from storage silos or production lines to processing units, storage facilities, or application points. These systems are engineered to handle various types of granular fertilizers, including nitrogen, phosphorus, and potassium-based products, as well as blended or customized formulations. The core components of such a system typically include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline network, and a dust collection system to ensure environmental compliance and operational safety.
The Advantages of Pneumatic Conveying for Granular Fertilizers
Pneumatic conveying, also known as air conveying, offers several significant advantages over traditional mechanical conveying methods for fertilizer granules. One of the primary benefits is the high efficiency in material transport, as it can move large volumes of granular fertilizer over considerable distances with minimal energy consumption. The system operates by using compressed air to create a flow that carries the granules through the pipeline, reducing the need for mechanical components like belts or buckets that may experience wear and tear over time. This results in lower maintenance costs and increased operational longevity. Additionally, pneumatic conveying systems provide flexibility in layout design, allowing for complex pipeline configurations that can adapt to the specific spatial constraints of a facility. The technology also ensures a dust-free environment, which is essential for maintaining product purity and adhering to environmental regulations. Furthermore, the system can be integrated with automated controls, enabling precise control over the conveying process and enhancing overall operational efficiency.
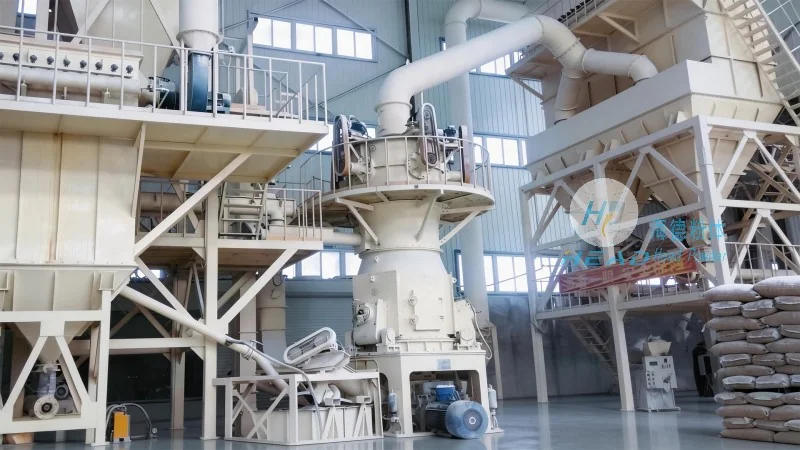
Key Features of the Fertilizer Granule Conveying System
The fertilizer granule conveying system developed by Shandong HeadPowder Engineering Co., Ltd. incorporates several key features that enhance its performance and reliability. The system utilizes high-quality materials, such as stainless steel or corrosion-resistant alloys, to ensure durability and resistance to the chemical properties of fertilizers. The conveying pipeline is designed with smooth, low-friction surfaces to minimize material degradation and reduce blockage risks. The feeder mechanism is equipped with advanced control algorithms that adjust the flow rate based on real-time demand, preventing overfilling or underfilling. The dust collection system includes high-efficiency filters and a pressure relief valve to maintain safe operating conditions and comply with local air quality standards. Furthermore, the system is equipped with monitoring sensors that provide real-time data on pressure, flow rate, and temperature, allowing for proactive maintenance and troubleshooting.
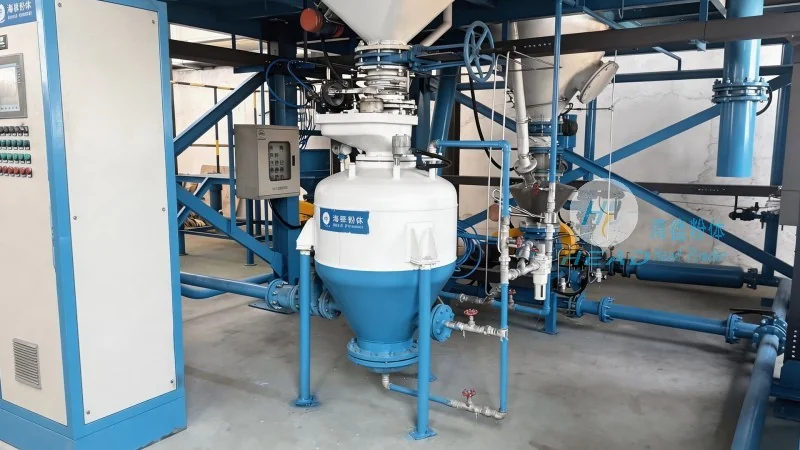
Application Scenarios and Operational Benefits
The fertilizer granule conveying system is widely used in various applications across the agricultural and industrial sectors. In agricultural settings, it is commonly employed in fertilizer manufacturing plants to transport raw materials and finished products to storage silos or distribution centers. The system is also utilized in farm operations to move granular fertilizers from bulk storage to application equipment, such as spreaders or injectors. In industrial applications, the system is used in chemical and petrochemical facilities to transport blended fertilizers or specialty products to processing units. The operational benefits of the system include increased throughput, reduced labor costs, and improved product quality. By minimizing material handling time and ensuring consistent flow rates, the system helps to optimize production schedules and reduce downtime. Additionally, the dust-free operation contributes to a safer working environment and lower health risks for personnel.
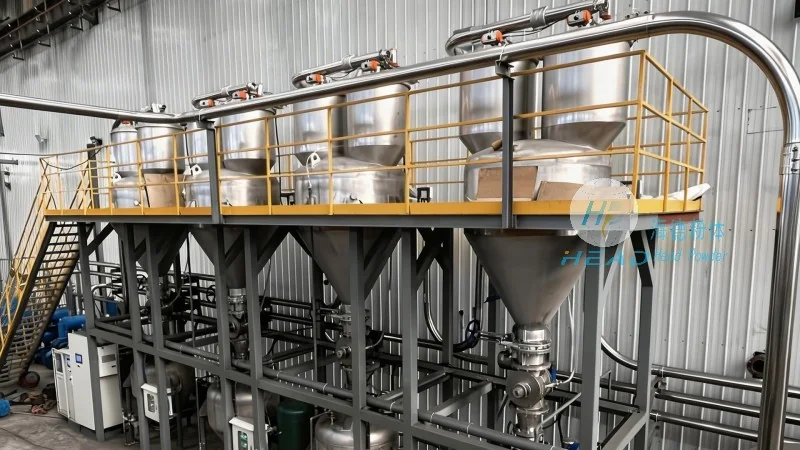
Technical Specifications and Customization Options
Shandong HeadPowder Engineering Co., Ltd. offers a range of technical specifications and customization options to meet the diverse needs of its clients. The conveying system can be configured to handle different particle sizes, from fine powders to coarse granules, with adjustable air flow rates and pressure levels. The pipeline network can be designed in various configurations, including straight, curved, or vertical sections, to accommodate the specific layout of a facility. The system can also be integrated with existing infrastructure, such as existing silos or storage tanks, to minimize installation costs and time. Customization options include the addition of automated control systems, remote monitoring capabilities, and specialized materials handling components tailored to the specific requirements of the fertilizer type. The company provides detailed technical documentation and engineering support to assist clients in selecting the most suitable system configuration for their applications.
Conclusion and Company Overview
In conclusion, the fertilizer granule conveying system, particularly with pneumatic conveying technology, represents a highly efficient and reliable solution for the transport of granular fertilizers. The system, manufactured by Shandong HeadPowder Engineering Co., Ltd., offers numerous advantages, including high throughput, low maintenance costs, and environmental compliance. By leveraging advanced engineering and high-quality materials, the system ensures consistent performance and durability, making it an ideal choice for agricultural and industrial applications. With its headquarters in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. continues to provide innovative bulk material handling solutions to clients worldwide, contributing to the advancement of the fertilizer industry and supporting sustainable agricultural practices.