

Introduction to Millet Conveying Systems and the Advantages of Millet Pneumatic Conveying
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of efficient millet conveying systems. The company's expertise lies in providing advanced solutions for the agricultural sector, particularly in the handling and transportation of millet, a staple grain widely used in various food products and industrial applications.
Understanding Millet Conveying Systems
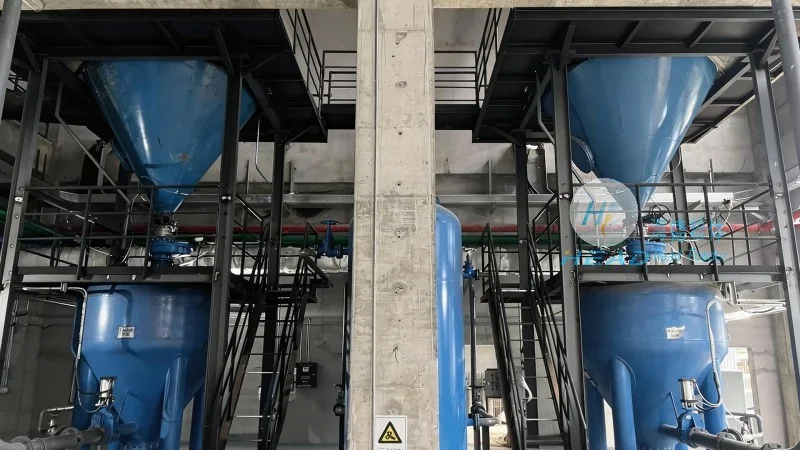
Millet conveying systems are engineered to facilitate the movement of millet from storage facilities to processing plants or distribution centers. These systems are crucial for optimizing workflow in agricultural operations, ensuring that millet is handled with minimal loss and maximum efficiency. The design of these systems considers factors such as grain moisture content, bulk density, and the need for gentle handling to preserve grain quality.
The Advantages of Pneumatic Conveying for Millet
Pneumatic conveying, or air-based transport, offers several key advantages over traditional mechanical conveying methods for millet. One of the primary benefits is the ability to transport millet over long distances with minimal infrastructure requirements. This method reduces the need for multiple transfer points and associated equipment, streamlining the overall process. Additionally, pneumatic conveying systems are highly effective in preventing contamination and maintaining grain purity, which is critical for both food safety and industrial use.
Efficiency and Cost-Effectiveness
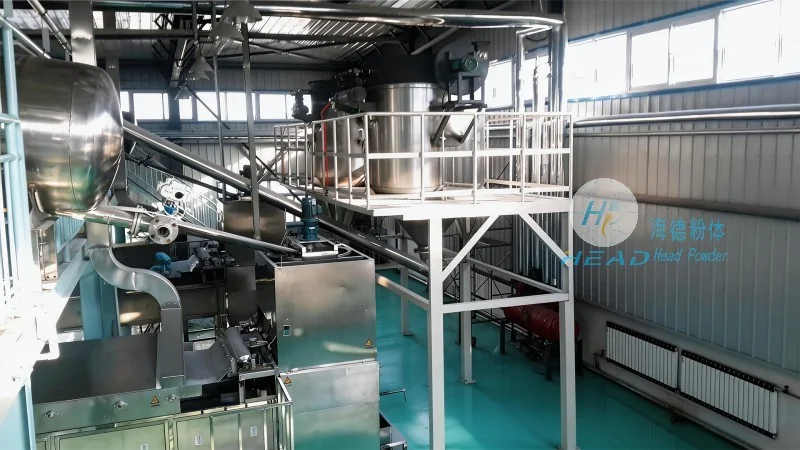
Implementing a pneumatic conveying system for millet can significantly enhance operational efficiency. By automating the transport process, companies can reduce labor costs and minimize downtime associated with manual handling. The system's ability to handle large volumes of millet at once further improves throughput, making it an ideal solution for high-production agricultural operations. Furthermore, the reduced need for physical handling equipment and maintenance of traditional systems leads to long-term cost savings.
Environmental and Safety Benefits
Modern millet conveying systems, especially those utilizing pneumatic technology, are designed with environmental and safety considerations in mind. Pneumatic conveying minimizes dust generation compared to mechanical systems, contributing to a cleaner working environment and reduced health risks for operators. The enclosed nature of the system also helps in controlling grain quality by preventing exposure to external elements, such as moisture or pests. This not only preserves the nutritional value of the millet but also extends its shelf life, making it more valuable for consumers and processors alike.
Customization and Scalability
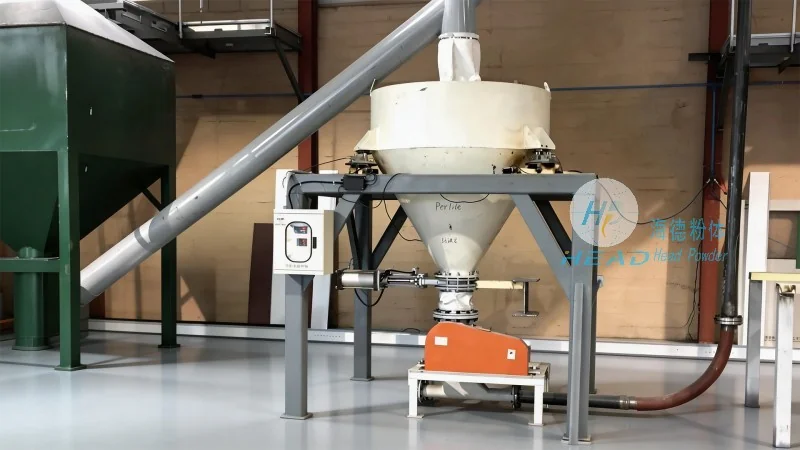
HeadPowder recognizes that each agricultural operation has unique requirements. Therefore, the company offers customized millet conveying solutions tailored to specific needs, including varying grain types, production volumes, and operational constraints. These systems can be scaled from small-scale farms to large industrial facilities, ensuring that the technology adapts to the growth and changing demands of the business. The modular design of the systems allows for easy expansion or modification as the operation evolves, providing a flexible and long-term investment.
Conclusion: Choosing the Right Millet Conveying Solution
For businesses in the millet industry, selecting an efficient and reliable conveying system is essential for maintaining productivity and product quality. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, provides comprehensive solutions that leverage the advantages of pneumatic technology. By investing in a well-designed millet conveying system, companies can enhance their operational efficiency, reduce costs, and ensure the safety and quality of their millet products. The expertise and commitment of HeadPowder make them a trusted partner in optimizing millet handling processes for the modern agricultural industry.