

Operation Process and Working Principle of Tonne Bag Discharge Powder Pneumatic Conveying Machine
For industrial applications requiring efficient and reliable powder handling, the tonne bag discharge powder pneumatic conveying machine has emerged as a critical solution. This equipment is designed to streamline the process of transferring bulk powders from storage bags to processing units, ensuring minimal waste and optimal performance. The following sections detail the operation process and working principles of this advanced system, highlighting its key components and operational dynamics.
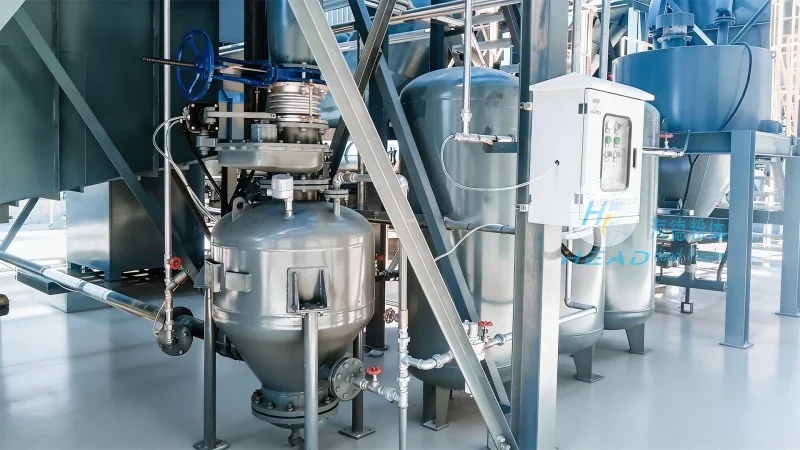
Introduction to Tonne Bag Discharge Powder Pneumatic Conveying Systems
The tonne bag discharge powder pneumatic conveying machine is a specialized piece of industrial equipment used to transfer bulk powders from large storage bags (typically 1 tonne capacity) into processing lines. This system is particularly valuable in industries such as food, pharmaceuticals, chemicals, and minerals, where maintaining product integrity and preventing contamination is paramount. The design of this equipment prioritizes efficiency, safety, and ease of maintenance, making it a preferred choice for businesses seeking to optimize their material handling operations.
Key Components and Their Roles
The tonne bag discharge powder pneumatic conveying machine comprises several essential components, each playing a vital role in the overall operation. These include the bag discharger, airlock, conveyor line, and dust collection system. The bag discharger is responsible for opening the tonne bag and releasing the powder into the system. The airlock acts as a valve to control the flow of material and prevent backflow. The conveyor line transports the powder through the system using air pressure, while the dust collection system ensures a clean and safe working environment by capturing any airborne particles.
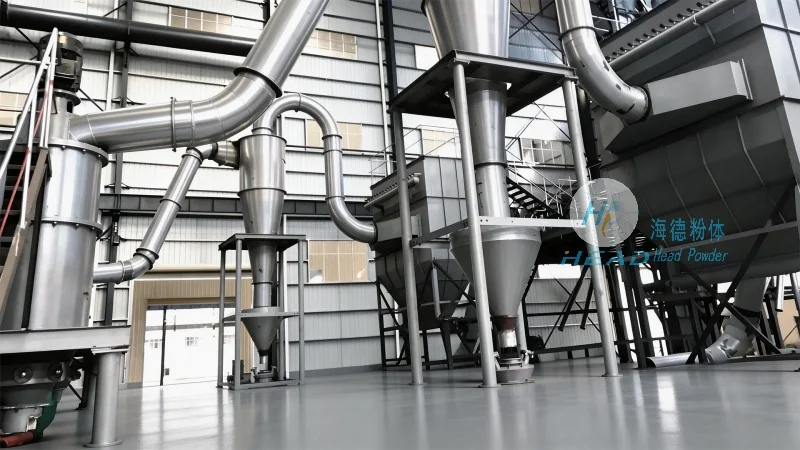
Operation Process: Step-by-Step Overview
The operation of the tonne bag discharge powder pneumatic conveying machine follows a systematic sequence to ensure efficient material transfer. The process begins with the placement of a filled tonne bag onto the bag discharger. The discharger then opens the bag, allowing the powder to fall into the hopper. From the hopper, the powder is fed into the airlock, which regulates the flow rate. Simultaneously, a vacuum or pressure system is activated to create airflow through the conveyor line. The air carries the powder particles along the pipeline to the processing unit. The airlock at the receiving end controls the discharge of the powder into the target container. Throughout this process, the system maintains consistent air pressure and flow rates to prevent clogging and ensure smooth operation.
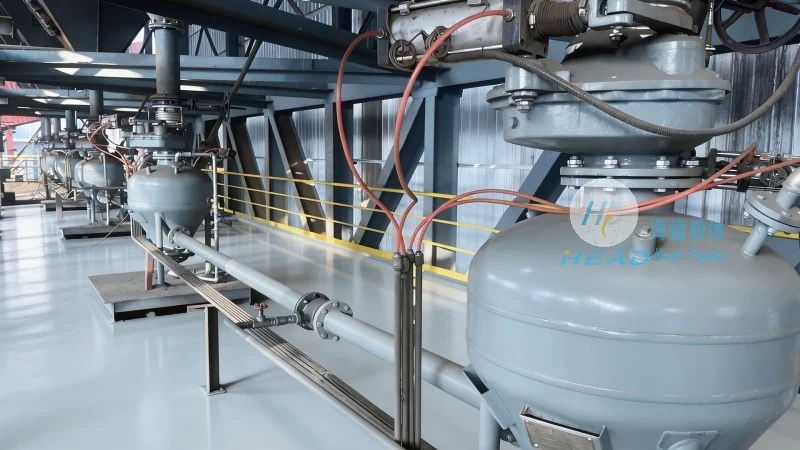
Working Principle: How the System Transfers Powders
The core working principle of the tonne bag discharge powder pneumatic conveying machine is based on pneumatic conveying technology, which utilizes air to transport bulk materials. The system operates by creating a pressure differential between the inlet and outlet of the conveyor line. In a vacuum system, air is drawn into the line, creating a negative pressure that pulls the powder particles along with it. In a pressure system, compressed air is forced through the line, pushing the powder forward. The tonne bag discharge mechanism ensures that the powder is released from the bag into the system without manual intervention, enhancing automation and reducing labor costs. The airlock components are crucial for maintaining the flow rate and preventing the backflow of powder or air, which could lead to system inefficiencies or product contamination.
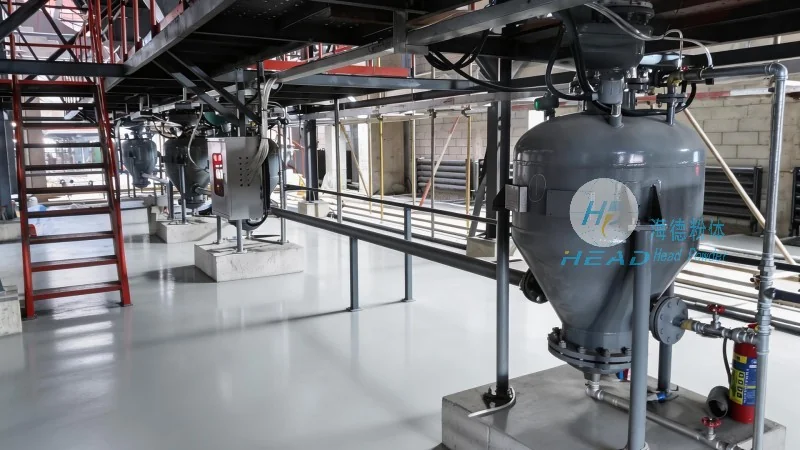
Advantages and Applications
The tonne bag discharge powder pneumatic conveying machine offers several advantages that make it suitable for a wide range of industrial applications. These include high transfer efficiency, minimal product degradation, and reduced labor requirements. The system is particularly effective for handling fine or abrasive powders, as it minimizes friction and impact during transfer. Additionally, the enclosed design of the equipment helps maintain product purity and prevents cross-contamination, which is critical in industries such as pharmaceuticals and food processing. The system is also versatile, capable of handling various powder types and transfer distances, making it a flexible solution for different production needs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder handling equipment, specializes in developing and supplying advanced pneumatic conveying systems. With a focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's expertise lies in designing customized systems that meet the specific requirements of each client, ensuring optimal performance and long-term durability. The company's products are manufactured with high-quality materials and undergo rigorous testing to ensure compliance with industry standards. HeadPowder's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering superior products and services in the industry.