

Principle and Working Scene Characteristics of Powder Conveying Lines in Grain Warehouses
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, specializes in the design and manufacturing of advanced powder conveying systems tailored for grain warehouse applications. Our focus is on delivering efficient, reliable solutions that enhance material handling processes in agricultural storage facilities. This article explores the fundamental principles behind these systems and highlights key operational characteristics relevant to real-world grain handling scenarios.
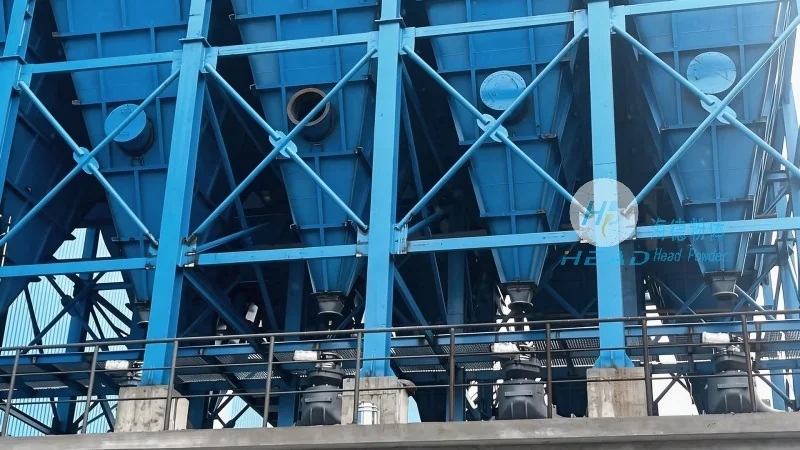
Core Principles of Powder Conveying Lines in Grain Warehouses
The operation of powder conveying lines in grain warehouses is based on a combination of mechanical and pneumatic engineering principles. These systems are engineered to transport bulk materials such as grains, flour, and other agricultural products from storage silos to processing or packaging areas. The primary objectives include maintaining consistent flow rates, minimizing material degradation, and ensuring energy efficiency. Our systems incorporate advanced components like aeration devices, vibration mechanisms, and variable speed drives to address the unique challenges of grain handling, including preventing caking, bridging, or blockages that can disrupt operations.
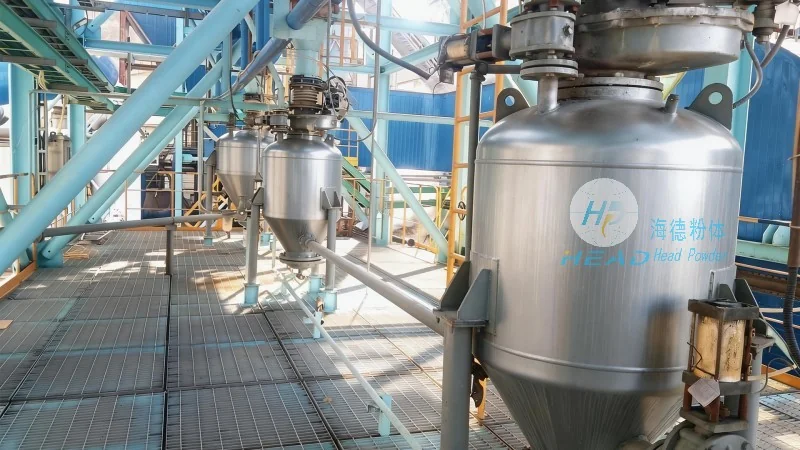
Key Operational Characteristics and Working Scenarios
The effectiveness of powder conveying lines in grain warehouses is determined by several critical operational characteristics. These include the type of material being handled, the distance and elevation changes required for transport, and the need for integration with existing storage infrastructure. In typical grain handling facilities, these systems must operate under varying environmental conditions, such as fluctuating temperatures and humidity levels, while maintaining stable performance. The design of our conveying lines prioritizes adaptability, allowing seamless integration with different warehouse layouts and processing workflows. Additionally, our solutions emphasize safety and compliance with industry standards, ensuring that operations meet regulatory requirements for food and agricultural material handling.
Application-Specific Features for Optimal Performance
When applied in grain warehouse environments, our powder conveying lines exhibit distinct features that enhance their performance. For example, the use of aeration and vibration helps maintain material flow in silos, preventing issues like caking or bridging. Our systems also include monitoring and control technologies that provide real-time feedback on system performance, enabling operators to adjust settings dynamically based on material conditions or processing demands. This adaptability is crucial in grain handling, where material properties can vary significantly due to seasonal changes or different crop types. Furthermore, the modular design of our conveying lines allows for easy expansion or reconfiguration as warehouse needs evolve, providing long-term value and flexibility to our clients.
Company Background and Commitment to Excellence
HeadPowder, headquartered in Shandong, China, is a leading manufacturer of specialized powder conveying equipment for the grain industry. Our company has built a reputation for delivering high-quality, reliable systems that meet the rigorous demands of modern agricultural operations. By focusing on the core principles of efficient material handling and adapting to the unique characteristics of grain warehouses, we provide solutions that enhance productivity and operational efficiency. Our team of engineers and technicians leverages years of experience and advanced manufacturing capabilities to develop systems that are both effective and sustainable. With a commitment to customer satisfaction and continuous innovation, headpowder remains a trusted partner for grain storage and processing facilities worldwide.