

Principles and Application Scenarios of Hybrid Pneumatic Conveying Equipment
Hybrid pneumatic conveying equipment represents a sophisticated solution in material handling, combining the advantages of different conveying technologies to achieve efficient and flexible material transport. This equipment is designed to handle a wide range of bulk materials, from powders and granules to fine particles, with precision and reliability. The core principle involves using a combination of pressure and vacuum systems to move materials through a pipeline network, ensuring minimal product degradation and optimal process control.
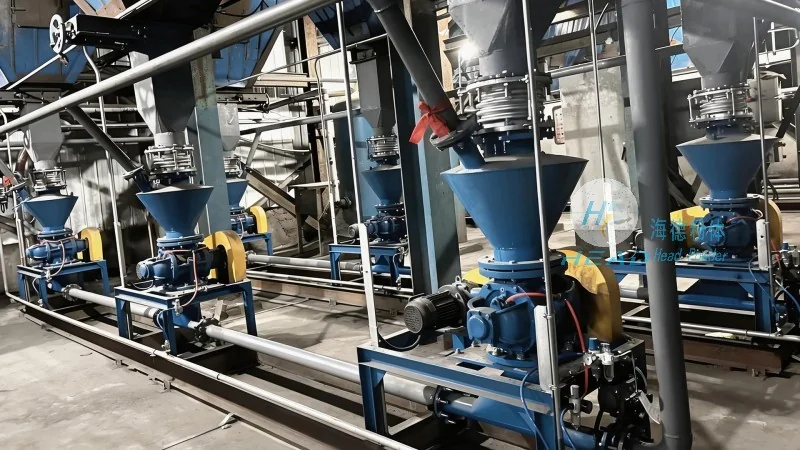
Principles of Operation
The fundamental operation of hybrid pneumatic conveying systems is based on the integration of positive and negative pressure stages. In the positive pressure mode, compressed air is used to push material through the pipeline, while the negative pressure mode utilizes vacuum to draw material into the system. This dual-mode approach allows for flexible operation, adapting to varying material characteristics and process requirements. The system typically includes components such as feeders, cyclones, filters, and control valves, all working in concert to maintain consistent material flow and prevent blockages. The design emphasizes energy efficiency and low maintenance, making it suitable for continuous industrial applications.
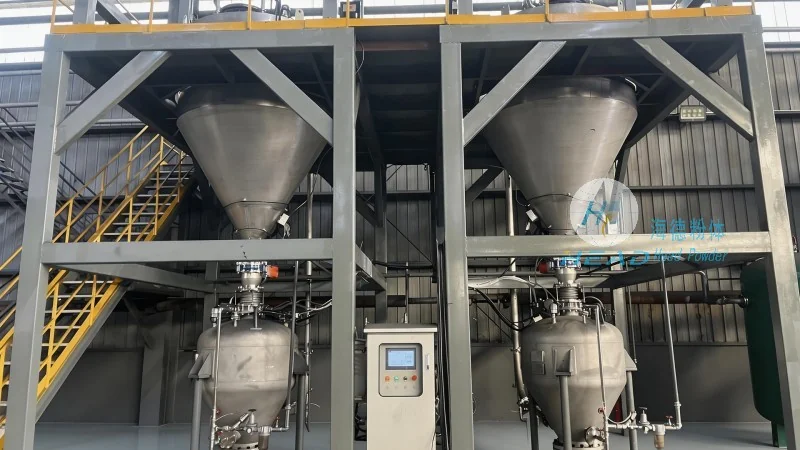
Key Features and Advantages
Hybrid pneumatic conveying equipment offers several key advantages that make it a preferred choice in modern industrial settings. Firstly, it provides high material transport efficiency, capable of moving materials over long distances with minimal loss. Secondly, the system is highly flexible, allowing for changes in material type or process flow without significant modifications. Additionally, it reduces product contamination and degradation, which is crucial for sensitive materials like pharmaceuticals or food products. The equipment also features advanced control systems that enable real-time monitoring and adjustment, ensuring optimal performance and safety. With its ability to handle diverse materials and operating conditions, hybrid pneumatic conveying equipment is a versatile solution for various industrial applications.
Application Scenarios and Use Cases
Hybrid pneumatic conveying equipment is widely used in several industrial sectors, each with specific requirements that the system addresses effectively. In the pharmaceutical industry, for example, it is employed to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring strict contamination control and product integrity. The food processing industry utilizes it for handling powders like flour, sugar, and spices, maintaining hygiene standards and preventing cross-contamination. In the chemical industry, the equipment is used to convey raw materials and finished products, supporting processes that demand high precision and safety. Additionally, in the agricultural sector, it aids in the transport of grain and other agricultural products, improving efficiency in storage and processing facilities. The versatility of hybrid pneumatic conveying systems makes them suitable for a broad range of applications, from small-scale operations to large-scale industrial plants.
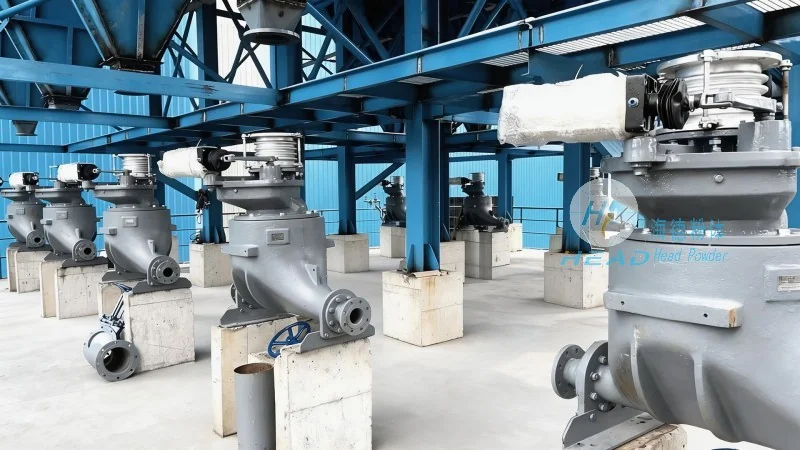
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions. With a strong commitment to innovation and quality, the company specializes in the design, development, and production of hybrid pneumatic conveying equipment. HeadPowder leverages years of industry experience to deliver customized solutions that meet the unique needs of its clients. The company's products are engineered to enhance operational efficiency, reduce costs, and improve product quality, aligning with the evolving demands of modern industries. HeadPowder's headquarters is located in Shandong, China, where the company maintains state-of-the-art manufacturing facilities and a dedicated research and development team. The company's focus on customer satisfaction and technological advancement has established it as a trusted partner in the material handling sector.