

Working Principle and Features of Quartz Powder Material Handling System Equipment
The working principle of quartz powder material handling system equipment revolves around the efficient transport of fine quartz particles from a storage area to a processing or packaging point. The process typically starts with the quartz powder being stored in a hopper or silo, where it is held under controlled conditions to prevent caking or moisture absorption. From the storage vessel, the material is fed into a conveyor system, which may include screw conveyors, belt conveyors, or pneumatic conveying lines. Screw conveyors utilize a rotating helical screw to push the powder forward through a tube, maintaining a consistent flow rate. Belt conveyors, on the other hand, use a moving belt to transport the powder over a series of rollers, suitable for longer distances and higher volumes. Pneumatic conveying systems employ compressed air to create a pressure differential, propelling the powder through a pipeline. This method is particularly effective for fine powders like quartz, as it minimizes dust and ensures a smooth transfer. The system also includes control mechanisms such as flow meters and pressure sensors to monitor and regulate the material flow, ensuring optimal performance and preventing issues like blockages or overloading. Additionally, the equipment may incorporate dust collection systems to capture any airborne particles, maintaining a clean and safe working environment.
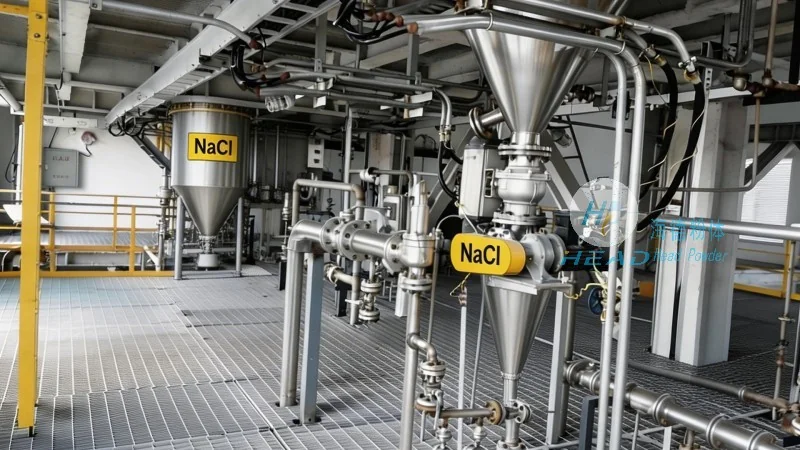
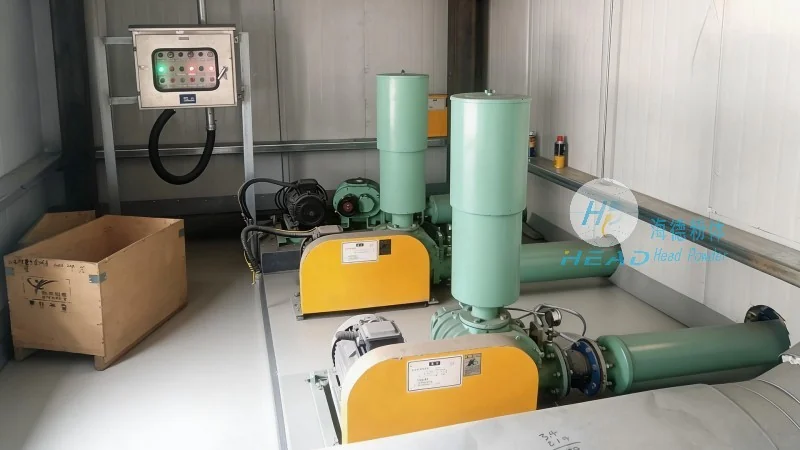
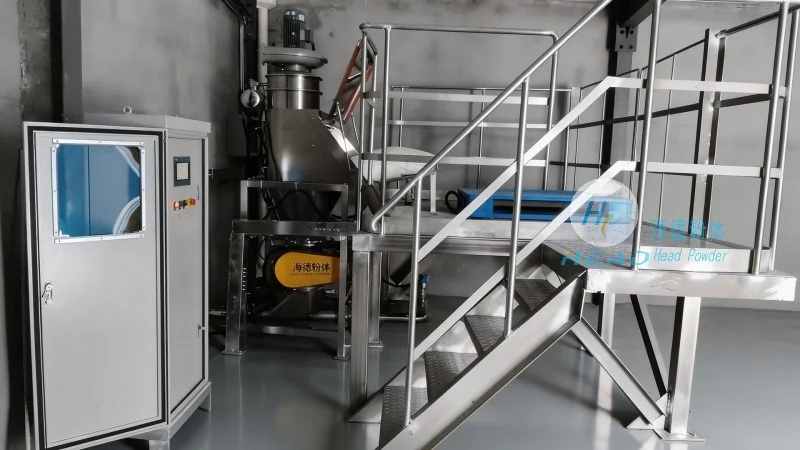
Key Features of Quartz Powder Material Handling System Equipment from Shandong HeadPowder Engineering Co., Ltd.
The quartz powder material handling system equipment from Shandong HeadPowder Engineering Co., Ltd. is engineered with several key features that enhance its functionality and reliability. One of the primary features is its high efficiency in handling fine powders, which is critical for maintaining product quality and preventing contamination. The equipment is constructed using durable materials, such as stainless steel or corrosion-resistant alloys, to withstand the abrasive nature of quartz powder and ensure long-term durability. Another important feature is the system's ability to minimize dust and airborne particles, achieved through sealed components and advanced filtration systems. This not only improves workplace safety but also maintains the purity of the quartz powder. The system offers flexibility in customization, allowing it to be adapted to different production scales and operational environments. Advanced control systems are integrated to enable precise monitoring and adjustment of the material flow, ensuring consistent output and reducing operational errors. The design prioritizes user safety with features like emergency stop buttons and protective enclosures, making it suitable for industrial settings where safety is a top priority. Furthermore, the equipment is designed for low maintenance, with easy access to components for cleaning and repair, reducing downtime and operational costs.
Operational Advantages and Application Scenarios
Quartz powder material handling systems offer significant operational advantages in various industries, including ceramics, glass manufacturing, and chemical processing. The equipment from Shandong HeadPowder Engineering Co., Ltd. provides high volume handling capabilities, reducing production downtime and increasing overall productivity. The system's low maintenance requirements and long service life contribute to cost savings over time. It also minimizes material loss and waste, which is crucial for maintaining profitability and environmental compliance. The sealed and enclosed design helps control dust emissions, aligning with environmental regulations. The adaptability of the system allows it to integrate seamlessly with existing production lines, reducing the need for extensive modifications or new installations. This makes it an ideal solution for both new and existing facilities. The reliability and performance of the equipment ensure consistent quality output, vital for meeting customer specifications and maintaining brand reputation. In addition, the system's energy efficiency, through optimized conveyor speeds and reduced air pressure in pneumatic systems, lowers operational costs. The combination of these features makes the quartz powder material handling system a reliable and efficient solution for businesses in need of consistent and safe powder transport.