

Working Principle and Features of White Carbon Black Powder Pneumatic Conveying System Equipment
White carbon black, also known as silica, is a crucial industrial material widely used in various sectors including rubber, plastics, coatings, and cosmetics. The efficient and reliable transport of white carbon black powder from storage to processing units is essential for maintaining production efficiency and product quality. Pneumatic conveying systems have emerged as a preferred solution for handling white carbon black powder due to their ability to transport powders in a dust-free, controlled manner. This article explores the working principle and key features of white carbon black powder pneumatic conveying systems, highlighting their operational efficiency and technical advantages.
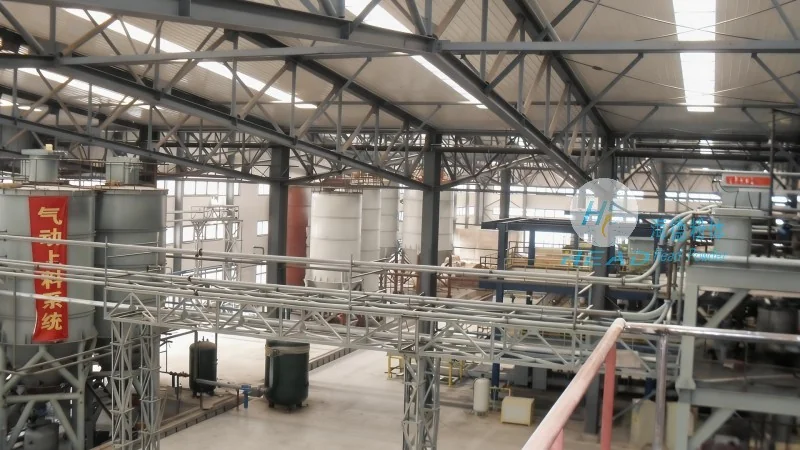
Working Principle of Pneumatic Conveying Systems for White Carbon Black Powder
The core of a white carbon black powder pneumatic conveying system lies in its ability to use air as the conveying medium. The system typically consists of several key components, including a hopper, a feeder, a conveying line, and a receiver. The process begins with the white carbon black powder being fed from the storage hopper into the feeder. The feeder then controls the flow rate of the powder, ensuring a consistent and controlled discharge. Simultaneously, a fan or blower generates a high-pressure air stream that is introduced into the conveying line. The air stream, moving at a sufficient velocity, lifts and transports the white carbon black powder particles through the pipeline. The powder is carried by the air flow, and upon reaching the receiver, the air is separated from the powder, often using a cyclone separator or a filter. The separated powder is then collected in the receiver, while the air is either recirculated or discharged. This continuous cycle allows for the seamless transport of white carbon black powder from the source to the destination, minimizing material loss and contamination.
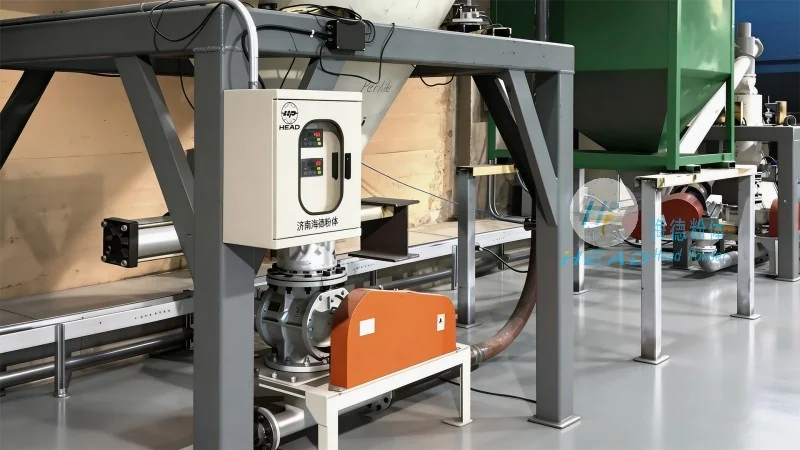
Key Features and Advantages of White Carbon Black Powder Pneumatic Conveying Systems
White carbon black powder pneumatic conveying systems offer several distinct features and advantages that make them ideal for industrial applications. Firstly, they provide a dust-free and enclosed transport environment, which is critical for maintaining product purity and preventing environmental contamination. Unlike traditional belt or bucket elevators, pneumatic systems do not generate dust during operation, ensuring a cleaner working environment. Secondly, these systems offer high flexibility in terms of layout and installation. The conveying lines can be easily adjusted or reconfigured to accommodate changes in production processes or facility layouts. Thirdly, pneumatic conveying systems are capable of handling a wide range of powder characteristics, including different particle sizes, densities, and flow properties of white carbon black powder. This adaptability makes them suitable for various applications, from small-scale laboratory use to large-scale industrial production. Additionally, the systems are relatively low in maintenance compared to other bulk material handling equipment, as they have fewer moving parts and less wear and tear. The use of air as the conveying medium also reduces the risk of material degradation, which is particularly important for sensitive materials like white carbon black. Furthermore, the enclosed nature of the system helps in controlling the temperature and humidity of the powder during transport, preserving its quality and preventing caking or agglomeration.
Operational Efficiency and Performance Metrics
The efficiency of a white carbon black powder pneumatic conveying system is evaluated based on several performance metrics. The most critical metric is the conveying capacity, which refers to the amount of powder that can be transported per unit time. This capacity is influenced by factors such as the air velocity, the diameter of the conveying line, and the properties of the white carbon black powder. For example, higher air velocities can increase the conveying capacity but may also lead to higher energy consumption. The system's pressure drop is another important metric, as it indicates the energy required to move the powder through the pipeline. A lower pressure drop means lower energy consumption and reduced operating costs. The system's reliability and uptime are also crucial, as any downtime can significantly impact production schedules and profitability. Modern pneumatic conveying systems are designed with advanced controls and monitoring systems that allow for real-time performance tracking and maintenance alerts, enhancing overall operational efficiency. Additionally, the system's ability to handle varying flow rates without significant performance degradation is a key advantage, ensuring consistent operation under different production conditions.
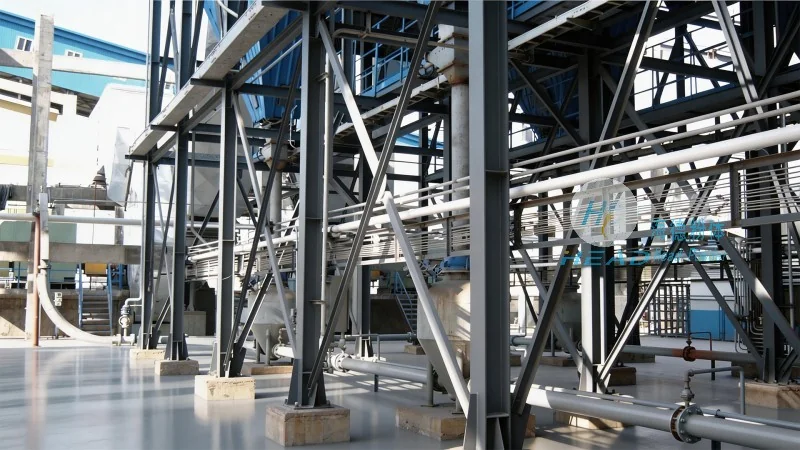
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of advanced pneumatic conveying systems for white carbon black powder and other industrial powders. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the bulk material handling industry. HeadPowder specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of its clients. The company's product portfolio includes a range of systems from small-scale laboratory units to large-scale industrial installations, ensuring that it can meet the diverse requirements of various industries. HeadPowder's engineering team leverages advanced technology and extensive industry experience to develop efficient and reliable pneumatic conveying systems that enhance production efficiency and product quality. The company adheres to strict quality control standards and provides comprehensive after-sales support, including installation, commissioning, and maintenance services. HeadPowder's facilities are located in Shandong, China, where it operates a state-of-the-art manufacturing plant equipped with the latest production equipment and technology. The company's focus on customer satisfaction and technical excellence has enabled it to build a strong reputation in the market, serving clients globally with high-quality pneumatic conveying systems.