

Working Principle and Features of the Rice Husk Ash Pneumatic Conveying System Equipment
When it comes to efficient material handling in industrial settings, especially for bulk materials like rice husk ash, the choice of equipment can significantly impact operational efficiency and cost-effectiveness. The pneumatic conveying system designed for rice husk ash processing represents a sophisticated solution that combines advanced engineering with practical application. This article delves into the working principle and key features of such equipment, highlighting how it addresses the unique challenges of handling this specific material.
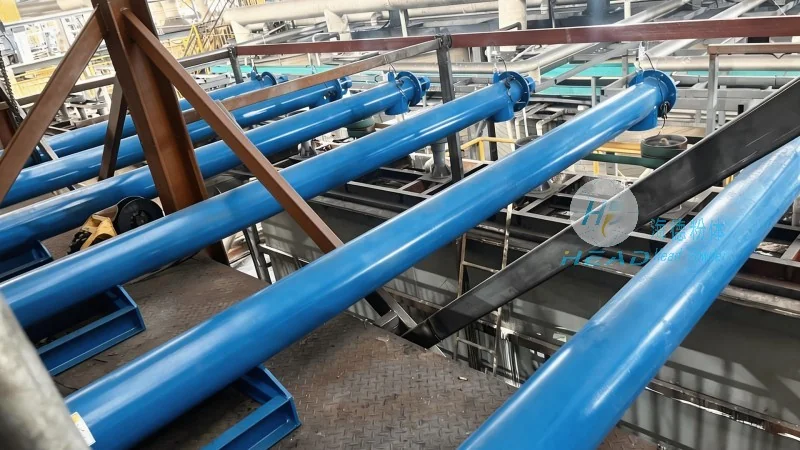
Understanding the Working Principle of the Rice Husk Ash Pneumatic Conveying System
The core of the rice husk ash pneumatic conveying system lies in its ability to transport bulk materials through a pressurized or vacuum environment using air or other gases. The system typically operates on one of two principles: positive pressure or negative pressure. In positive pressure systems, air is forced through the material, creating a flow that moves the ash from the source to the destination. Conversely, negative pressure systems draw air and material through a vacuum, pulling the rice husk ash into the conveying line. Both methods are engineered to maintain consistent flow rates and prevent material degradation or blockages.
Key components of the system include the conveying line, which is usually made of durable materials like stainless steel or high-density polyethylene to withstand the abrasive nature of rice husk ash. The feeders are critical for controlling the material flow rate, ensuring a steady supply to the system. The air compressor or vacuum pump provides the necessary pressure or suction to move the material through the line. Additionally, filters and cyclones are integrated to separate the material from the air, preventing dust accumulation and maintaining air quality. The entire system is designed to be modular, allowing for easy expansion or integration with existing industrial setups.
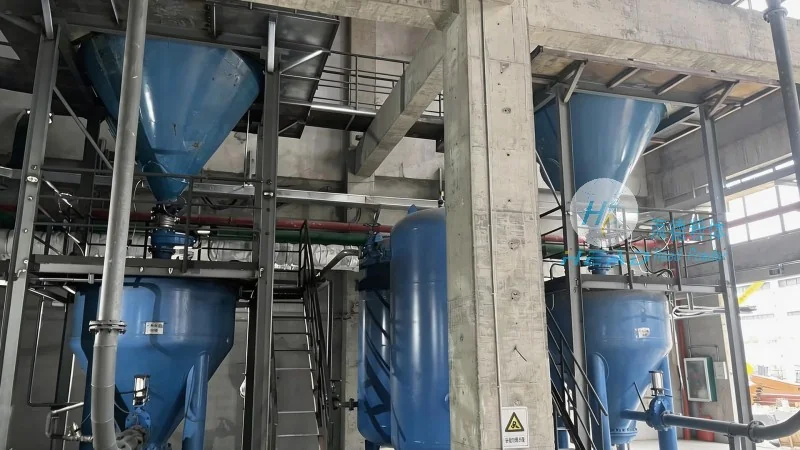
Key Features and Advantages of the Rice Husk Ash Pneumatic Conveying System
One of the primary advantages of this system is its versatility in handling various particle sizes and moisture content of rice husk ash. The adjustable air flow and pressure settings enable operators to optimize the conveying process for different material characteristics, ensuring minimal loss and maximum efficiency. Another notable feature is the hygienic design, which is essential for industries where material purity is critical, such as food processing or pharmaceuticals. The system’s components are easy to clean and maintain, reducing downtime and maintenance costs.
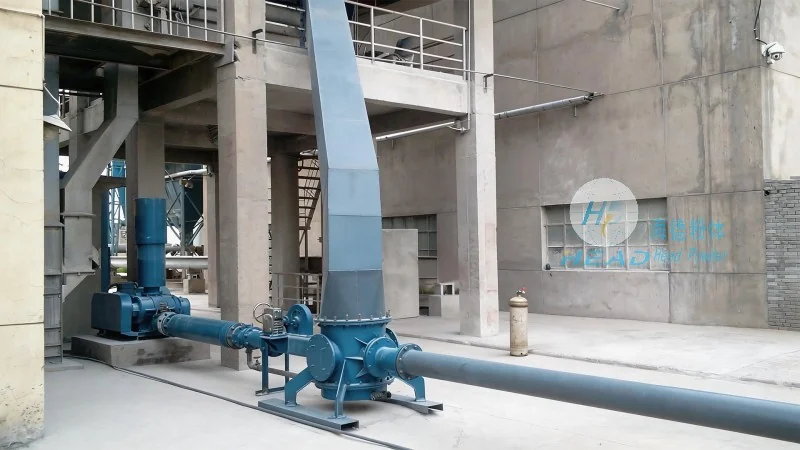
The system also offers energy efficiency through optimized air usage and reduced material handling time. By eliminating the need for mechanical components like belts or buckets, the pneumatic system minimizes wear and tear, leading to lower operational costs over time. Furthermore, the compact design of the equipment allows for installation in limited spaces, making it suitable for both new and retrofit applications. The system’s ability to handle long-distance conveying without intermediate storage points also streamlines the material flow, enhancing overall production throughput.
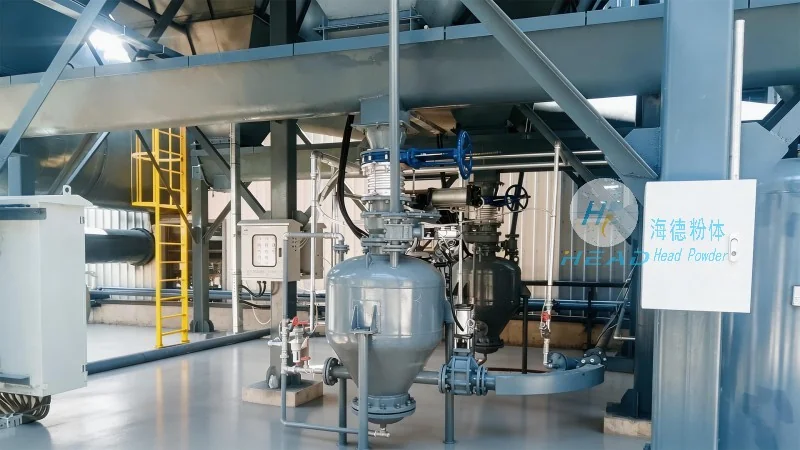
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field of industrial material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and supplying high-quality pneumatic conveying systems tailored to the needs of various industries. With a focus on innovation and customer satisfaction, the company has built a reputation for delivering reliable and efficient equipment that meets international standards. HeadPowder’s expertise lies in understanding the unique challenges of handling bulk materials like rice husk ash, and their engineers work closely with clients to develop customized solutions that enhance operational performance.
HeadPowder’s facilities are located in Shandong, China, where the company leverages advanced manufacturing technologies and a skilled workforce to produce top-tier equipment. The company adheres to strict quality control measures, ensuring that each product meets the highest standards of durability and performance. Clients benefit from HeadPowder’s comprehensive support, including installation, maintenance, and technical assistance, which ensures the long-term reliability of the pneumatic conveying systems.