

Working Principle and Features of Potassium Carbonate Fertilizer Pneumatic Conveying System Equipmen
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the fertilizer industry. This article delves into the working principle and key features of the potassium carbonate fertilizer pneumatic conveying system equipment, providing a comprehensive overview for industry professionals and potential clients.
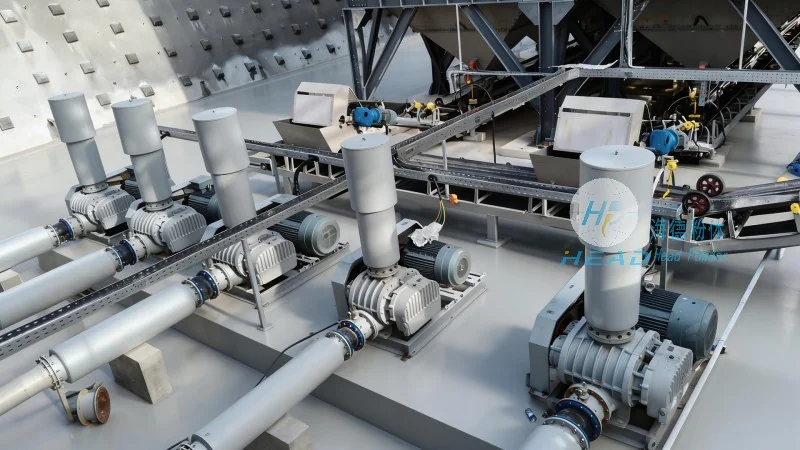
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder is headquartered in Shandong, China, and has established itself as a trusted provider of customized engineering solutions for bulk material handling. With a focus on innovation and quality, the company serves clients across various sectors, including agriculture, chemical processing, and food production. The expertise of HeadPowder lies in developing efficient and reliable systems that meet the specific demands of modern industrial applications.
Working Principle of Potassium Carbonate Fertilizer Pneumatic Conveying System
The potassium carbonate fertilizer pneumatic conveying system operates on the principle of air-driven material transport. At its core, the system utilizes a combination of positive and negative pressure to move bulk materials through a network of pipes. The process begins with the material being fed into a hopper or silo, where it is then drawn into a conveyor line by a vacuum or pressure source. The system typically includes components such as a rotary valve, a filter, and a blower or vacuum pump. The material is carried by the air stream, which is controlled to maintain optimal flow rates and prevent clogging. The conveying process is continuous, ensuring a steady supply of fertilizer to downstream processing or storage facilities. The system is designed to handle the specific characteristics of potassium carbonate, such as its granular or powder form, ensuring efficient and safe transport without degradation of the product.
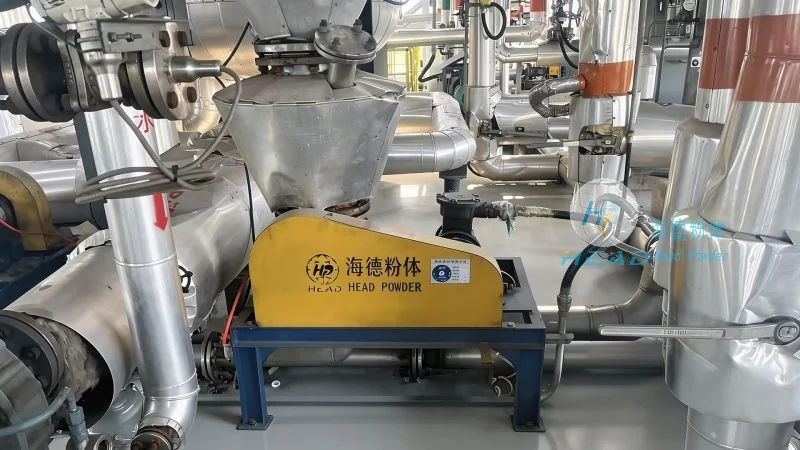
Key Features of the Pneumatic Conveying System
The potassium carbonate fertilizer pneumatic conveying system from HeadPowder is equipped with several advanced features that enhance its performance and reliability. One of the primary features is the use of a closed-loop system, which minimizes dust emissions and ensures environmental compliance. The system incorporates high-efficiency filters that capture fine particles, protecting both the equipment and the environment. Another key feature is the adjustable air flow control, which allows operators to optimize the conveying rate based on the material's properties and system requirements. The system also includes safety mechanisms, such as pressure relief valves and overload protection, to prevent accidents and equipment damage. Additionally, the design incorporates corrosion-resistant materials, suitable for the chemical properties of potassium carbonate, ensuring long-term durability and minimal maintenance. The system's modular construction enables easy integration with existing facilities and facilitates future expansion or upgrades.
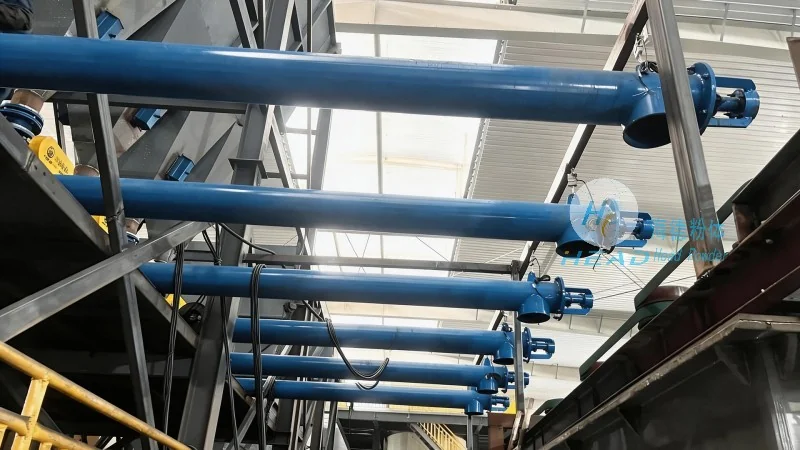
Advantages of Using a Pneumatic Conveying System for Potassium Carbonate Fertilizer
Implementing a pneumatic conveying system for potassium carbonate fertilizer offers numerous advantages over traditional methods like belt conveyors or manual handling. The most significant benefit is the reduction in labor costs and operational time, as the system automates the material transport process. This leads to increased productivity and efficiency in fertilizer production and distribution. The system also minimizes product loss and contamination, as the closed-loop design prevents exposure to external elements and reduces the risk of spillage. Furthermore, the system's ability to handle both dry and slightly moist materials makes it versatile for various fertilizer formulations. The energy efficiency of the pneumatic system, particularly when using vacuum technology, reduces operational costs compared to positive pressure systems. The system's compact design allows for installation in limited spaces, making it suitable for existing industrial sites without major modifications. Overall, the pneumatic conveying system provides a reliable, cost-effective, and environmentally friendly solution for transporting potassium carbonate fertilizer.
Customization and Application Considerations
HeadPowder understands that each fertilizer facility has unique requirements, and therefore, the pneumatic conveying system is customizable to meet specific needs. The system can be tailored in terms of capacity, conveying distance, and material handling capabilities. For instance, the system can be designed to handle large volumes of potassium carbonate, suitable for bulk production facilities, or scaled down for smaller operations. The system's components, such as the blower size and filter capacity, can be adjusted based on the material's density and flow characteristics. Additionally, the system can be integrated with other processing equipment, such as mixers or packaging machines, to create a fully automated production line. When selecting a pneumatic conveying system, factors such as the fertilizer's moisture content, particle size distribution, and the required conveying distance should be considered to ensure optimal performance. HeadPowder's engineering team provides comprehensive consultation to help clients choose the most suitable system configuration and ensure seamless integration with their existing infrastructure.