

Working Principle and Features of Grain Pneumatic Conveying Systems
Grain pneumatic conveying systems are essential equipment in the agricultural and food processing industries, designed to transport bulk materials like grains, powders, and other granular substances efficiently and safely. These systems utilize air pressure to move materials through a pipeline, offering a flexible and effective solution for material handling in various applications.
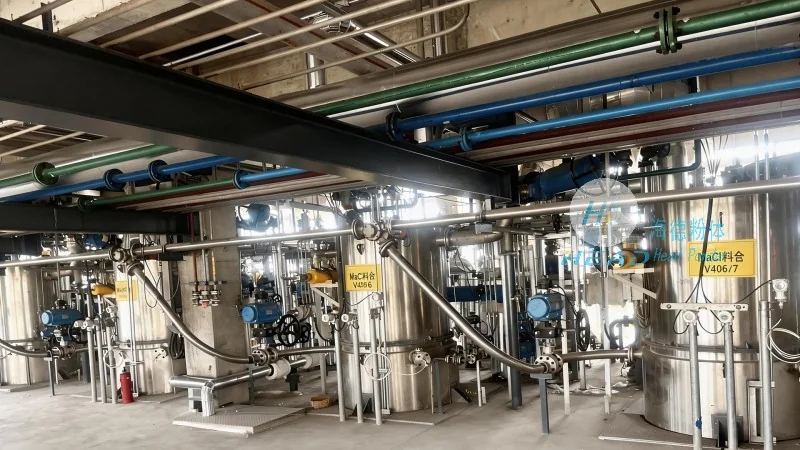
Working Principle of Grain Pneumatic Conveying Systems
The core mechanism of a grain pneumatic conveying system involves the use of compressed air to create a flow that propels the material through a sealed pipeline. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure. In positive pressure systems, air is forced into the pipeline, pushing the material along with it. Conversely, negative pressure systems draw air and material from the source into a vacuum, pulling the material through the system. The choice between these systems depends on factors such as the material's properties, the distance to be transported, and the desired level of dust control. The system typically includes components like a hopper for material storage, a feeder to control the flow rate, a conveyor line with appropriate ductwork, and a receiver or silo for the discharged material. The air flow is regulated by valves and fans to maintain optimal pressure and ensure smooth material transport. This mechanism allows for the continuous and automated movement of bulk materials, reducing manual labor and enhancing operational efficiency.
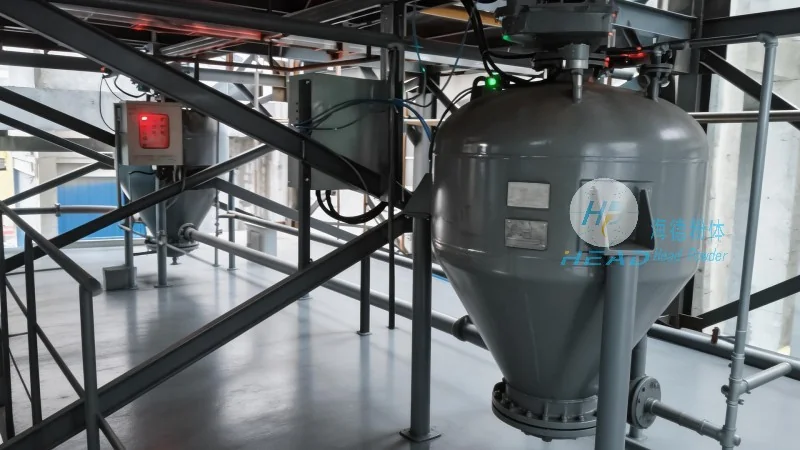
Key Features and Advantages of Grain Pneumatic Conveying Systems
Grain pneumatic conveying systems offer several distinct advantages that make them a preferred choice for many industries. One of the most significant benefits is the ability to transport materials without direct contact, which minimizes contamination and reduces the risk of product degradation. This is particularly important for food-grade grains and other sensitive materials, where hygiene and purity are critical. Additionally, these systems are highly flexible, as they can be easily integrated into existing production lines and adapted to different material types and processing requirements. The sealed pipeline design effectively controls dust emissions, improving workplace safety and compliance with environmental regulations. Another advantage is the ability to handle a wide range of materials, from fine powders to large granules, without the need for additional equipment like buckets or belts. This versatility makes the system suitable for various applications, including storage, processing, and distribution of grains. Furthermore, pneumatic conveying systems are generally more energy-efficient compared to traditional methods like bucket elevators or belt conveyors, as they use air pressure to move materials over longer distances with less mechanical wear. The compact design of the system also saves space in facilities, making it ideal for both large-scale and small-scale operations. Overall, the combination of efficiency, flexibility, and safety makes grain pneumatic conveying systems a reliable and cost-effective solution for bulk material handling.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying equipment, specializing in the design and production of grain pneumatic conveying systems. With years of experience in the industry, the company has developed a reputation for delivering high-quality, reliable, and efficient solutions tailored to the specific needs of its clients. HeadPowder's commitment to innovation and quality ensures that their products meet the highest standards of performance and durability. The company's facilities are equipped with advanced technology and skilled personnel, enabling them to provide customized solutions that enhance operational efficiency and reduce costs for their customers. HeadPowder's products are widely used in the agricultural, food processing, and chemical industries, contributing to the smooth and safe handling of bulk materials. The company's dedication to customer satisfaction and technical excellence has established it as a trusted partner in the field of material handling equipment.