

What is a Tonne Bag Unloading Station Pneumatic Conveying System? And What Are Its Design Principles
For industrial facilities dealing with bulk material handling, the tonne bag unloading station with a pneumatic conveying system represents a critical component in ensuring efficient material transfer. This system is specifically designed to handle large quantities of bulk materials from tonne bags, converting them into a transportable form through air-based technology. Understanding both the system's function and its underlying design principles is essential for optimizing material handling processes in various industrial applications.

Overview of Tonne Bag Unloading Station Pneumatic Conveying Systems
A tonne bag unloading station is a specialized facility used to receive and process bulk materials that are packaged in large, heavy-duty bags, typically with a capacity of one tonne or more. The primary function of this station is to safely and efficiently unload the contents of these bags and transfer the material to a storage silo, processing equipment, or other downstream units. The pneumatic conveying system integrated into this station uses air pressure to move the material from the bag to the desired destination, eliminating the need for manual handling and reducing the risk of dust exposure and material loss.
Key Components of the System
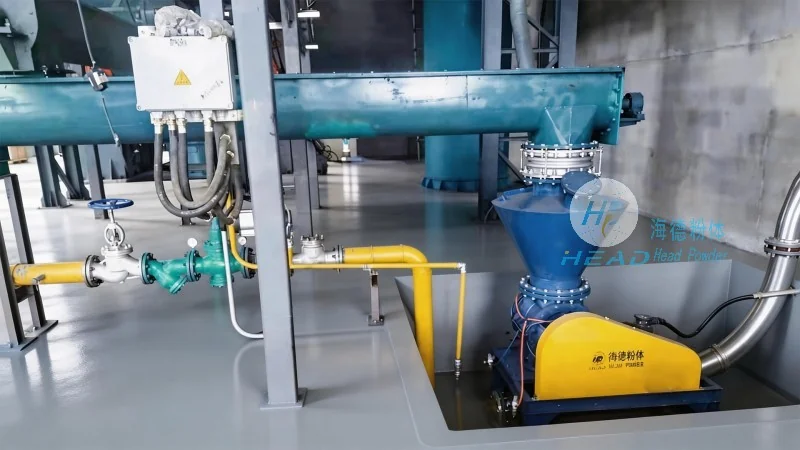
The tonne bag unloading station pneumatic conveying system consists of several key components that work in concert to achieve the material transfer. These components include the bag opening mechanism, the material feeder, the airlock or rotary valve, the conveying pipeline, and the receiver or silo. The bag opening mechanism is responsible for safely opening the tonne bag without damaging the material inside. The material feeder then draws the material from the bag and feeds it into the conveying system. The airlock or rotary valve acts as a gate to control the flow of material into the pipeline, preventing backflow and maintaining a consistent flow rate. The conveying pipeline transports the material through the system using air pressure, and the receiver or silo stores the material until it is ready for processing.
Design Principles and Operational Mechanisms
The design of a tonne bag unloading station pneumatic conveying system is based on several fundamental principles to ensure optimal performance and reliability. One of the core design principles is the use of positive pressure or negative pressure (or a combination of both) to move the material through the pipeline. Positive pressure systems use compressed air to push the material forward, while negative pressure systems use vacuum to pull the material. The choice between these systems depends on factors such as the material's properties, the distance to be conveyed, and the desired flow rate. Another important design principle is the selection of appropriate equipment based on the material's characteristics, including its density, moisture content, and flowability. For example, cohesive or sticky materials may require special feeding mechanisms or air-assisted feeding to ensure smooth transfer. The system's design also considers the need for dust control and environmental safety, incorporating features such as bag sealing, dust collection, and air filtration to minimize environmental impact and ensure worker safety.
Benefits and Applications
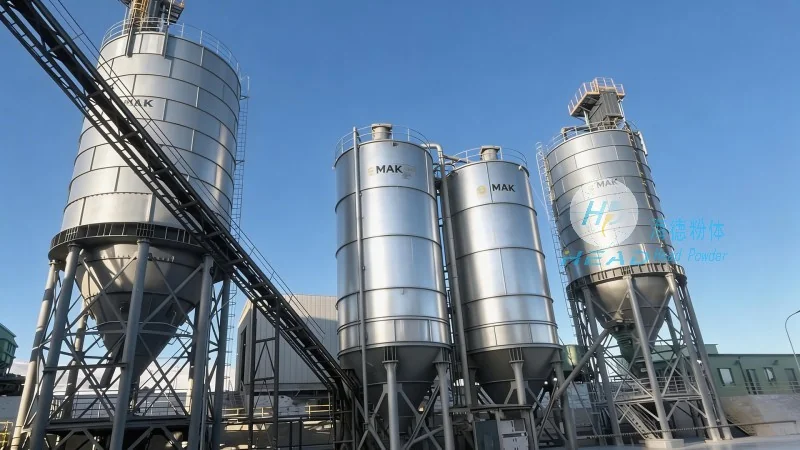
The tonne bag unloading station with a pneumatic conveying system offers numerous benefits for industrial operations. These benefits include increased efficiency in material handling, reduced labor costs due to automated processes, improved safety by minimizing manual handling and dust exposure, and enhanced product quality by preventing contamination and material loss. The system is widely used in various industries, including food processing, chemical manufacturing, pharmaceuticals, and mining, where bulk materials are handled in large quantities. For instance, in the food industry, the system can be used to handle ingredients like flour, sugar, or grains from tonne bags, ensuring a clean and efficient transfer process. In the chemical industry, it can be used to handle powders and granules, such as fertilizers or pigments, while maintaining strict safety and environmental standards.
Conclusion
In conclusion, the tonne bag unloading station pneumatic conveying system is a sophisticated and efficient solution for handling bulk materials in industrial settings. Its design, based on principles of air-based material transport and careful consideration of material properties, ensures reliable and safe operation. By integrating advanced components and adhering to best practices in material handling, this system helps industrial facilities optimize their processes, reduce costs, and improve overall productivity. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems, leveraging years of experience to deliver solutions tailored to the specific needs of industrial clients.