

What is Dust-Free Automatic Material Pneumatic Conveying? What Are Its Design Principles?
Dust-free automatic material pneumatic conveying is a sophisticated industrial technology designed to transport bulk materials through a closed system using air as the primary conveying medium. This method is widely used in various industries, including pharmaceuticals, food processing, and chemical manufacturing, where maintaining a clean and controlled environment is critical. The core of this technology lies in its ability to move materials without exposing them to external contaminants, ensuring product purity and operational efficiency.
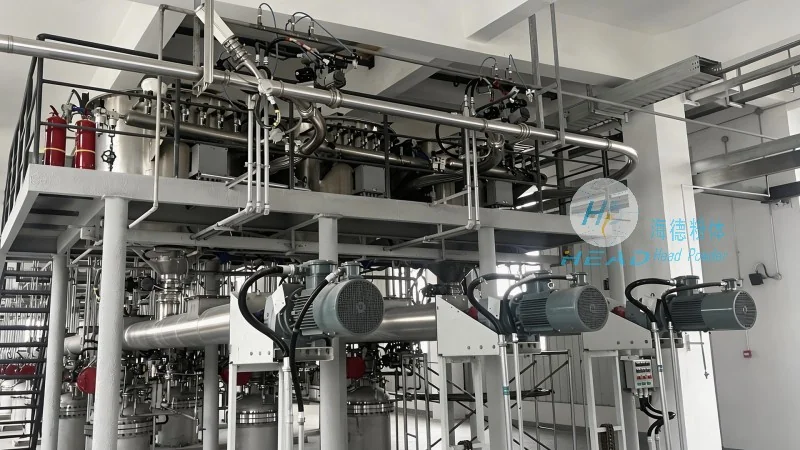
Understanding the Core Components and Design Principles
The design of a dust-free automatic material pneumatic conveying system involves several key components that work in tandem to achieve efficient and clean material transport. The primary components include a material feed hopper, a conveying line (often equipped with filters and cyclones), a dust collection system, and a control unit. The system operates on the principle of creating a pressure differential between the inlet and outlet of the conveying line. By introducing air into the system, the material is lifted and transported through the pipeline. The design emphasizes the use of high-efficiency filters and sealed connections to prevent dust leakage and maintain a sterile environment. This approach ensures that the material remains free from contamination throughout the conveying process, which is essential for industries with stringent quality standards.

Key Design Principles for Efficient and Clean Material Transport
Several critical design principles underpin the effectiveness of dust-free automatic material pneumatic conveying systems. One of the most important principles is the use of a closed-loop system, which minimizes exposure to external air and contaminants. This design feature is crucial for maintaining the integrity of sensitive materials, such as pharmaceutical powders or food ingredients. Another key principle is the selection of appropriate air velocities and pressure levels. The system must be designed to handle the specific properties of the material being conveyed, including its density, particle size, and flowability. For example, materials with high moisture content or fine particles may require higher air velocities to ensure proper suspension and transport. The design also incorporates features like cyclone separators and bag filters to capture and remove any particles that may escape the conveying line, further enhancing the dust-free operation. Additionally, the system is equipped with pressure sensors and control valves to regulate air flow and maintain consistent conveying performance, ensuring that the material is transported reliably and without interruption.
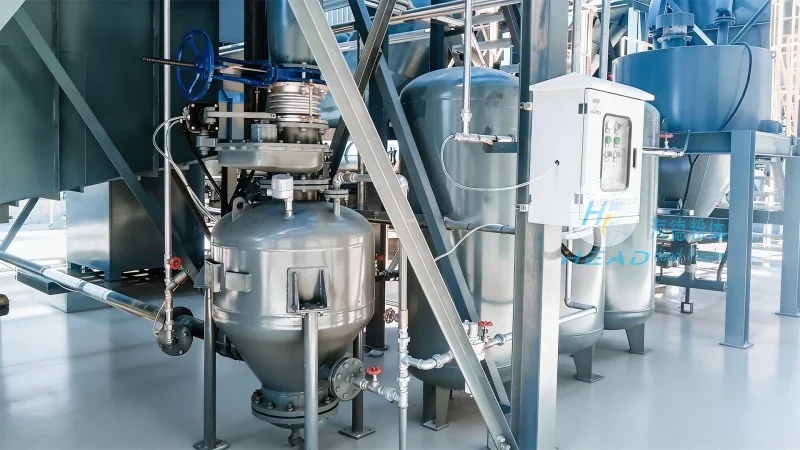
Applications and Benefits in Industrial Settings
Dust-free automatic material pneumatic conveying systems are employed in a wide range of industrial applications where material handling requires precision and cleanliness. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the final product meets strict regulatory standards. The food processing sector utilizes these systems for handling ingredients like flour, sugar, and spices, maintaining food safety and quality. In chemical manufacturing, the technology is applied to transport powders and granules, preventing cross-contamination and protecting workers from hazardous materials. The benefits of this technology extend beyond just cleanliness; it also enhances operational efficiency by reducing downtime due to material blockages and improving overall process reliability. Furthermore, the closed system design minimizes the risk of dust explosions, making it a safer option compared to traditional open-air conveying methods.
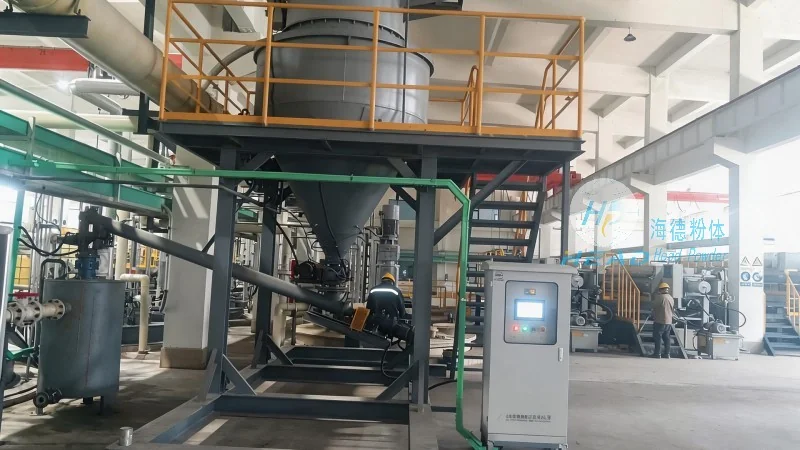
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design and production of dust-free automatic material pneumatic conveying systems. With a strong commitment to quality and innovation, HeadPowder has established itself as a trusted partner for industries requiring high-purity material handling solutions. The company's headquarters is located in Shandong, China, where it leverages advanced engineering capabilities and state-of-the-art manufacturing facilities to develop customized solutions tailored to the unique needs of each client. HeadPowder's team of experienced engineers and technicians works closely with clients to understand their specific requirements, ensuring that the final system meets all operational and regulatory standards. The company's products are known for their reliability, efficiency, and adherence to industry best practices, making them a preferred choice for businesses seeking to enhance their material handling processes while maintaining the highest standards of cleanliness and safety.