

Classification and Application Analysis of Purified Ash Pneumatic Conveying Systems
Pneumatic conveying systems are essential in industrial processes for transporting bulk materials like ash and other powders. The "purified ash" variant focuses on systems designed to handle ash with specific purification requirements, ensuring efficient and clean material transport. These systems are critical in power plants and other facilities where ash management is a key operational concern.
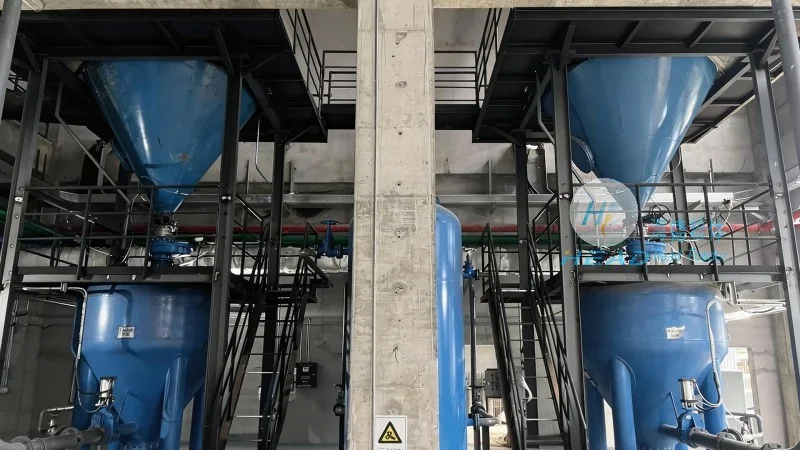
Classification of Pneumatic Conveying Systems for Ash Handling
There are several classifications of pneumatic conveying systems used for ash handling, each tailored to different operational needs and material characteristics. The primary types include positive pressure systems, negative pressure systems, and hybrid systems. Positive pressure systems use a blower to push air and material through the pipeline, while negative pressure systems use a vacuum to draw material into the system. Hybrid systems combine elements of both, offering flexibility in handling different material properties and system configurations.
Key Components and Working Principles
The core components of a purified ash pneumatic conveying system include the material feed hopper, air supply unit (blower or vacuum pump), conveying pipeline, and material discharge unit. The system operates by introducing air into the pipeline, creating a flow that carries the ash particles. The air velocity must be sufficient to overcome the gravitational forces and frictional resistance of the material, ensuring stable transport. For purified ash, additional components such as filters and dust collection systems may be integrated to maintain air quality and comply with environmental regulations.
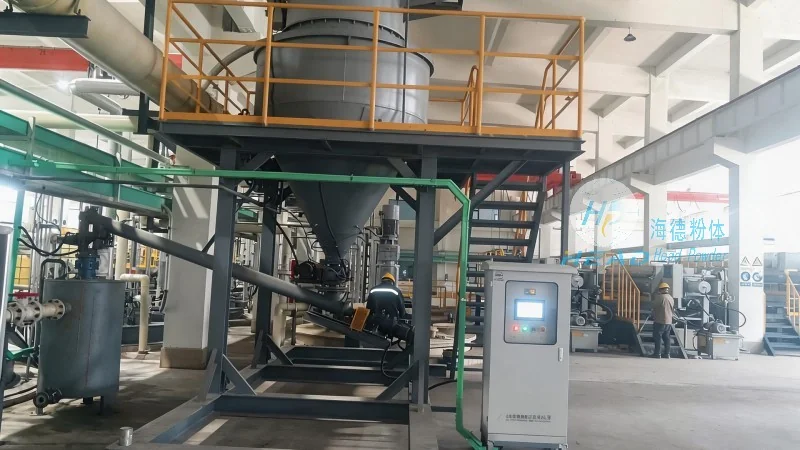
Applications in Industrial Settings
Purified ash pneumatic conveying systems are widely used in power generation, cement production, and other industrial sectors where large volumes of ash need to be transported. In power plants, these systems are crucial for transporting fly ash from boilers to storage or disposal facilities. The systems ensure that ash is moved efficiently without the need for manual handling, reducing labor costs and improving safety. In cement plants, ash is often used as a supplementary cementitious material, and pneumatic conveying systems facilitate its transport from storage to the production line. The ability to handle large volumes and maintain material quality makes these systems indispensable in these applications.
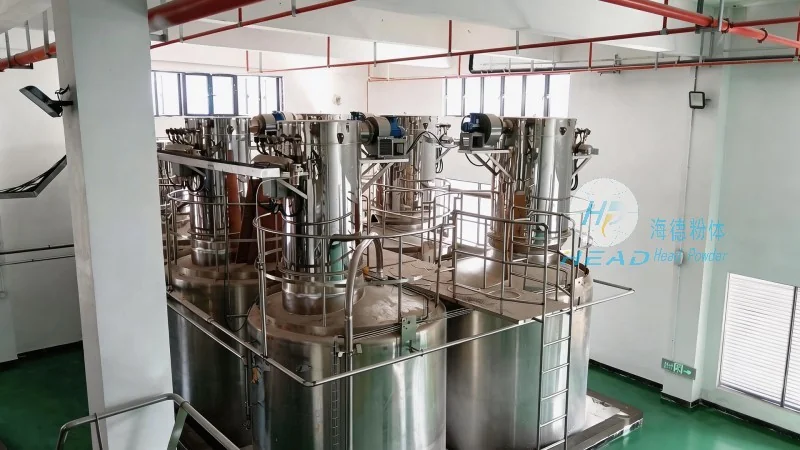
Advantages of Using Pneumatic Conveying for Ash Handling
Compared to traditional methods like belt conveyors or trucks, pneumatic conveying systems offer several advantages. They provide a closed system, which helps in controlling dust emissions and maintaining environmental standards. The systems are also more flexible in terms of layout, as they can be installed in various configurations to fit the space constraints of a facility. Additionally, pneumatic conveying reduces the risk of material contamination and damage, which is critical for ash that may be used in other industrial processes. The energy efficiency of modern systems, particularly positive pressure designs, also contributes to lower operational costs over time.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems for industrial applications. With a focus on purified ash handling, the company leverages years of experience to deliver customized solutions that meet the specific needs of clients. The company's headquarters is located in Shandong, China, and it serves a global market with a commitment to quality and reliability. HeadPowder's systems are engineered to ensure efficient material transport while adhering to environmental regulations, making them a trusted choice for industries requiring high-performance ash handling solutions.