

Role of Pneumatic Conveying in Urea Transportation
Urea, a vital nitrogen fertilizer, is widely utilized in agricultural and industrial sectors. The efficient and secure transportation of urea is crucial for supply chain management and operational efficiency. Pneumatic conveying technology has become a reliable method for handling urea, offering advantages over conventional approaches like belt conveyors or truck transport. This article examines the role of pneumatic conveying in urea transportation, highlighting its benefits and practical applications.
Understanding Pneumatic Conveying for Urea
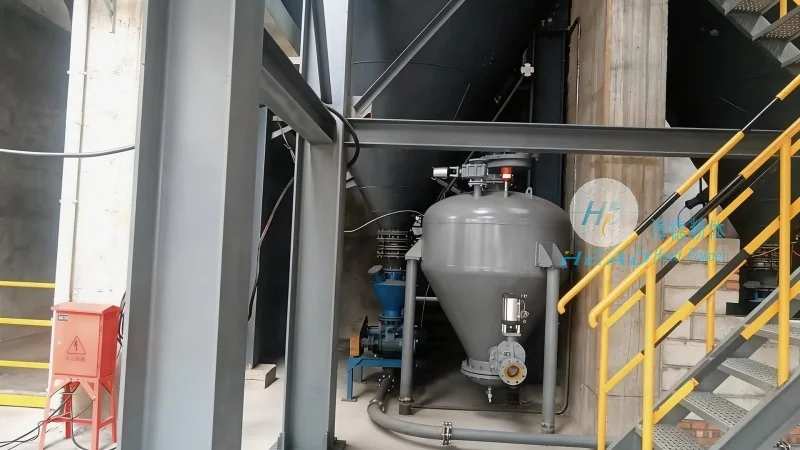
Pneumatic conveying systems utilize air or gas to transport bulk materials such as urea through a pipeline. These systems are typically classified into dilute-phase and dense-phase categories. Dilute-phase systems are well-suited for long-distance and high-volume transport, while dense-phase systems are ideal for short distances and require precise control. The selection of a system depends on factors including urea characteristics, distance, and required flow rate. For urea, a fine granular material, dilute-phase systems are commonly employed due to their capacity to handle high capacities and preserve material integrity.
Benefits of Pneumatic Conveying in Urea Handling
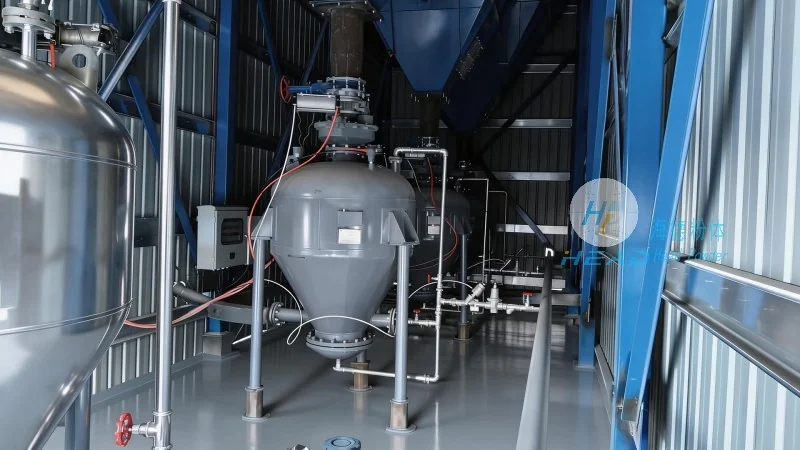
One of the primary advantages of pneumatic conveying for urea is its ability to minimize product degradation. Unlike mechanical conveyors, which can cause friction and abrasion, pneumatic systems reduce the risk of clumping or particle damage. This is critical for maintaining urea's quality, as any degradation can affect its effectiveness as a fertilizer. Additionally, pneumatic conveying enhances safety by eliminating the need for manual handling of bulk materials, reducing accident risks and dust exposure. The enclosed pipeline system also aids in controlling dust emissions, aligning with environmental regulations.
Applications in Urea Transportation
Pneumatic conveying is widely applied in various stages of urea transportation. From production plants to storage facilities, and then to distribution centers or farms, these systems ensure seamless material flow. In industrial settings, such as fertilizer manufacturing plants, pneumatic conveyors connect reactors, storage silos, and packaging lines, enabling continuous production processes. For agricultural applications, the technology is used to transport urea from storage silos to application equipment, ensuring timely and efficient delivery to fields. The flexibility of pneumatic systems allows them to adapt to different operational needs, whether it's a small-scale farm or a large industrial facility.
Key Considerations for Implementing Pneumatic Conveying
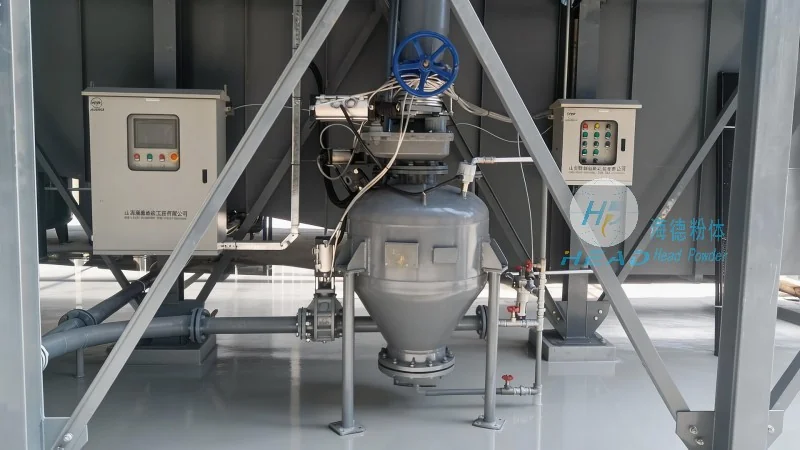
When implementing pneumatic conveying for urea, several factors must be considered to ensure optimal performance. Material properties, including particle size, density, and moisture content, play a significant role in system design. For urea, which has a relatively uniform particle size, the system can be optimized for consistent flow. Air pressure and velocity are critical parameters affecting conveying efficiency and energy consumption. Proper system sizing, including pipeline diameter and length, is essential to avoid blockages or excessive energy use. Regular maintenance and monitoring are also necessary to prevent system failures and ensure long-term reliability.
Case Study: Shandong HeadPowder Engineering Co., Ltd.
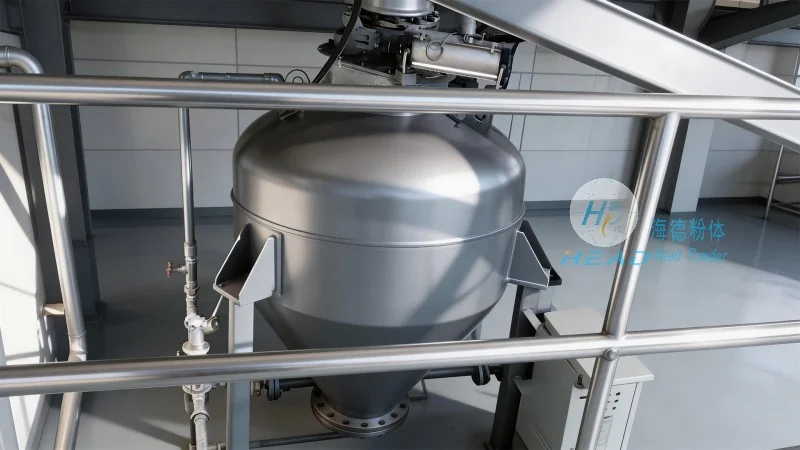
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, has extensive experience in designing and implementing systems for urea transportation. The company specializes in customizing solutions to meet specific client needs, ensuring that the systems are tailored to the unique requirements of each project. With a focus on quality and efficiency, HeadPowder has successfully delivered numerous pneumatic conveying projects across China, contributing to the smooth operation of urea supply chains. The company's expertise in material handling and process engineering has helped clients improve operational efficiency and reduce costs associated with traditional transportation methods.
Conclusion
Pneumatic conveying plays a vital role in the efficient and safe transportation of urea. By leveraging this technology, industries can enhance supply chain management, reduce operational risks, and maintain product quality. As the demand for urea continues to grow, the adoption of advanced pneumatic conveying systems will become increasingly important. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of providing innovative solutions that address the evolving needs of the urea industry, ensuring reliable and sustainable transportation of this essential fertilizer.