

Design of Quartz Sand Negative Pressure Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. The company's core focus is on providing efficient and reliable solutions for the transportation of bulk materials, with a particular emphasis on quartz sand handling. This article introduces the design principles and key features of a negative pressure pneumatic conveying system specifically engineered for quartz sand applications.
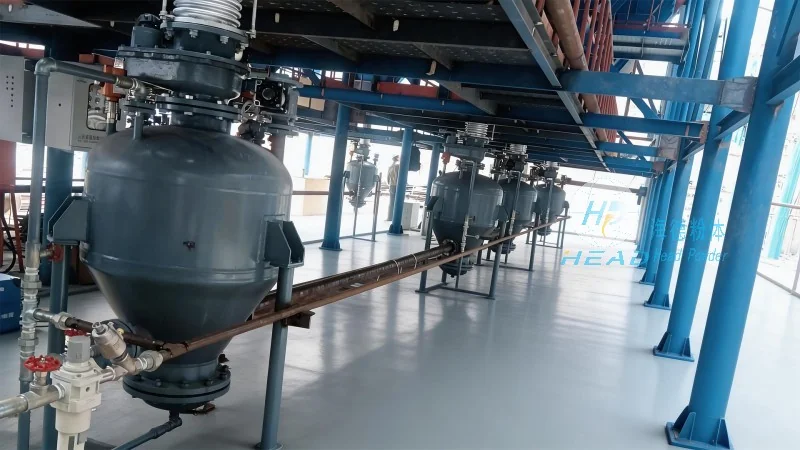
Overview of Negative Pressure Pneumatic Conveying Technology
Negative pressure pneumatic conveying, also known as suction conveying, is a method that uses a vacuum to draw material from a source and transport it through a pipeline to a destination. This approach is highly effective for handling fine to medium-sized particles like quartz sand, offering advantages such as low material degradation, minimal dust generation, and the ability to convey materials over long distances with minimal energy consumption. The system operates by creating a pressure differential between the source and the receiver, ensuring a continuous and controlled flow of material.
Key Design Considerations for Quartz Sand Conveying
When designing a negative pressure pneumatic conveying system for quartz sand, several critical factors must be considered to ensure optimal performance and durability. First, the material's physical properties, including particle size distribution, density, and moisture content, are analyzed to determine the appropriate air velocity and pipeline diameter. Quartz sand typically consists of hard, abrasive particles, which necessitates the use of high-quality, wear-resistant components such as stainless steel or special alloys for the conveying line and equipment. Additionally, the system's capacity and the required conveying distance are evaluated to select the right blower or vacuum pump, ensuring sufficient airflow to maintain the material's suspension without causing excessive pressure drops or energy waste.
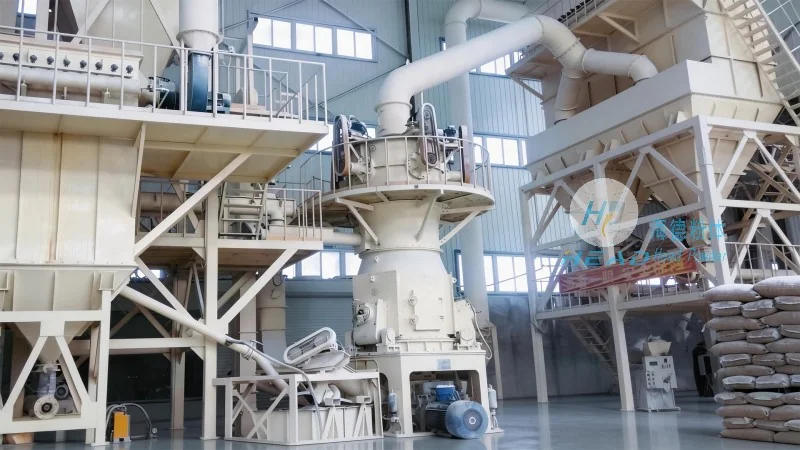
Components and Functional Design of the System
The negative pressure pneumatic conveying system for quartz sand includes several key components, each designed to work in concert to achieve efficient material transport. The primary components are the suction hopper, which collects the quartz sand and initiates the suction process; the pipeline network, which transports the material from the source to the receiver; the receiver, which collects the conveyed material; and the vacuum pump or blower, which provides the necessary suction force. The suction hopper is equipped with a rotary valve or feeder to control the material flow and prevent blockages, while the pipeline is designed with appropriate bends and fittings to minimize pressure losses and maintain consistent airflow. The receiver is typically a sealed container to prevent dust emissions and ensure safe material handling. The vacuum pump, often a roots blower or a rotary vane pump, is selected based on the system's required airflow and pressure, ensuring reliable operation under varying load conditions.
Advantages of Negative Pressure Conveying for Quartz Sand
Compared to positive pressure conveying systems, negative pressure pneumatic conveying offers several advantages when handling quartz sand. One of the most significant benefits is the reduced risk of material contamination and degradation, as the system operates in a sealed environment with minimal exposure to external air. This is particularly important for quartz sand, which is often used in applications requiring high purity, such as glass manufacturing or abrasive products. Additionally, negative pressure systems are more energy-efficient for long-distance conveying, as they require less power to maintain the vacuum compared to the higher pressures needed in positive pressure systems. The low dust generation also contributes to a safer working environment and easier maintenance, as there is less accumulation of fine particles in the equipment and surroundings.
Application Scenarios and Customization Options
The negative pressure pneumatic conveying system designed for quartz sand is versatile and can be adapted to various industrial applications. Common uses include transporting quartz sand from storage silos to processing plants, conveying material between different production stages, and handling quartz sand in environments where dust control is critical. The system can be customized to meet specific operational requirements, such as varying conveying distances, material flow rates, or the need for multiple delivery points. For example, the pipeline can be extended or branched to serve several receivers, and the vacuum pump can be upgraded to handle higher capacities or longer distances. The company, Shandong HeadPowder Engineering Co., Ltd., offers tailored solutions based on client needs, ensuring that the system is optimized for the specific application and operational conditions.
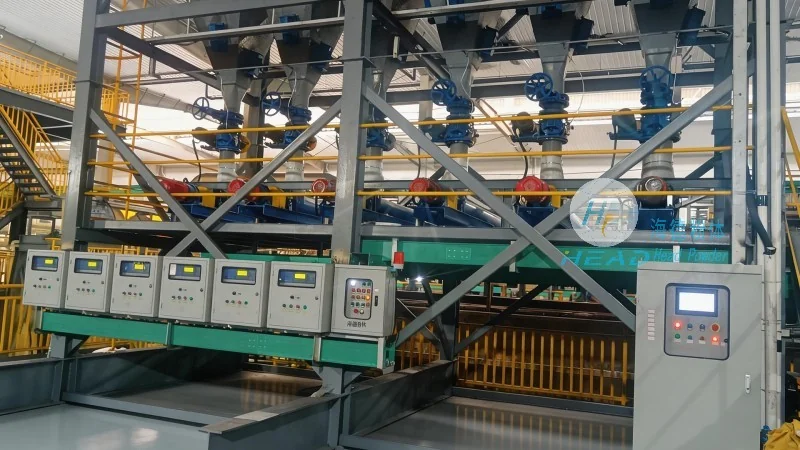
Maintenance and Operational Guidelines
To ensure the longevity and reliability of the negative pressure pneumatic conveying system, proper maintenance and operational guidelines are essential. Regular inspections of the pipeline and components for signs of wear or damage are recommended, particularly in areas exposed to abrasive quartz sand particles. The rotary valve and feeder in the suction hopper should be checked for proper operation and lubricated as needed to prevent blockages. The vacuum pump should be maintained according to the manufacturer's specifications, including regular cleaning of filters and checking for proper lubrication. Operational guidelines include starting the system with the suction hopper filled to prevent air leaks and ensuring that the receiver is properly sealed to maintain the vacuum. By following these guidelines, the system can operate efficiently and safely for extended periods, minimizing downtime and maintenance costs.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. has developed a sophisticated negative pressure pneumatic conveying system specifically designed for quartz sand applications. By incorporating advanced design principles and high-quality components, the system offers efficient, reliable, and low-dust material transport. The company's expertise in engineering and manufacturing ensures that the system meets the demanding requirements of industrial applications, providing a durable and cost-effective solution for quartz sand handling. With its focus on customer needs and customized solutions, Shandong HeadPowder Engineering Co., Ltd. continues to be a leader in the field of pneumatic conveying technology, delivering high-performance equipment that enhances operational efficiency and safety in various industries.