

Principle and Working Scene Characteristics of Bag Breakage Material Conveying Equipment
Bag breakage material conveying equipment is a specialized system designed to handle bulk materials that have been compromised in their packaging, such as broken bags or containers. This equipment plays a crucial role in industrial settings where material handling efficiency and safety are paramount. The following sections will explore the fundamental principles behind these systems and the specific working scenarios where they are most effectively applied.
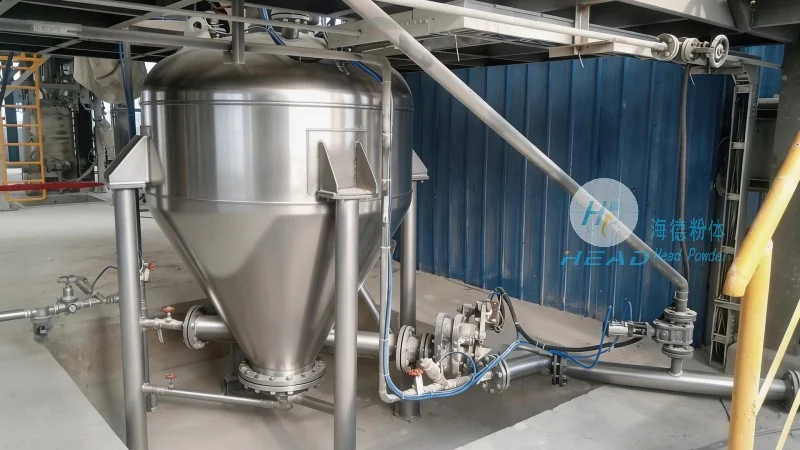
Understanding the Core Principles of Bag Breakage Material Conveying Equipment
At the heart of bag breakage material conveying equipment lies a combination of mechanical and pneumatic components working in tandem to extract and transport materials from damaged packaging. The primary function is to safely and efficiently transfer loose or fragmented materials from the source, such as a storage silo or a hopper, to the next stage of processing or storage. This process typically involves several key steps: material intake, bag or container rupture, material extraction, and conveyance to a collection point or processing unit.
One of the critical principles is the use of controlled air pressure and flow to displace materials from the broken packaging. This method minimizes the risk of material spillage and ensures a clean, contained transfer. The equipment often incorporates features like flexible hoses, rotary valves, or vacuum systems to handle various types of broken bags, including paper, plastic, or composite materials. The design is tailored to accommodate different bag sizes and shapes, making it versatile for diverse industrial applications.
Key Working Scene Characteristics and Applications
The effectiveness of bag breakage material conveying equipment is highly dependent on the specific working environment and the nature of the materials being handled. Different industries, such as food processing, chemical manufacturing, and mining, utilize these systems under distinct conditions that require specialized configurations.

In the food processing industry, for example, the equipment must adhere to strict hygiene standards. This means materials like grains, powders, or dried fruits are transferred in a way that prevents contamination and maintains product quality. The conveying systems often include stainless steel components and sealed pathways to ensure food safety. The working scene may involve large-scale production lines where broken bags from raw material storage are processed quickly to keep production running smoothly.
In the chemical manufacturing sector, the focus shifts to handling potentially hazardous materials. The equipment is designed with robust, corrosion-resistant materials to withstand the chemical properties of the substances being processed. The working scene might involve transferring powders or granules from storage silos to reactors or mixing units, with strict safety protocols in place to prevent leaks or exposure. The conveying system’s ability to handle fine powders without clogging is particularly important in this environment.
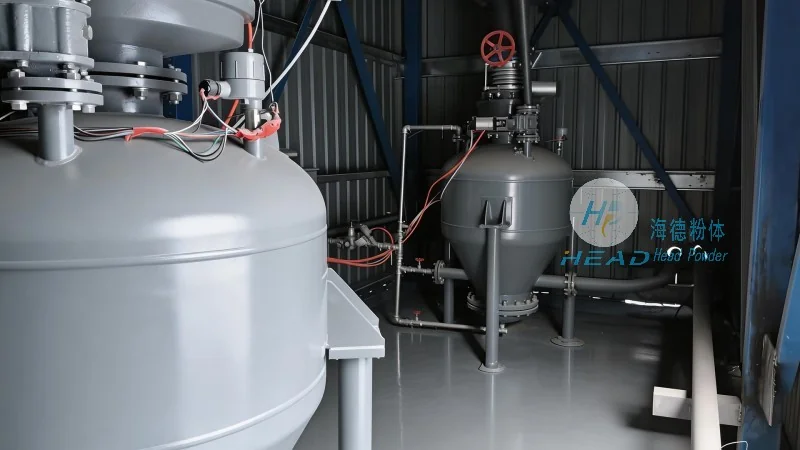
For mining and mineral processing applications, the equipment is built to handle abrasive and heavy materials. The working scene typically involves large-scale operations where broken bags containing ore or minerals are processed. The conveying systems are often more rugged, with heavy-duty components that can withstand the harsh conditions of mining sites. The focus here is on durability and efficiency in moving large volumes of material over long distances.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the material handling industry, specializes in designing and supplying advanced bag breakage material conveying equipment. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted provider of solutions tailored to the needs of various industrial sectors. The company’s commitment to quality, innovation, and customer satisfaction is reflected in its comprehensive product line and technical expertise.
HeadPowder’s team of engineers and technicians work closely with clients to understand their specific material handling challenges and develop customized solutions. The company’s facilities in Shandong are equipped with state-of-the-art manufacturing capabilities, ensuring that each piece of equipment meets the highest standards of performance and reliability. By leveraging years of experience in the industry, HeadPowder continues to enhance its product offerings to meet evolving market demands.