

Principle and Operational Characteristics of Tonne Bag Quantitative Feeding Powder Material Handling
For industrial applications requiring precise and efficient handling of bulk powders, the tonne bag quantitative feeding system offers a robust solution. This system is designed to automate the process of measuring and dispensing powder materials from large tonne bags, ensuring consistent quality and operational efficiency in various production environments. The following sections will explore the fundamental principles behind this technology and the key operational scenarios where it excels, providing insights into how it addresses the challenges of bulk material handling in modern manufacturing.
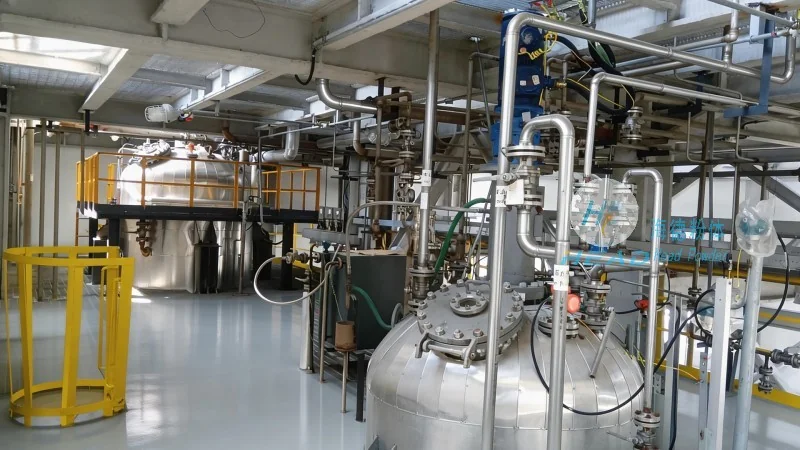
Core Principles of the Tonne Bag Quantitative Feeding System
The tonne bag quantitative feeding system operates on a combination of advanced measurement technologies and automated control mechanisms. At its heart, the system utilizes high-precision load cells or volumetric sensors to accurately determine the weight or volume of powder being dispensed from a tonne bag. These sensors provide real-time data to the control unit, which then adjusts the feeding rate to maintain the desired quantity. The system typically includes a hopper that receives the powder from the tonne bag, a conveyor or feeding mechanism that transports the material to the processing equipment, and a control panel that manages the entire operation. By integrating these components, the system ensures that each batch of powder is delivered with minimal variance, meeting stringent quality standards for downstream processes. The control unit often employs sophisticated algorithms, such as PID (Proportional-Integral-Derivative) control, to fine-tune the feeding rate based on real-time sensor feedback, further enhancing accuracy and stability. This closed-loop control system minimizes the impact of external factors like bag weight variations or material flow inconsistencies, ensuring consistent output regardless of the operating conditions.
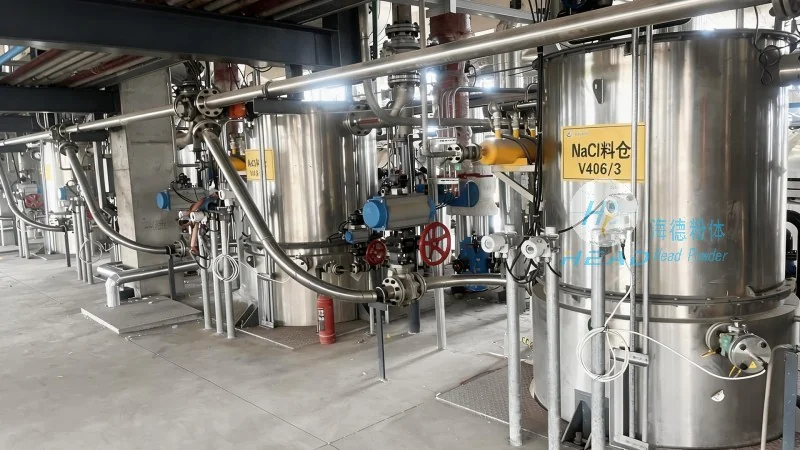
Key Working Scene Characteristics
The tonne bag quantitative feeding system is particularly well-suited for industrial settings where large volumes of bulk powders are handled, such as in chemical manufacturing, food processing, pharmaceutical production, and mining operations. In these environments, the system's ability to handle tonne bags (typically 1 tonne or 1000 kg) directly, without the need for intermediate storage or manual handling, significantly reduces labor costs and operational downtime. The automated nature of the system also minimizes human error, which is critical when dealing with materials that require precise dosing for product consistency. Additionally, the system's modular design allows for easy integration with existing production lines, making it a versatile solution for both new installations and retrofit projects. The operational scenarios often involve continuous or batch processing, where the system can be programmed to feed specific quantities at predetermined intervals, ensuring smooth workflow and optimal resource utilization. For example, in a chemical plant producing fertilizers, the system can feed precise amounts of raw materials into a mixer, while in a food processing facility, it can dispense exact quantities of flour or sugar into a production line. The adaptability of the system to different materials and processes makes it a valuable asset in any industrial setting where bulk powder handling is essential.
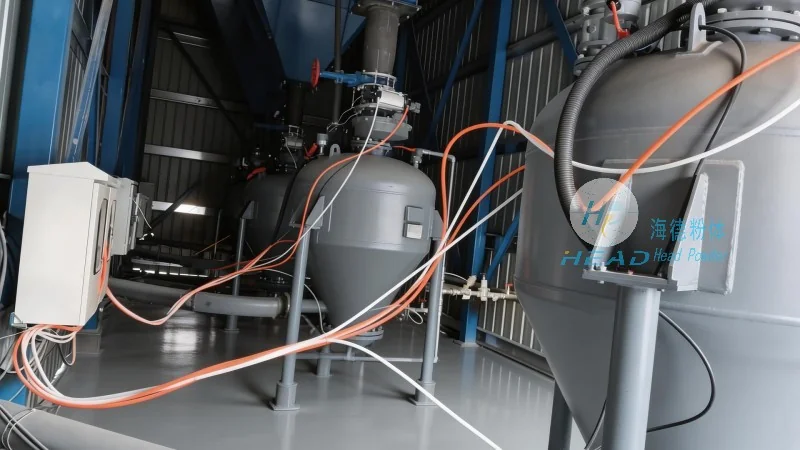
Company Background and Expertise
HeadPowder, a leading provider of powder handling solutions, specializes in developing and manufacturing advanced material handling systems tailored to the needs of diverse industries. With its headquarters in Shandong, China, HeadPowder Engineering Co., Ltd. has built a reputation for delivering reliable, efficient, and cost-effective equipment that enhances productivity and product quality. The company's team of engineers and technicians brings extensive experience in powder technology, mechanical design, and automation, ensuring that each system is customized to meet the unique requirements of clients. By leveraging cutting-edge technology and rigorous quality control processes, HeadPowder has become a trusted partner for businesses seeking to optimize their powder handling operations. The company's commitment to innovation and customer satisfaction has enabled it to serve a wide range of industries, from chemical and pharmaceutical to food and mining, with solutions that address the most challenging material handling needs. HeadPowder's research and development efforts focus on improving system accuracy, durability, and energy efficiency, ensuring that their products remain at the forefront of the industry. The company also provides comprehensive after-sales support, including installation, maintenance, and technical assistance, to ensure that clients can maximize the performance of their tonne bag quantitative feeding systems. Through continuous improvement and customer-centric approach, HeadPowder has established itself as a key player in the global powder handling market.