

Principle and Working Scene Characteristics of Calcium Carbonate Stone Powder Pneumatic Conveying Ma
HeadPowder, a leading manufacturer in the field of material handling equipment, specializes in providing efficient and reliable solutions for the transportation of calcium carbonate, a widely used fine powder in various industrial applications. The company is headquartered in Shandong, China, and has built a strong reputation for delivering high-performance pneumatic conveying systems tailored to the specific needs of clients in sectors such as chemical processing, food production, and pharmaceutical manufacturing.
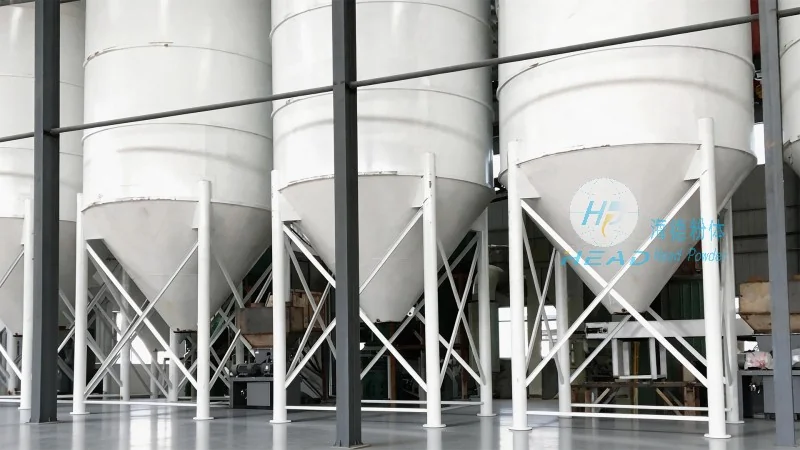
Overview of Calcium Carbonate Stone Powder Pneumatic Conveying Machines
A calcium carbonate stone powder pneumatic conveying machine is a specialized piece of equipment designed to transport fine powders like calcium carbonate through a pipeline using compressed air. This technology offers a cost-effective and flexible alternative to traditional bulk material handling methods, which often involve complex and expensive equipment such as screw conveyors or belt conveyors. The system typically comprises several key components: a hopper for material storage, a rotary airlock valve to control discharge, a pipeline network for conveying, and a receiver to collect the material at the destination. Each component works in concert to ensure smooth, continuous, and controlled movement of the powder.
The Working Principle of Pneumatic Conveying Systems
The fundamental principle of pneumatic conveying for calcium carbonate stone powders is the creation of a fluidized bed within the conveying line. When compressed air is introduced into the hopper, it lifts the powder particles, forming a cloud of fine particles that are then drawn through the pipeline by the air flow. The rotary airlock valve at the hopper outlet regulates the discharge rate, preventing clogging and maintaining a consistent flow. The receiver at the end of the pipeline collects the conveyed powder, while the air is filtered and returned to the system, minimizing waste and energy consumption. This closed-loop system ensures that the material is handled hygienically and without exposure to the environment, which is critical for applications involving food-grade or pharmaceutical-grade powders.
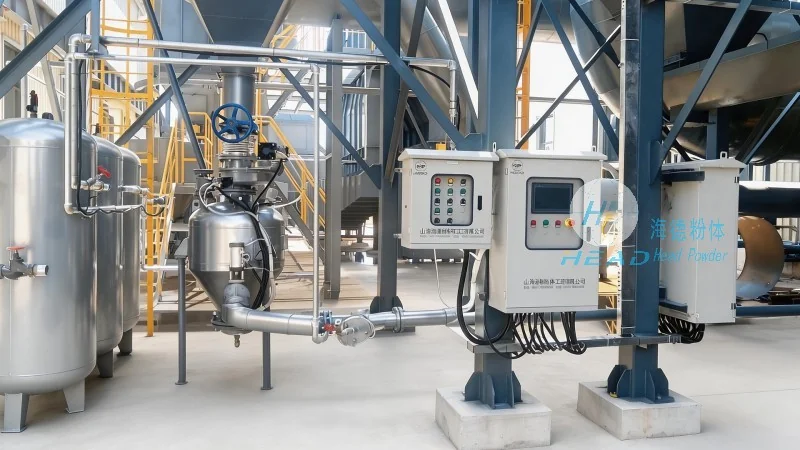
Key Characteristics of Working Scenes for Pneumatic Conveying Machines
The working scene characteristics of calcium carbonate stone powder pneumatic conveying machines are tailored to meet the specific demands of industrial environments. These systems are commonly used in settings where dust control is paramount, as the enclosed pipeline design prevents airborne particle dispersion, reducing health hazards and maintaining a clean workspace. The flexibility of the system allows for easy integration into existing production lines, with the ability to adjust the conveying distance or direction by modifying the pipeline layout. Additionally, the low maintenance requirements and the ability to handle varying powder flow rates make these machines suitable for both small-scale and large-scale production facilities. For instance, in a chemical plant producing calcium carbonate-based products, the system can be configured to transport the powder from a storage silo to a mixing or packaging area, optimizing the workflow and reducing downtime.
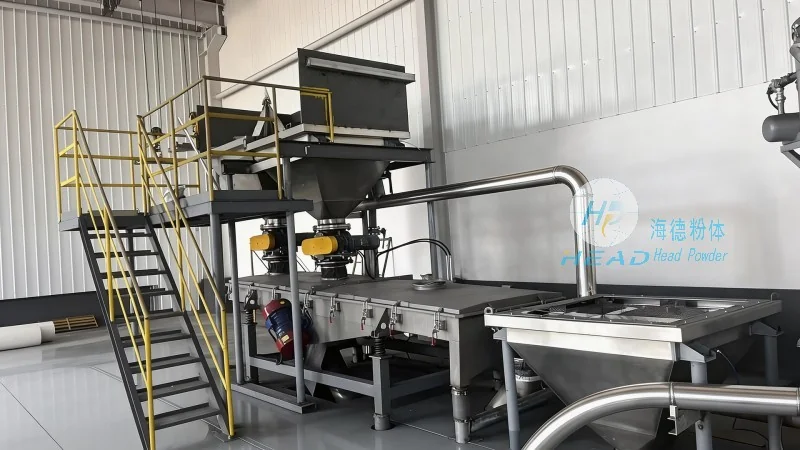
Technical Advantages and Practical Applications
HeadPowder Engineering Co., Ltd. offers pneumatic conveying machines for calcium carbonate stone powders that deliver several technical advantages. The use of positive pressure systems ensures that the material is conveyed without the need for vacuum pumps, reducing energy costs and maintenance complexity. The system's ability to handle abrasive powders, such as calcium carbonate, is enhanced by the use of wear-resistant materials in the hopper and pipeline components, extending the equipment's service life. In practical applications, these machines are widely used in the chemical, food, and pharmaceutical industries, where the precise and hygienic handling of fine powders is essential. The systems are also suitable for applications requiring high conveying capacities, such as in large-scale mineral processing plants. For example, in a calcium carbonate mining operation, the pneumatic conveying system can transport the ground powder from the processing plant to a storage facility or a shipping port, ensuring efficient material movement and reducing the need for manual handling.
Conclusion and Company Information
Calcium carbonate stone powder pneumatic conveying machines represent a modern and efficient solution for the transportation of fine materials. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, continues to innovate and provide high-quality equipment that meets the evolving needs of industrial clients. By leveraging advanced pneumatic conveying technology, the company ensures that its products deliver reliable performance, low operational costs, and minimal environmental impact, making them an ideal choice for industries seeking sustainable and effective material handling solutions. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the material handling equipment market, providing tailored solutions that enhance productivity and operational efficiency for its clients worldwide.