

Working Principle and Features of Pharmaceutical Bulk Material Pneumatic Conveying Systems
Pharmaceutical bulk material pneumatic conveying systems are critical components in pharmaceutical manufacturing, responsible for the safe and efficient transport of powders and granules. These systems are designed to maintain product integrity while adhering to strict regulatory standards, making them indispensable in the production of pharmaceuticals. Understanding the working principle and key features of such systems is essential for evaluating their suitability for various pharmaceutical processes.
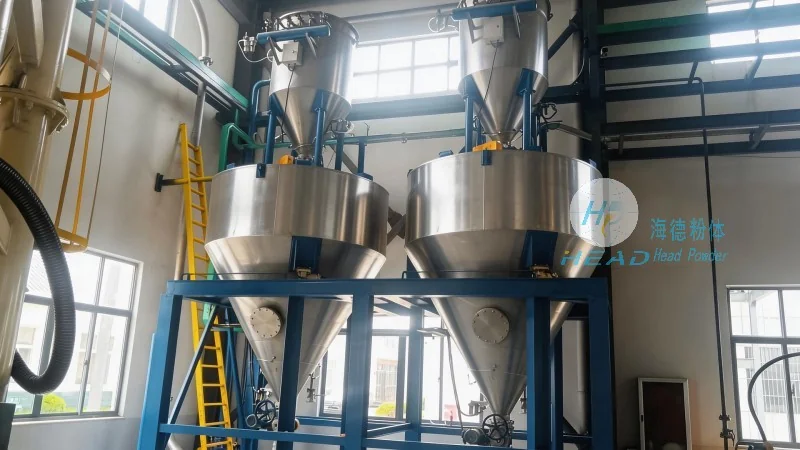
Working Principle of Pharmaceutical Bulk Material Pneumatic Conveying Systems
The fundamental working principle of pharmaceutical bulk material pneumatic conveying systems relies on the use of compressed air or other gases to create a pressure differential that propels bulk materials through a pipeline network. The system typically comprises several key components: a material hopper for storing the bulk material, a feeder to control the material flow rate, a conveying line where the material is transported, and a receiver for depositing the material at the destination. The process initiates when bulk material is fed into the hopper. The feeder then regulates the material's flow into the conveying line. Compressed air is introduced into the line, generating a pressure gradient that moves the material forward as a suspension. The material is carried by the air stream, ensuring it remains suspended and transported without direct contact with the conveying equipment. This method minimizes contamination risks and preserves the quality of the pharmaceutical product throughout the conveying process.
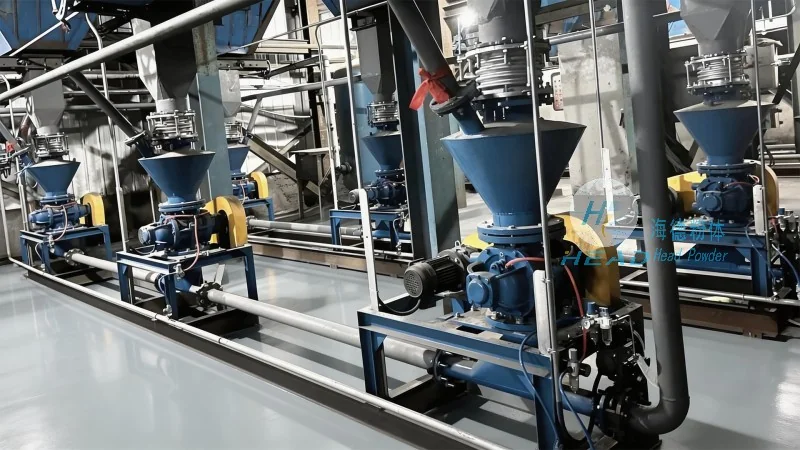
Key Features of Pharmaceutical Bulk Material Pneumatic Conveying Systems
Pharmaceutical bulk material pneumatic conveying systems are distinguished by several key features that enhance their performance and suitability for the pharmaceutical industry. Firstly, they employ a closed system design, which is crucial for maintaining product purity and preventing cross-contamination. The enclosed pipeline network ensures that powders and granules are contained throughout the conveying process, reducing exposure to environmental factors or human contact. Secondly, these systems offer high-precision control over material flow, enabling accurate dosing and consistent product quality. The feeder mechanisms, often equipped with variable speed drives, allow for precise regulation of the material feed rate, which is vital in pharmaceutical manufacturing where uniformity is paramount. Thirdly, the systems are constructed from materials compatible with pharmaceutical products, such as stainless steel, and are designed for easy cleaning and maintenance to meet cGMP guidelines. The components are easily disassembled for thorough cleaning, ensuring that the equipment remains hygienic and compliant with regulatory requirements. Additionally, the systems are equipped with safety features, including pressure relief valves and air filtration systems, to prevent accidents and ensure safe operation. The air filtration systems are essential for removing particulates and ensuring that the air used for conveying is clean, further protecting the product from contamination.
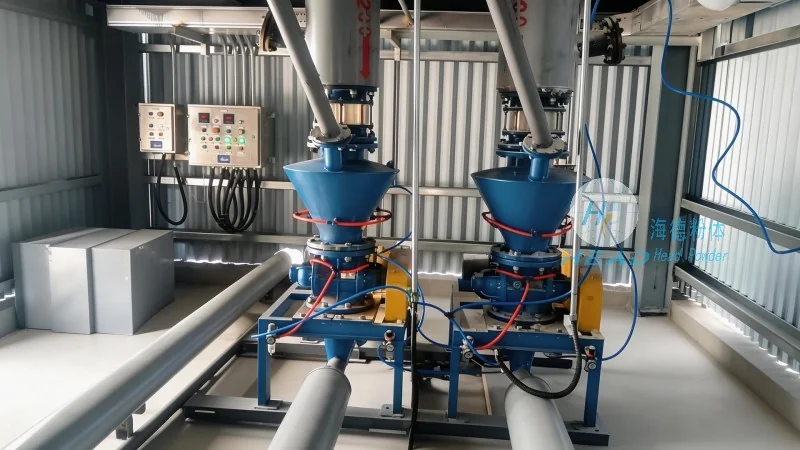
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer of pharmaceutical bulk material handling solutions. The company is headquartered in Shandong, China, and specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems tailored to the pharmaceutical industry's needs. HeadPowder's systems are engineered to meet stringent cGMP and other regulatory standards, ensuring they are suitable for transporting sensitive pharmaceutical materials. The company's commitment to quality and innovation has established it as a trusted partner for pharmaceutical manufacturers globally, providing reliable and efficient solutions for bulk material handling. With a focus on customer satisfaction and product excellence, HeadPowder continues to develop cutting-edge technologies to enhance the performance and safety of its pneumatic conveying systems, supporting the pharmaceutical industry's pursuit of high-quality, safe medications.