

Working Principle and Features of Wheat Bran Powder Conveyors
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling equipment. Our products are engineered to meet the specific demands of industries dealing with bulk materials like wheat bran, ensuring efficient and reliable material transport. This article delves into the working principle and key features of our wheat bran powder conveyors, providing a comprehensive understanding of how these systems operate and their advantages in industrial applications.
Understanding the Working Principle of Wheat Bran Powder Conveyors
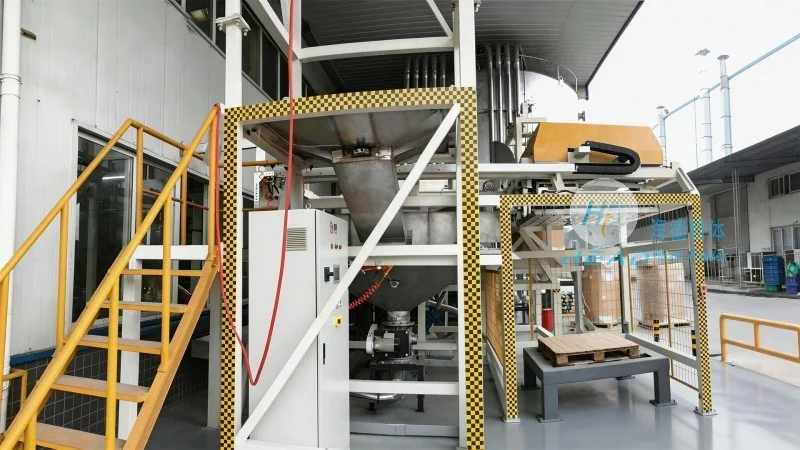
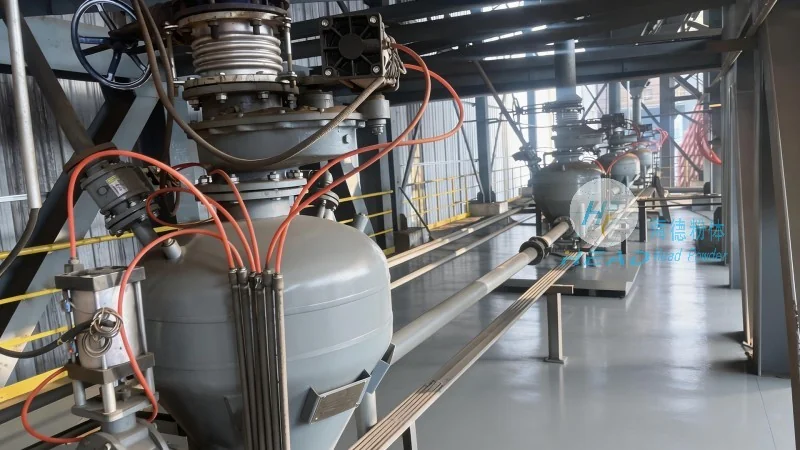
Wheat bran powder conveyors are designed to transport bulk wheat bran efficiently from one location to another within a processing facility. The core working principle involves the use of a conveyor system that can handle fine, dry powders without causing segregation or degradation. These systems typically employ a combination of mechanical components, such as screw conveyors, pneumatic conveying lines, or belt conveyors, depending on the specific requirements of the application. The conveyor mechanism ensures that the wheat bran is moved smoothly through the system, maintaining its quality and preventing clogging or blockages. The design incorporates features like adjustable speed controls and material flow monitoring to optimize performance and ensure consistent operation. By understanding the fundamental mechanics of these conveyors, users can appreciate how they contribute to the overall efficiency of wheat bran processing operations.

Key Features of Wheat Bran Powder Conveyors
HeadPowder's wheat bran powder conveyors are equipped with several distinctive features that enhance their performance and reliability. One of the primary features is the robust construction, which is built to withstand the abrasive nature of wheat bran and other similar powders. The materials used in the construction, such as stainless steel or corrosion-resistant alloys, ensure durability and longevity. Another important feature is the integrated dust control system, which helps maintain a clean and safe working environment by capturing and filtering airborne particles. This not only improves workplace safety but also prevents product contamination. The conveyors also feature adjustable discharge mechanisms, allowing for precise control over the output rate and preventing overloading of downstream equipment. Additionally, the systems are designed with easy maintenance in mind, incorporating accessible components and simple operational controls that reduce downtime and maintenance costs. These features collectively contribute to the high efficiency and reliability of the conveyors, making them an ideal choice for industrial wheat bran processing.
Applications and Benefits in Wheat Bran Processing
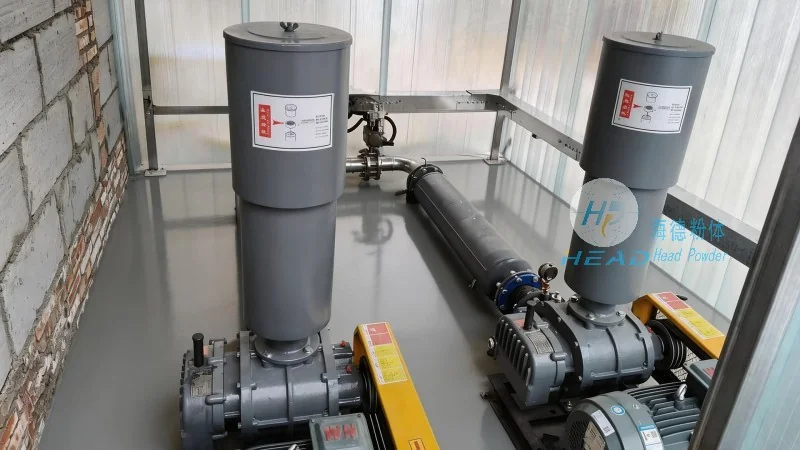
The wheat bran powder conveyors from HeadPowder are widely used in various stages of wheat bran processing, from initial collection to final packaging. In the milling industry, these conveyors are essential for transporting wheat bran from the grinding process to storage silos or packaging lines. Their ability to handle fine powders without segregation ensures that the bran maintains its quality and nutritional value. The conveyors also play a crucial role in feed manufacturing, where consistent and reliable material transport is critical for producing high-quality animal feed. The benefits of using these conveyors extend beyond efficiency; they also contribute to cost savings by reducing material loss and minimizing the need for manual handling. Furthermore, the advanced design of the conveyors helps in maintaining a clean and hygienic environment, which is vital in food processing industries. By leveraging the features and performance of these conveyors, businesses can enhance their operational efficiency and product quality, ultimately leading to better business outcomes.