

Working Principle and Features of Stabilizer Powder Pneumatic Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading enterprise in the field of pneumatic conveying technology, specializing in the design, manufacturing, and installation of systems for transporting powder materials such as stabilizer powders. The company is headquartered in Shandong, China, where it leverages advanced engineering expertise to develop customized solutions tailored to the unique requirements of various industrial applications.
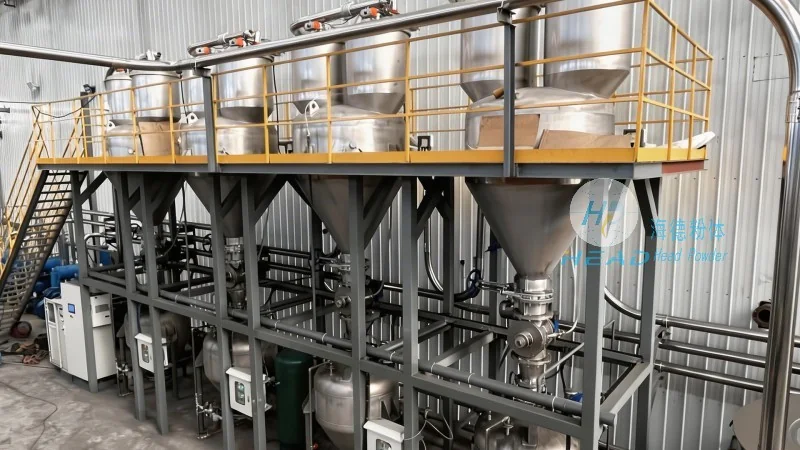
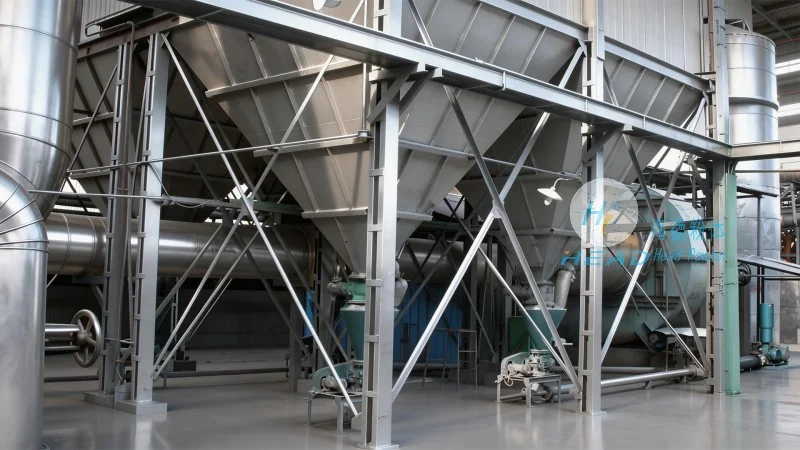
Working Principle of the Stabilizer Powder Pneumatic Conveying System
The core mechanism of the stabilizer powder pneumatic conveying system involves the use of air to transport bulk powder materials through a sealed pipeline network. This process typically operates under either suction or pressure modes, depending on the specific system configuration and application needs. In the suction mode, a vacuum is created at the material inlet to draw the powder into the system, while in the pressure mode, compressed air forces the powder through the pipeline. The system comprises several key components, including a material feeder to control the flow rate of the stabilizer powder, a conveying pipeline that transports the material from the source to the destination, and a separation unit that separates the powder from the air at the end of the line. The feeder ensures a consistent and controlled feed of the powder, preventing blockages and maintaining system efficiency. The conveying pipeline is often made of materials like stainless steel or plastic, selected for their resistance to corrosion and wear from the powder particles. The separation unit, such as a cyclone or bag filter, captures the powder and returns it to the process while releasing the clean air back into the environment. This closed-loop system minimizes dust emissions and ensures compliance with environmental regulations.
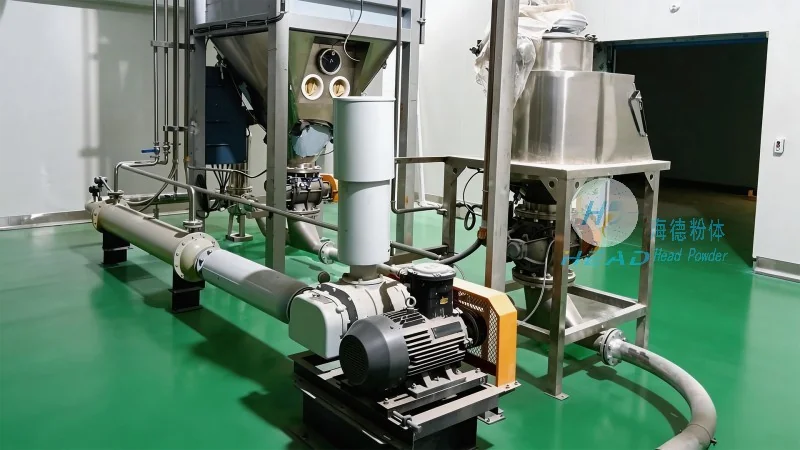
Key Features of the Stabilizer Powder Pneumatic Conveying System
One of the primary advantages of the headpowder stabilizer powder pneumatic conveying system is its high efficiency in material transport. By utilizing air as the conveying medium, the system can move large quantities of powder over considerable distances with minimal energy consumption compared to traditional methods like bucket elevators or belt conveyors. The system is also highly reliable, with advanced control systems that monitor pressure, flow rate, and other critical parameters to prevent system failures and ensure continuous operation. This reliability is particularly important in industries where uninterrupted material supply is essential, such as in chemical manufacturing or food processing. Another notable feature is the system's adaptability to different types of stabilizer powders. The design allows for the handling of powders with varying particle sizes, moisture content, and flow properties, making it suitable for a wide range of applications. The system's ability to handle abrasive or corrosive powders is enhanced by the use of high-quality materials in the construction of the feeder, pipeline, and separation components. Additionally, the system is designed with user-friendly maintenance in mind. Regular maintenance is simplified by the modular design of the components, which allows for easy access and replacement of parts without extensive downtime. This reduces overall operational costs and increases the system's lifespan. Environmental considerations are also a key feature of the system. The closed-loop design and efficient separation units minimize dust emissions, contributing to a cleaner working environment and reduced environmental impact. The system's compliance with local and international environmental standards makes it an attractive choice for companies committed to sustainable operations.
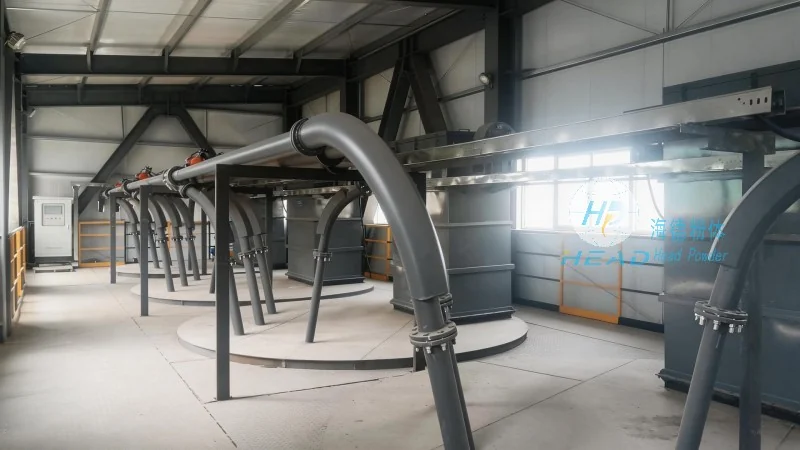
Application and Performance in Industrial Settings
The stabilizer powder pneumatic conveying system from headpowder has proven effective in various industrial settings, where the reliable and efficient transport of powder materials is critical. In chemical plants, for example, the system is used to transport stabilizer powders used in the production of polymers or coatings, ensuring a consistent supply of raw materials to the production lines. The system's ability to handle high volumes and maintain low dust levels helps maintain product quality and reduces the risk of contamination. In the construction industry, the system is employed to transport stabilizer powders used in concrete additives or cement, facilitating the efficient delivery of materials to construction sites. The system's adaptability to different powder characteristics allows it to handle both fine and coarse powders, making it versatile for various construction applications. In the food industry, the system is used to transport stabilizer powders used as additives in food products, where hygiene and dust control are paramount. The system's closed-loop design and stainless steel components ensure that the powder remains clean and free from contamination, meeting stringent food safety standards. Performance-wise, the system typically achieves high conveying rates, often ranging from several tons per hour to over 100 tons per hour, depending on the system size and configuration. The system's energy efficiency is also a significant advantage, with lower operational costs compared to traditional conveying methods. The system's reliability is further enhanced by the use of advanced sensors and control systems that detect and respond to system anomalies in real-time, minimizing downtime and maximizing productivity. Overall, the stabilizer powder pneumatic conveying system from headpowder offers a robust, efficient, and environmentally friendly solution for the transport of powder materials, making it a preferred choice for industries requiring high-quality and reliable material handling solutions.