

Working Principle and Features of Environmental Protection Pneumatic Conveying System Equipment
Environmental protection pneumatic conveying systems represent a crucial technology in modern material handling, offering efficient and sustainable solutions for transporting bulk materials. These systems are designed to minimize environmental impact while ensuring high performance in industrial applications. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing advanced equipment that adheres to stringent environmental standards.
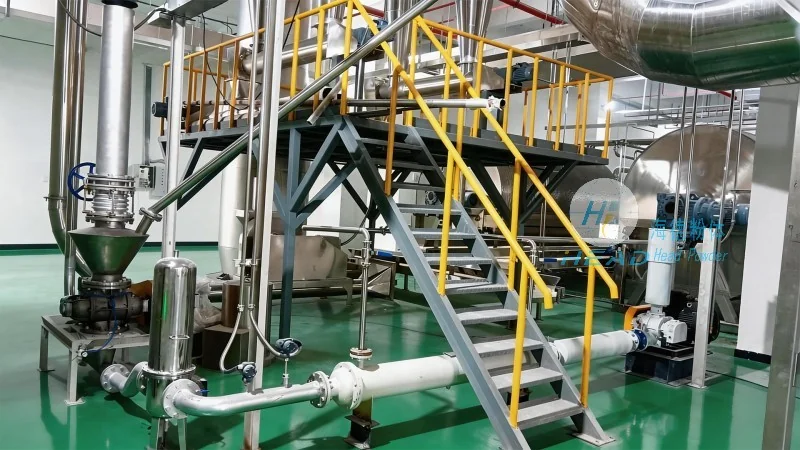
Working Principle of the Environmental Protection Pneumatic Conveying System
The core mechanism of an environmental protection pneumatic conveying system involves the use of compressed air or gas to transport bulk materials through a pipeline network. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. Compressed air is then introduced, creating a flow that propels the material forward. This method eliminates the need for mechanical components like belts or chains, reducing wear and maintenance requirements. The system operates by maintaining a consistent air velocity within the pipeline, ensuring that the material is carried without clogging or degradation. The design incorporates features such as air filtration and dust collection to minimize emissions and ensure compliance with environmental regulations.
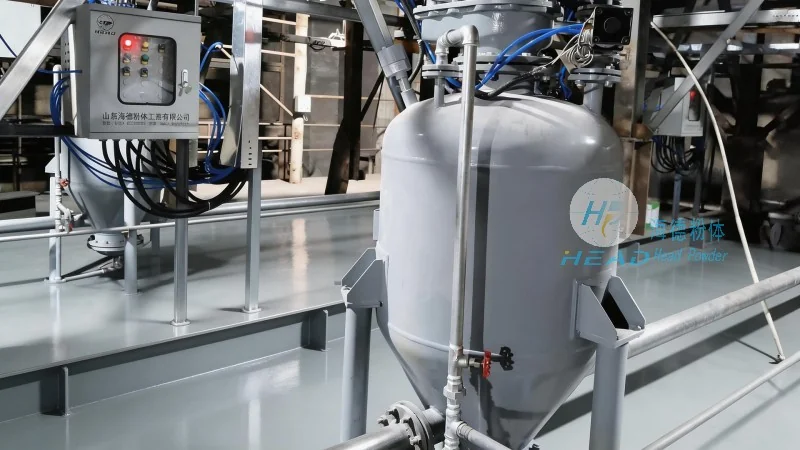
Key Features of the System
Shandong HeadPowder Engineering Co., Ltd. offers several distinctive features that enhance the functionality and efficiency of their environmental protection pneumatic conveying systems. One of the primary advantages is the system's ability to handle a wide range of materials, including powders, granules, and bulk solids, with minimal degradation. The equipment is engineered for high throughput, allowing for continuous operation in industrial settings. Additionally, the system incorporates advanced control systems that optimize air pressure and flow, reducing energy consumption and operational costs. Another notable feature is the integration of dust suppression and filtration technology, which ensures that emissions are kept to a minimum, aligning with global environmental standards. The design also emphasizes durability and low maintenance, with robust components that withstand harsh operating conditions. Furthermore, the system is scalable, allowing for customization to meet the specific needs of different industries, from food processing to chemical manufacturing.
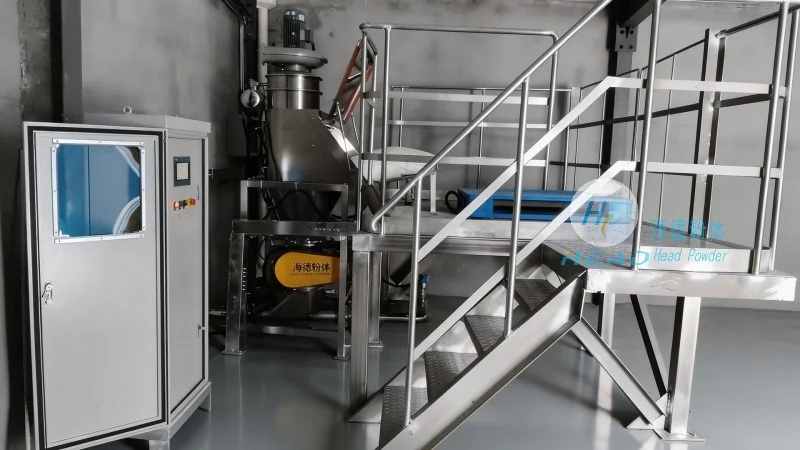
Technical Advantages and Environmental Impact
The environmental protection pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. offers several technical advantages that contribute to its effectiveness. The use of enclosed pipelines prevents dust and particulate matter from being released into the environment, reducing air pollution and health risks for workers. The system's energy efficiency is another key benefit, as it minimizes power consumption compared to traditional mechanical conveying methods. This not only lowers operational costs but also reduces the carbon footprint of industrial operations. The equipment is also designed for easy integration into existing production lines, allowing for seamless upgrades without major disruptions. The company's commitment to sustainability is reflected in the materials used in the construction of the system, which are often recyclable or made from eco-friendly components. By adopting this technology, industries can achieve significant reductions in waste and emissions, contributing to a more sustainable future.
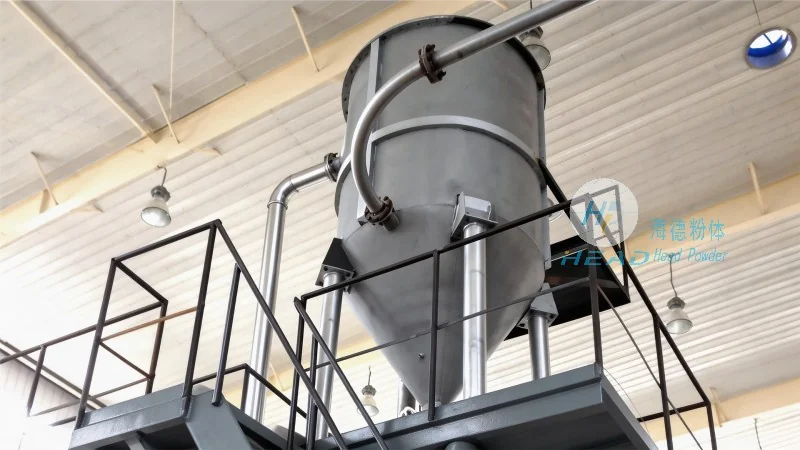
Application Examples and Industry Use Cases
The environmental protection pneumatic conveying system is widely used across various industries, demonstrating its versatility and reliability. In the food and beverage sector, it is employed to transport ingredients like flour, sugar, and spices, ensuring hygienic and dust-free handling. The system's ability to maintain product integrity is particularly valuable in these applications. In the chemical industry, it is used to convey powders and granules, such as fertilizers and pigments, while adhering to strict safety and environmental regulations. The pharmaceutical industry also benefits from the system's ability to handle sensitive materials without contamination. Additionally, the system is utilized in the mining and minerals sector for transporting raw materials and byproducts, improving operational efficiency and reducing environmental impact. Each application leverages the system's core principles of efficient material transport and minimal environmental impact, making it a preferred choice for companies committed to sustainability.