

Working Principle and Features of Vacuum Negative Pressure Pneumatic Conveying System Equipment
Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced vacuum negative pressure pneumatic conveying systems. Our systems are engineered to efficiently transport bulk materials with precision and reliability, making them ideal for various industrial applications. This article explores the working principle and key features of our vacuum negative pressure pneumatic conveying equipment, highlighting its advantages and practical applications.
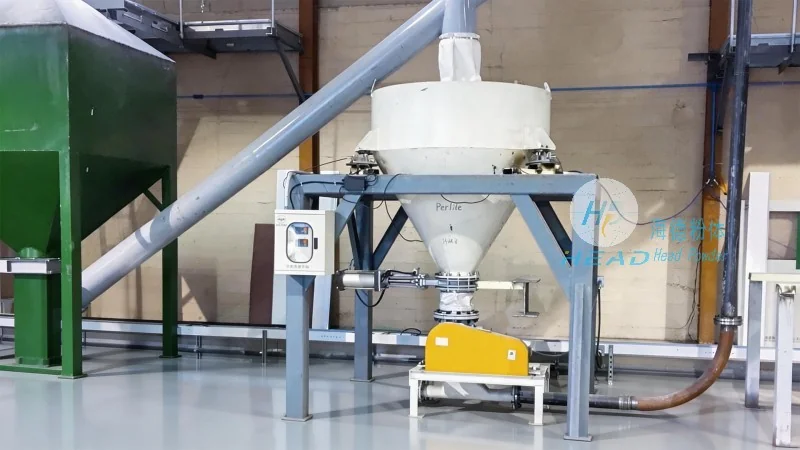
Introduction to Vacuum Negative Pressure Pneumatic Conveying Systems
At Shandong HeadPowder Engineering Co., Ltd., we specialize in developing and manufacturing high-performance vacuum negative pressure pneumatic conveying systems. These systems are designed to handle a wide range of bulk materials, including powders, granules, and fine particles, with minimal product degradation and maximum efficiency. The core technology behind our systems involves creating a negative pressure environment within the conveying line, which draws material from the source to the destination through a sealed pipeline. This method offers several advantages over traditional positive pressure systems, such as reduced energy consumption, lower operational costs, and enhanced safety.
Working Principle of Vacuum Negative Pressure Pneumatic Conveying Systems
The working principle of our vacuum negative pressure pneumatic conveying systems is based on the fundamental concept of air movement and material transport. The system operates by generating a vacuum in the receiving hopper or the conveying line, which creates a pressure differential between the source and the destination. As the pressure inside the conveying line is lower than the atmospheric pressure outside, air is drawn into the system, carrying the material particles along with it. The material is then deposited at the discharge point, where the pressure is restored to atmospheric levels. This process is continuous and can be controlled to handle varying material flow rates and particle sizes. The vacuum is typically generated by a high-efficiency vacuum pump, which maintains the necessary pressure differential throughout the conveying cycle. The system also includes components such as a filter, a silencer, and a material separator to ensure clean and efficient operation.
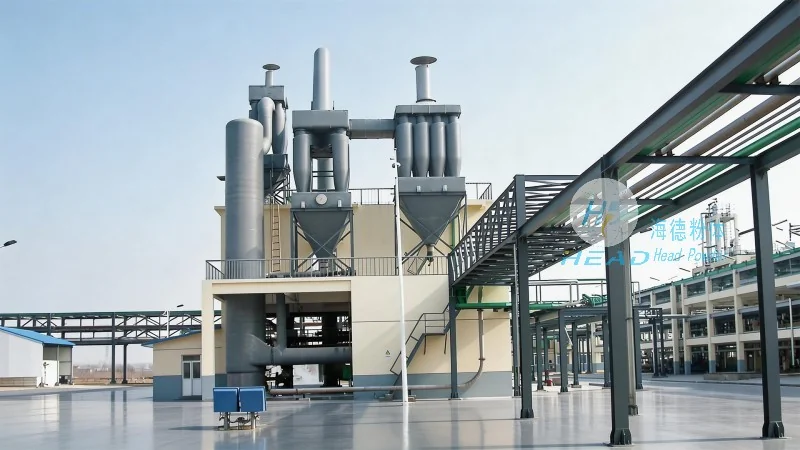
Key Features of Vacuum Negative Pressure Pneumatic Conveying Systems
Our vacuum negative pressure pneumatic conveying systems are equipped with several key features that enhance their performance and usability. One of the primary features is the ability to handle a wide variety of materials, including sensitive powders that are prone to clumping or degradation. The sealed pipeline design prevents contamination and maintains product integrity, which is crucial for industries such as pharmaceuticals, food processing, and chemical manufacturing. Another important feature is the energy efficiency of the system, as the vacuum pump operates at lower pressures compared to positive pressure systems, resulting in reduced energy consumption and lower operational costs. The system also offers flexibility in terms of layout and installation, as the conveying line can be customized to fit the specific requirements of the facility. Additionally, our systems are designed with safety in mind, incorporating features such as pressure relief valves and emergency shut-off mechanisms to prevent accidents and ensure safe operation.
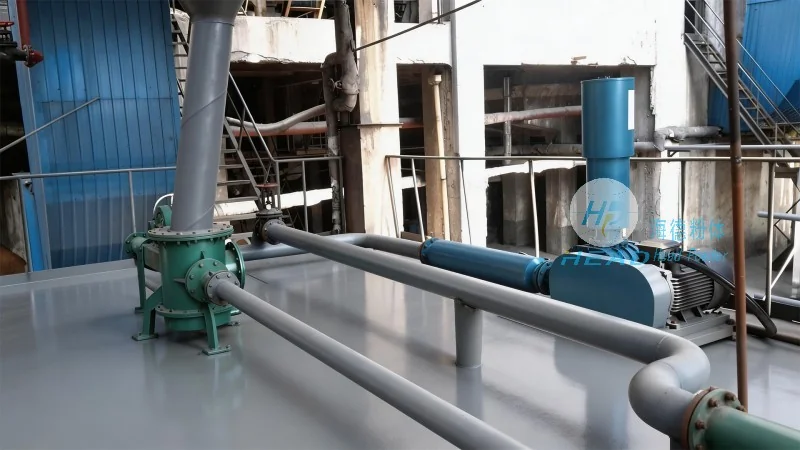
Applications and Benefits of Vacuum Negative Pressure Pneumatic Conveying Systems
Vacuum negative pressure pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and minerals. The systems are particularly suitable for applications where product contamination and degradation must be minimized, such as the transport of sensitive powders or granules. The benefits of using our vacuum negative pressure systems include improved product quality, reduced labor costs, and increased operational efficiency. The sealed pipeline design prevents cross-contamination and maintains the purity of the material, which is essential for industries that adhere to strict quality standards. Additionally, the energy-efficient operation of the system reduces the overall cost of material handling, making it a cost-effective solution for long-term use. Our systems are also designed to be easy to maintain and service, with accessible components that can be replaced quickly, minimizing downtime and maximizing productivity.
Conclusion and Company Information
Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality vacuum negative pressure pneumatic conveying systems that meet the diverse needs of our clients. Our systems are designed with advanced technology and engineering expertise to ensure reliable and efficient operation. We offer customized solutions tailored to the specific requirements of each application, ensuring optimal performance and cost-effectiveness. With our extensive experience and expertise in the field, we are a trusted partner for industries seeking reliable and efficient material handling solutions. Our company is located in Shandong, China, and we are dedicated to delivering superior products and services to our customers worldwide.