

Working Principle and Features of Methylcellulose Pneumatic Conveying Equipment
At Shandong HeadPowder Engineering Co., Ltd. (headpowder), we specialize in the design and manufacturing of advanced pneumatic conveying systems tailored for various industrial applications, including the efficient handling of methylcellulose and other fine powders. This article delves into the working principle and key characteristics of our methylcellulose pneumatic conveying equipment, providing a comprehensive understanding of its functionality and benefits.

Understanding the Working Principle of Methylcellulose Pneumatic Conveying Equipment
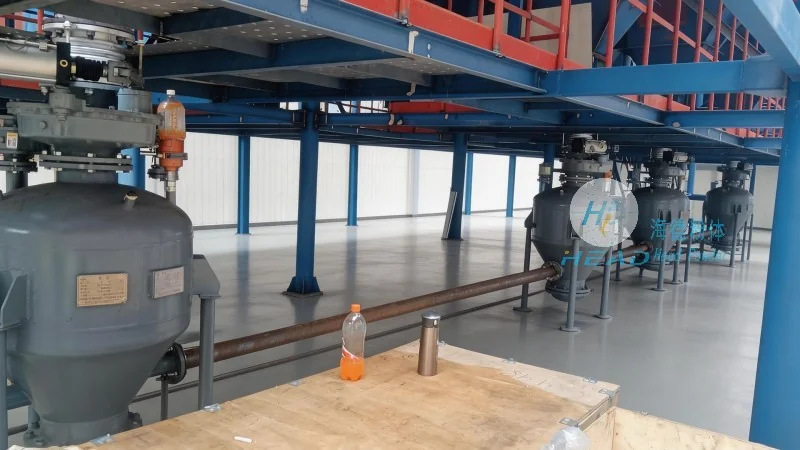
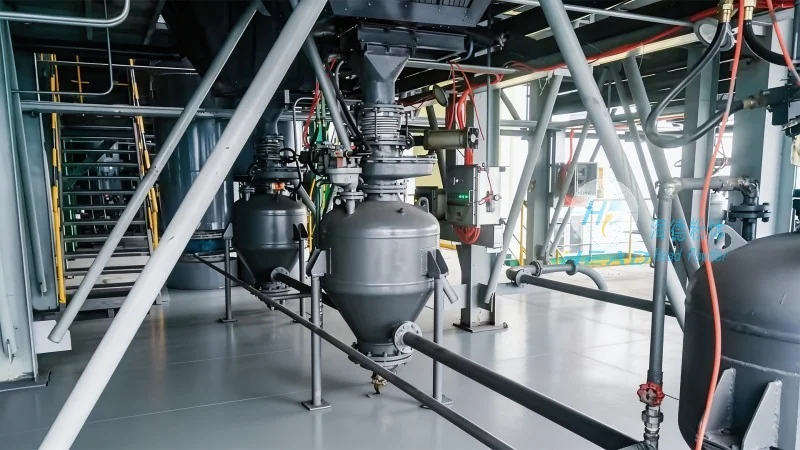
The core of methylcellulose pneumatic conveying equipment lies in its ability to transport fine powders like methylcellulose through a pressurized or vacuum system. The process typically involves a series of components that work in tandem to ensure reliable and efficient material transfer. The system begins with a hopper or feeder that stores the methylcellulose powder. From there, the material is drawn into a conveying line by either positive pressure (air or gas) or negative pressure (vacuum). The conveying line may include bends, filters, and control valves to manage the flow and prevent blockages. The equipment is engineered to handle the specific properties of methylcellulose, such as its fine particle size and potential for static charge, ensuring smooth operation and minimal product degradation.
Key Features of Methylcellulose Pneumatic Conveying Equipment
Our methylcellulose pneumatic conveying equipment is designed with several distinct features that enhance performance and reliability. One of the primary features is its ability to handle fine powders with high efficiency, minimizing product loss and ensuring consistent flow rates. The system incorporates advanced control mechanisms that allow for precise regulation of air pressure and flow, adapting to varying load conditions. Additionally, the equipment is constructed from materials that are resistant to corrosion and wear, ensuring long-term durability even in harsh industrial environments. Another notable feature is its low maintenance requirements, with easy access to components for cleaning and maintenance, reducing downtime and operational costs. The design also prioritizes safety, with built-in safety valves and pressure relief systems to prevent over-pressurization and ensure operator safety.
Benefits of Using Methylcellulose Pneumatic Conveying Equipment
Implementing methylcellulose pneumatic conveying equipment offers numerous advantages for industrial operations. The primary benefit is the significant improvement in material handling efficiency, as the system can transport powders over long distances with minimal labor and energy consumption. This reduces the need for manual handling and associated risks, enhancing workplace safety. The equipment also helps maintain product quality by minimizing exposure to air and moisture, which can affect the properties of methylcellulose. Furthermore, the system's ability to handle fine powders without clogging or blockages ensures consistent production output and reduces the likelihood of equipment downtime. For manufacturers dealing with methylcellulose, this translates to increased productivity and cost savings over time.
Application Examples and Industry Use Cases
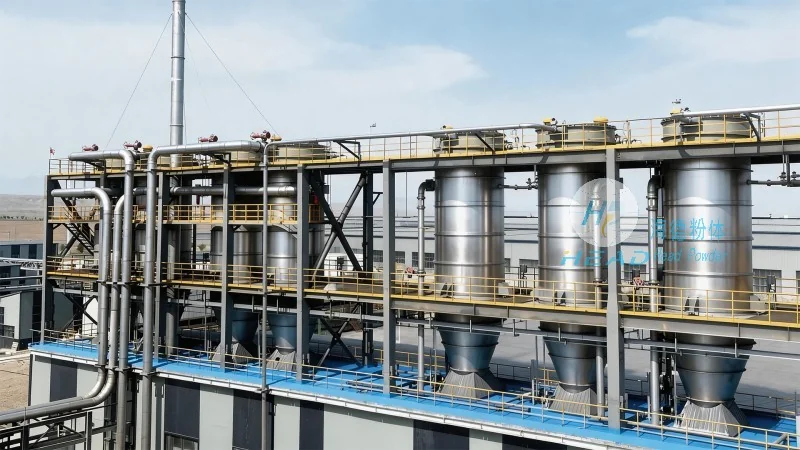
Methylcellulose pneumatic conveying equipment is widely used in various industries where fine powders need to be transported, such as pharmaceuticals, food processing, and chemical manufacturing. In the pharmaceutical industry, the equipment is crucial for handling active ingredients and excipients, ensuring that the powders are transferred without contamination or degradation. In food processing, it is used for transporting ingredients like methylcellulose in food products, maintaining product integrity and safety standards. Chemical manufacturers also benefit from the system's ability to handle reactive or sensitive powders, providing a controlled environment for material transfer. These applications highlight the versatility and reliability of our equipment, making it a preferred choice for industries requiring high-quality material handling solutions.