

Working Principle and Features of the Air-Driven Magnesium Sulfate Heptahydrate Handling Equipment
For industrial applications involving the transport of magnesium sulfate heptahydrate, specialized equipment is essential to ensure efficient and safe handling. The air-driven handling system, commonly referred to as a pneumatic conveyor, has become a preferred solution for many industries due to its versatility and reliability. This article explores the working principle and key features of such equipment, with a focus on the specific requirements of magnesium sulfate heptahydrate transport.
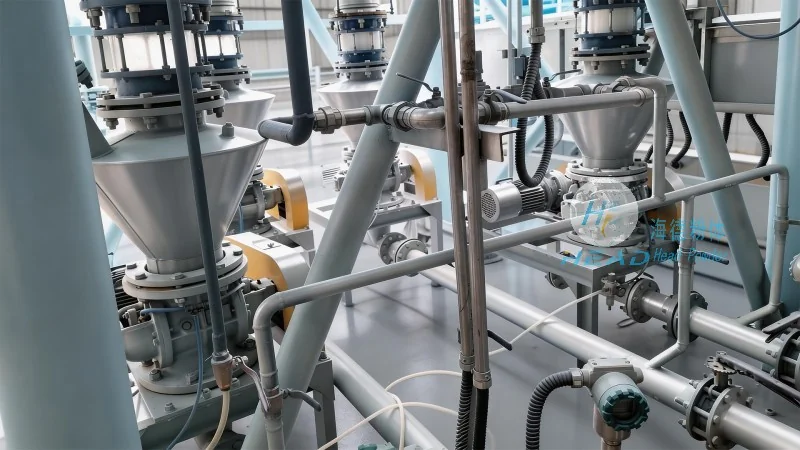
Introduction to Air-Driven Handling Equipment for Magnesium Sulfate Heptahydrate
Magnesium sulfate heptahydrate, often used in pharmaceuticals, agriculture, and chemical manufacturing, requires careful handling to maintain its quality and prevent degradation. Traditional methods like belt conveyors or bucket elevators may not be suitable for this material due to its hygroscopic nature and potential for dust generation. The air-driven system addresses these challenges by utilizing compressed air to move the material through a sealed pipeline, minimizing exposure to the environment and reducing the risk of contamination.
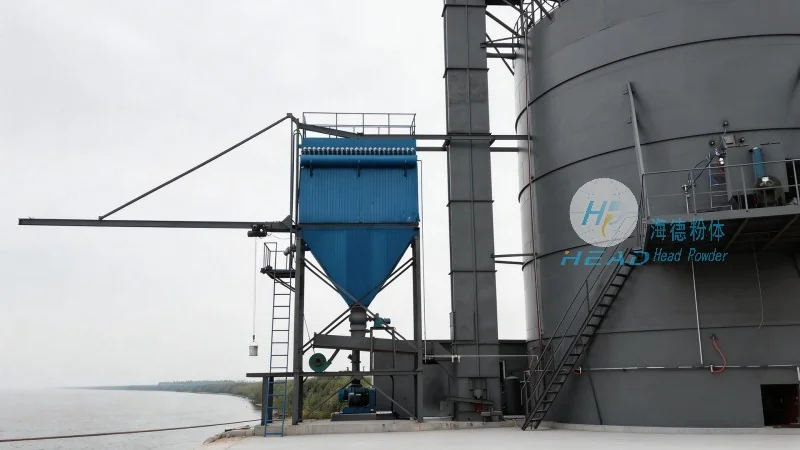
Working Principle of the Air-Driven Magnesium Sulfate Heptahydrate Handling Equipment
The core of the air-driven handling system is the transfer of material using air pressure. The equipment typically consists of a series of components including a material hopper, an air compressor, a conveying pipeline, and a discharge unit. The process begins with the material being fed into the hopper, where it is then pneumatically conveyed through the pipeline by the force of compressed air. The air compressor generates the necessary pressure to move the material, while the pipeline design ensures a smooth and continuous flow. For magnesium sulfate heptahydrate, the system is often configured as a positive pressure system, where air is blown into the pipeline to push the material forward. This method is effective for handling dry powders and granules, as it prevents material from sticking to the pipeline walls and maintains a consistent flow rate.
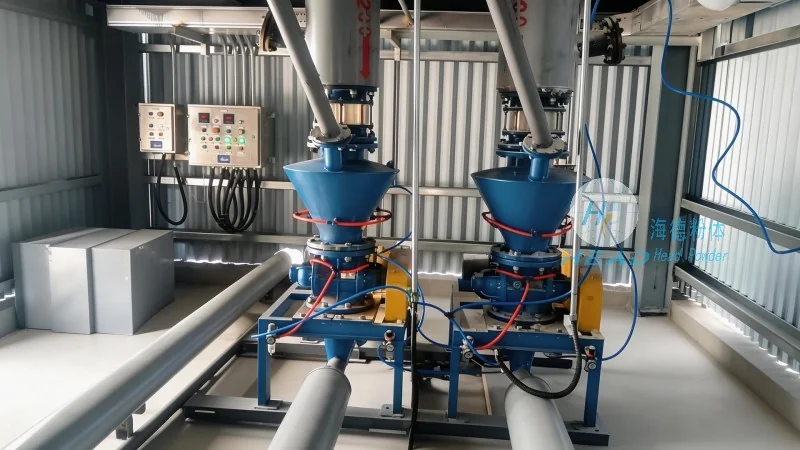
Key Features and Advantages of the Air-Driven System
The air-driven handling equipment for magnesium sulfate heptahydrate offers several advantages that make it an ideal choice for industrial applications. Firstly, it provides a dust-free and enclosed transport process, which is crucial for maintaining the purity of the material and ensuring compliance with environmental regulations. The sealed pipeline design minimizes the release of fine particles into the air, reducing the risk of inhalation hazards and contamination of the surrounding environment. Secondly, the system is highly efficient in terms of energy consumption and operational speed. The use of compressed air allows for rapid material transfer over long distances, with minimal downtime for maintenance or cleaning. Additionally, the equipment is designed to handle varying material loads, making it adaptable to different production volumes and operational needs. The positive pressure system also ensures that the material is not exposed to external air, which helps preserve its moisture content and prevent caking or clumping. This is particularly important for magnesium sulfate heptahydrate, as moisture retention is critical for maintaining its chemical properties and usability in downstream processes.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer of industrial handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and producing customized air-driven systems tailored to the specific needs of various industries. With a focus on quality and innovation, the company has developed advanced solutions for material transport, including the air-driven handling equipment for magnesium sulfate heptahydrate. HeadPowder's expertise in pneumatic conveying technology ensures that their products are reliable, efficient, and compliant with international standards. The company's facilities are located in Shandong, China, where they employ skilled engineers and technicians to design, manufacture, and test their equipment. By choosing HeadPowder, industries can benefit from a proven solution that enhances operational efficiency while maintaining the highest standards of safety and environmental responsibility.