

Introduction to Equipment and Structural Principles of Mineral Sand Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., branded as HeadPowder, is a leading enterprise in the field of pneumatic conveying technology, specializing in the design, manufacturing, and supply of equipment for mineral sand and bulk material handling. The company is headquartered in Shandong, China, and has built a strong reputation for delivering high-quality, reliable systems that meet the demands of modern industrial operations. HeadPowder's commitment to innovation and customer satisfaction has enabled it to serve a diverse clientele across various sectors, including mining, chemical processing, and food production. The company's team of experienced engineers and technicians ensures that each project is tailored to the unique needs of the client, resulting in efficient and effective material handling solutions.
Overview of Mineral Sand Pneumatic Conveying Systems
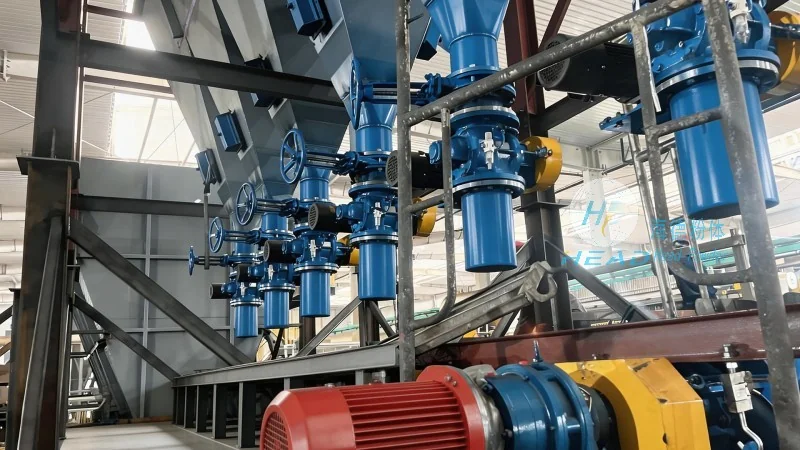
Mineral sand pneumatic conveying systems represent a sophisticated approach to transporting bulk materials through a pipeline using air pressure. Unlike traditional mechanical conveyors, these systems offer a dust-free, flexible, and low-maintenance solution for moving mineral sands and other fine or granular materials. The primary function of the system is to draw material from a hopper or storage silo and transport it to a discharge point, such as a processing plant or storage facility. The system operates by creating a pressure differential between the inlet and outlet of the pipeline, which propels the material forward. This method not only enhances material flow efficiency but also reduces the risk of material degradation and contamination.
Structural Principles of Pneumatic Conveying Equipment
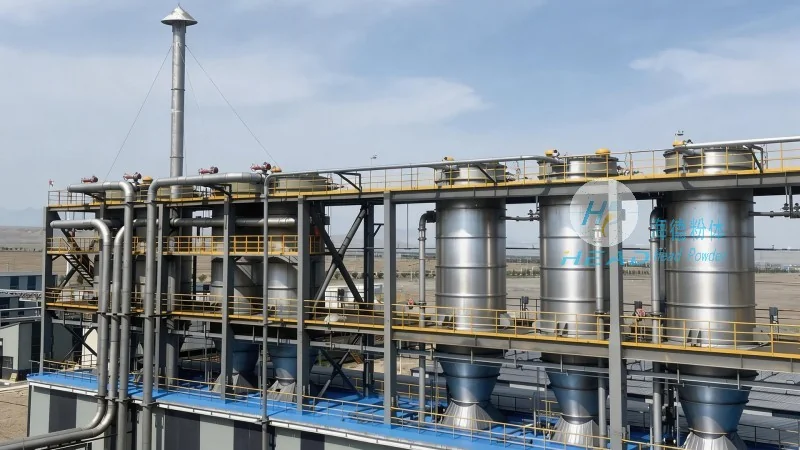
The structural design of mineral sand pneumatic conveying systems is a critical factor in ensuring optimal performance and longevity. HeadPowder's systems incorporate several key components that work in harmony to achieve efficient material transport. The feeding mechanism, typically a rotary valve or screw feeder, ensures a consistent and controlled intake of material from the source. This component is designed to handle the abrasive nature of mineral sands, preventing wear and tear over time. The air delivery system, which may include a blower or compressor, provides the necessary pressure to move the material through the pipeline. The pipeline network is constructed from durable materials like stainless steel or high-density polyethylene (HDPE), chosen for their resistance to corrosion and abrasion. The discharge unit, often equipped with a cyclone separator or bag filter, separates the material from the air stream, allowing for clean material collection and air recycling. Advanced control systems, such as programmable logic controllers (PLCs) and sensors, are integrated into the design to monitor and regulate system performance, ensuring consistent operation and minimizing energy consumption.
Key Features and Advantages of the Equipment
HeadPowder's mineral sand pneumatic conveying systems are equipped with several features that enhance their functionality and reliability. One of the primary advantages is the high material handling capacity, which can range from 5 to over 200 tons per hour, depending on the system configuration. This flexibility allows the equipment to handle a wide variety of material types and volumes, making it suitable for both small-scale and large-scale industrial applications. The systems are also highly adaptable, with the ability to integrate multiple inlet and outlet points, enabling complex material routing within a facility. Another significant benefit is the dust-free operation, which improves workplace safety and reduces environmental pollution. The equipment is designed with easy maintenance in mind, featuring modular components that can be replaced or serviced without extensive downtime. The use of advanced materials and engineering ensures a long service life, with minimal maintenance requirements, making these systems a cost-effective investment for industrial operations.
Application Scenarios and Industrial Use
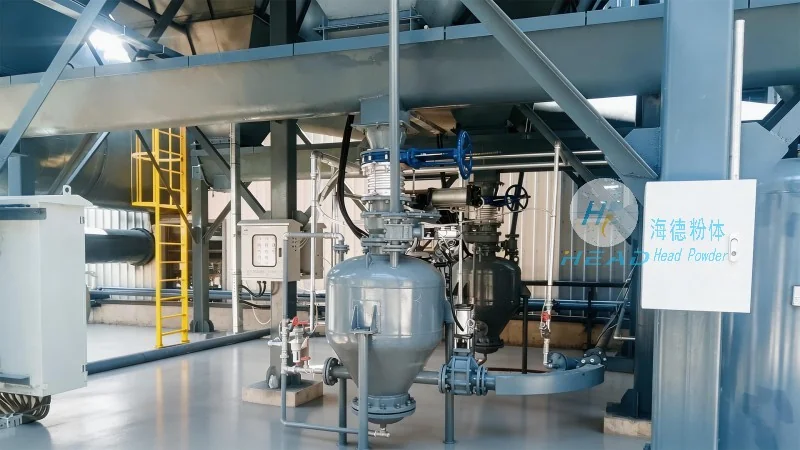
Mineral sand pneumatic conveying systems find extensive applications in various industries, particularly in the mining and chemical sectors. In the mining industry, these systems are commonly used to transport crushed mineral sands from processing plants to storage or shipping facilities, ensuring efficient material movement and reducing the need for manual handling. In the chemical industry, they are employed to handle powders and granules during production processes, such as mixing, blending, and packaging. The food processing industry also benefits from these systems, as they provide a hygienic and efficient method for transporting food-grade powders and granules, maintaining product quality and safety standards. HeadPowder's systems are customized to meet the specific requirements of each application, incorporating features like temperature control, material drying, and dust collection to ensure optimal performance. The company's expertise in system design and integration ensures that clients receive solutions that are tailored to their unique operational needs, enhancing productivity and reducing operational costs.