

Operation Process and Working Principle of Air-Driven Transportation for Ammonium Bicarbonate Materi
Ammonium bicarbonate, a widely used chemical in various industrial applications, requires efficient and reliable transportation methods to ensure smooth production workflows. Air-driven transportation, or pneumatic conveying, offers a robust solution for moving this material from storage to processing units. This article delves into the operation process and working principle of such systems, highlighting the key components and mechanisms involved in the process.
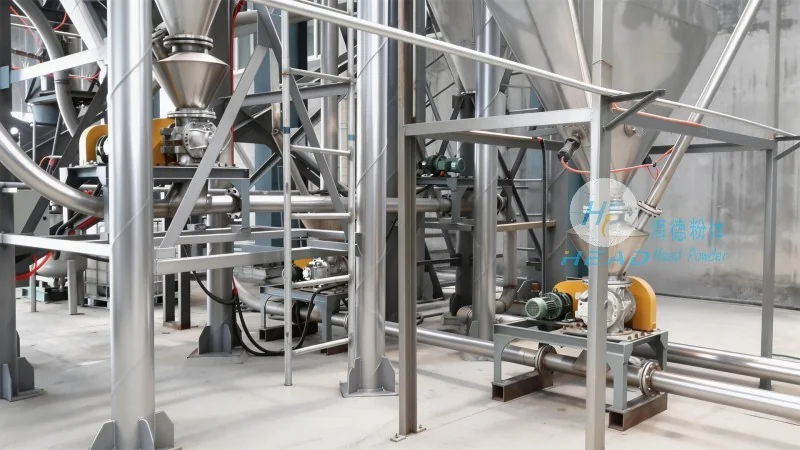
Key Components of the Air-Driven Transportation System
The air-driven transportation system for ammonium bicarbonate typically consists of several critical components that work in tandem to achieve effective material movement. These include a hopper or storage silo for material storage, a feeder to control the flow of material, a conveyor pipe network, a blower or air compressor to generate the necessary air pressure, and a receiver or discharge hopper for material collection. Each component plays a vital role in maintaining the system's efficiency and safety.
Working Principle of the Air-Driven Transportation Process
The operation of the air-driven transportation system begins with the material being fed from the storage hopper into the conveyor pipe. The feeder regulates the amount of ammonium bicarbonate released, ensuring a consistent flow rate. Simultaneously, the blower generates high-pressure air that is introduced into the conveyor pipe. As the air flows through the pipe, it creates a low-pressure zone, which draws the ammonium bicarbonate particles into the air stream. The mixture of air and material then travels through the pipe network to the discharge point, where the material is separated from the air and collected in the receiver hopper.
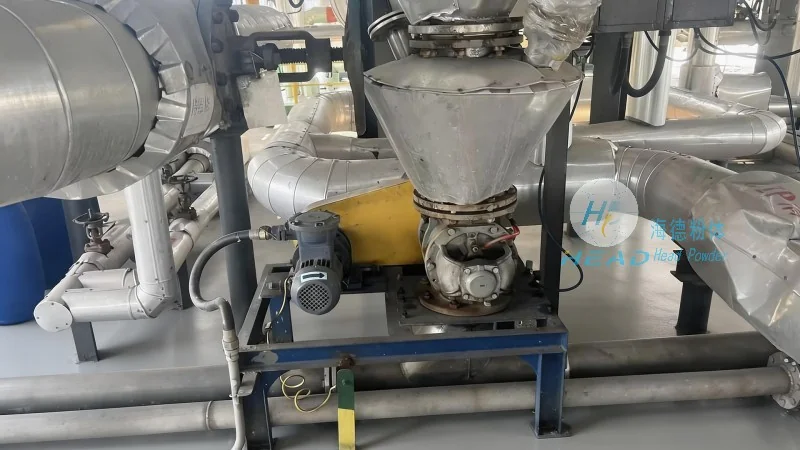
Control and Monitoring in the System
Modern air-driven transportation systems for ammonium bicarbonate are equipped with advanced control and monitoring features to optimize performance and ensure safety. These systems often include sensors to detect material levels in the hopper and receiver, pressure gauges to monitor air pressure, and alarms to alert operators of any abnormalities. Additionally, variable frequency drives (VFDs) may be used to adjust the blower speed, allowing for precise control over the air flow and material transport rate. This level of control helps maintain consistent material delivery and reduces the risk of system failures or material blockages.
Advantages of Air-Driven Transportation for Ammonium Bicarbonate
Compared to traditional mechanical conveying methods, air-driven transportation offers several advantages for handling ammonium bicarbonate. These include reduced risk of material contamination, as the system is enclosed and sealed, preventing exposure to external elements. Additionally, the system can handle a wide range of material sizes and moisture content, making it suitable for various industrial applications. The enclosed nature of the system also minimizes dust emissions, contributing to a safer working environment. Furthermore, the flexibility of the pipe network allows for easy reconfiguration of the system to accommodate changes in production requirements.
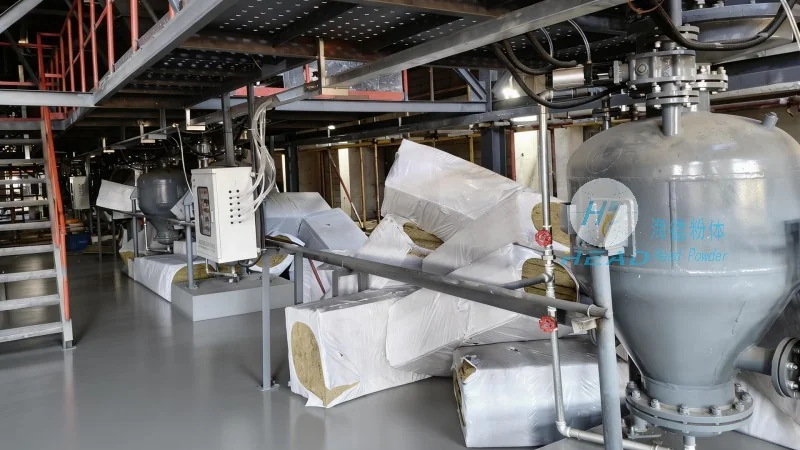
Applications and Industries Served
The air-driven transportation systems developed by Shandong HeadPowder Engineering Co., Ltd. are widely used in industries that handle ammonium bicarbonate, including chemical manufacturing, food processing, and pharmaceutical production. These systems are particularly valuable in applications where material purity and consistent flow are critical. For example, in chemical plants, the system ensures that ammonium bicarbonate is delivered to reactors without any contamination, which is essential for maintaining product quality. In food processing facilities, the enclosed system prevents cross-contamination with other materials, meeting stringent food safety standards. The reliability and efficiency of these systems make them a preferred choice for industries seeking to optimize their material handling processes.
Conclusion and Company Overview
Efficient air-driven transportation is crucial for the smooth operation of processes involving ammonium bicarbonate. The systems developed by Shandong HeadPowder Engineering Co., Ltd. leverage advanced technology and robust design to provide reliable and safe material handling solutions. By understanding the operation process and working principle of these systems, industries can enhance their production efficiency and ensure the quality of their products. With a focus on innovation and customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. continues to provide high-quality air-driven transportation solutions tailored to the specific needs of its clients.